
RAYPCB · ENGINEERING REFERENCE
Solder Paste for PCB Assembly: Alloy, Powder & Flux Selection
Specify the alloy, powder, flux and handling evidence that a PCB assembly needs. Compare requirements before substituting a paste.
Original engineering guidance · References checked September 29, 2026
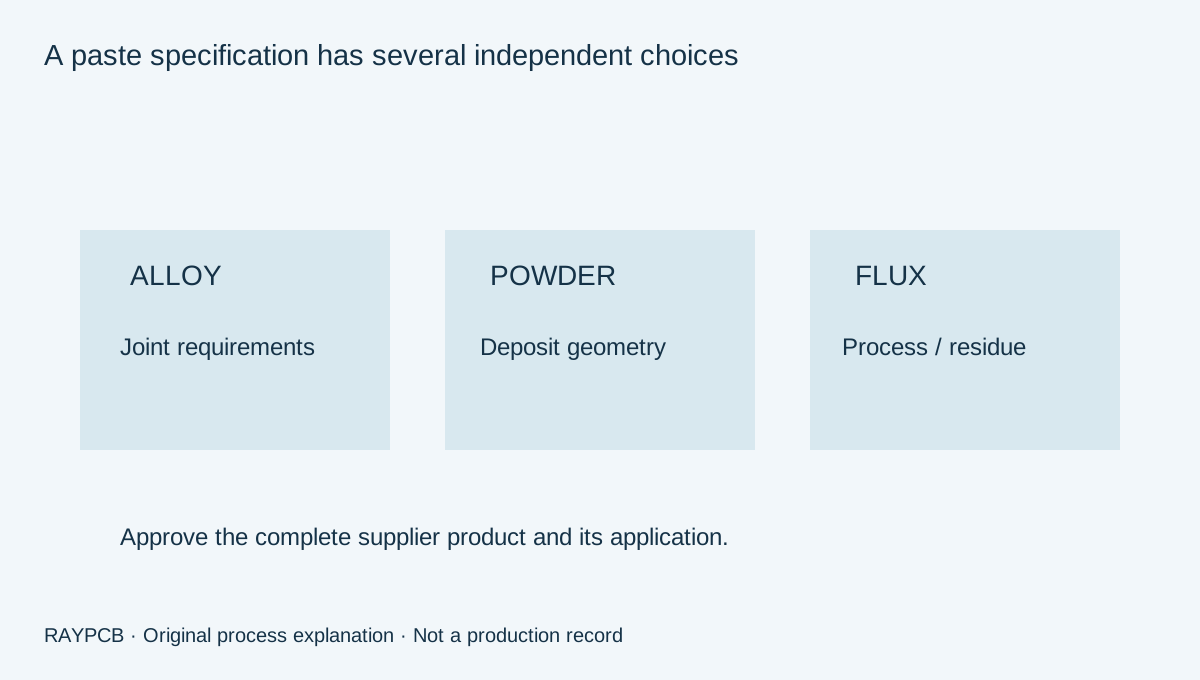
Specify a soldering material, not just a jar of paste
Solder paste combines metal alloy particles with a flux vehicle so that solder can be deposited, components placed and joints formed during reflow. For PCB assembly, selecting the paste means selecting a complete material system. Alloy, powder distribution, deposition behavior, flux activity, residue requirements and storage instructions belong together. Two products carrying the same alloy designation are not automatically interchangeable in an approved manufacturing process.
The useful purchasing question is therefore: which exact product can be used with this board, these components and this process? A fine-pitch device may make printing difficult, while a large grounded connector or thermal pad makes heating and solder volume difficult. The selected paste has to work across the actual assembly. This guide helps engineers prepare that selection; it is not a retail catalog or a substitute for the supplier's current technical data sheet.
If the immediate task is a new build, start with the released BOM, assembly drawing and any customer restrictions. If the task is a substitution, identify what changes and what evidence must be repeated. A paste substitution is easier to review when the current product, proposed product and affected requirements appear side by side. Descriptions such as premium, fine pitch or lead free are not enough to close that comparison.
The specification fields that matter
| Specification field | What to record | Why it changes the decision |
|---|---|---|
| Product identity | Supplier, exact product code, revision and lot | Establishes which formulation and document apply |
| Alloy | Composition and permitted alternatives | Sets the metallurgical and thermal starting point |
| Powder | Supplier classification and particle distribution | Affects deposition through the actual geometry |
| Flux system | Classification, process conditions and residues | Connects soldering to cleaning and product reliability |
| Deposition | Printing, dispensing, jetting or another qualified method | Different delivery methods need suitable behavior |
| Handling | Storage, conditioning, exposure and expiry instructions | Keeps production use within the approved material conditions |
The Indium PCB assembly paste portfolio illustrates why alloy, powder and flux cannot be reduced to one universal product. It includes different formulations and deposition applications. Use manufacturer product data for a shortlisted material rather than inferring suitability from a broad category page. Supplier marketing descriptions help locate a candidate; the released specification and trial evidence determine whether it can be used on your assembly.
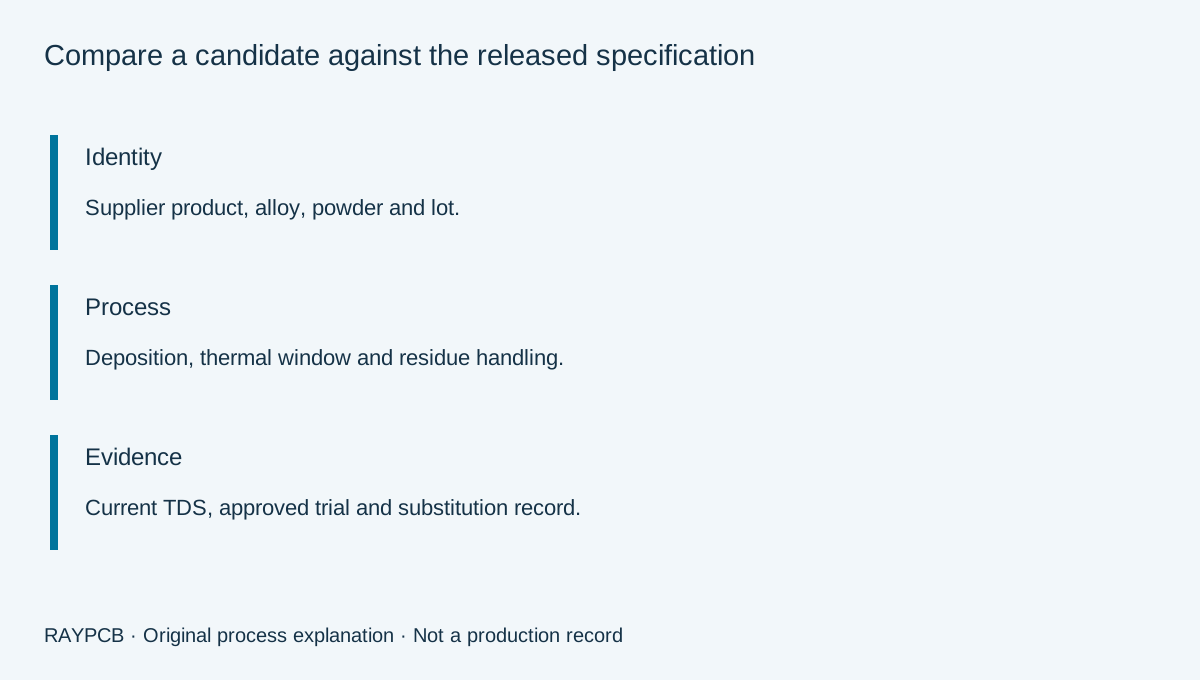
Start with the joint and the product requirements
An alloy decision affects more than the temperature needed to form a joint. Review component termination finishes, board finish, service conditions, customer material restrictions and the approved repair route. A change made to simplify initial assembly can complicate later repair or introduce an unreviewed mixed-alloy condition. Document which parts and surfaces participate in the joint rather than treating the paste as an isolated consumable.
Lead-free does not identify one alloy or one process window. Similarly, a lower melting range does not by itself establish suitability for an application with demanding mechanical or thermal exposure. Request a materials review when the reason for selection involves shock, vibration, low-temperature assembly or repeated temperature cycling. This page does not assign reliability ratings to alloy families or claim that one composition is universally best.
For an alternate product, write a small change matrix: what stays the same, what changes, and what evidence addresses each change. Keep approved BOM and process records synchronized. If the same paste is used across several products, do not assume that a successful trial on the simplest board qualifies the most thermally demanding board. Select a trial scope that represents the actual differences in the affected products.
Connect powder selection to the aperture and deposition method
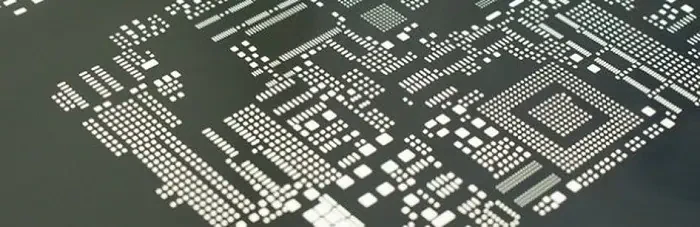
Powder choice should be evaluated with aperture size, foil thickness, opening shape, wall condition and the expected deposit. Choosing a finer powder is not a complete response to a poorly releasing aperture. It also changes the material system that must print, remain usable during production and reflow acceptably. Ask the supplier for guidance on the intended deposition method and validate the smallest or most difficult feature groups on the board.
The actual stencil defines the geometry that paste must pass through. A general statement about component pitch can hide substantial differences in aperture area and thickness. Move dimensional questions to the PCB stencil design and selection guide, where foil and aperture decisions can be reviewed together. Keep the paste product and stencil revision connected in the resulting release record.
For dispensing or jetting, confirm that the candidate formulation is specified for that delivery method. A paste that performs well under a squeegee does not automatically behave correctly in a nozzle or jetting system. Record equipment compatibility, deposition stability and any handling requirements that differ from the printing line. Trial results should identify the method used; a photograph of a finished board cannot establish this compatibility.
Plan residue handling before committing to the material
No-clean describes a material and process approach; it does not mean every product may retain every residue under every condition. Review the electrical environment, exposed surfaces, coating or encapsulation plans, inspection access and customer requirements. If cleaning is required, the chemistry, equipment, rinse and drying process must be compatible with the assembly. Changing only the flux can therefore affect downstream operations even when the alloy remains unchanged.
A practical release note should state whether residue is retained or removed, how that decision is justified and which evidence is required. Avoid an ambiguous instruction such as clean if necessary when production needs a repeatable disposition. The engineering team should define what condition triggers cleaning, what method is approved and how completion is verified. This becomes especially useful when a prototype is transferred to repeat production or another assembly location.
Keep flux classification, safety information and cleaning instructions as different records. A safety data sheet addresses handling hazards; it does not replace the thermal or printing parameters in the technical data sheet. The Kester document center provides product-specific documentation for its materials. Check the exact product and current revision, and obtain clarification from the supplier when the intended process is outside the documented use.
Treat storage, conditioning and working exposure separately
The unopened shelf life, permitted storage conditions, conditioning before use, working exposure and restart procedure answer different questions. Do not combine them into one timer. The label may identify expiry, while the technical document describes the conditions under which that expiry or working period applies. A material-control record should make these conditions visible to the operator without requiring them to guess from a previous product.
Track receipt, lot identity, storage location, removal from storage, opening and return or disposal disposition. If a container has an uncertain history, record the uncertainty and request a material decision. Adding fresh material to an unidentified remainder can destroy useful traceability. Likewise, an acceptable visual appearance is not proof that an expired or mishandled product has retained its intended performance.
Conditioning should follow the supplier's procedure, including the instructions that prevent moisture contamination when changing environments. Do not invent a warming method or use a universal time based only on container size. Production interruptions also need a defined response: what is checked at restart, how the first prints are evaluated, and which material may be reused. The solder paste printing process guide connects these handling decisions to observable deposit quality.
Build a usable paste specification brief
The worksheet records the deposition route, flux system and whether the alloy, powder, current technical data and residue requirements have been documented. Its result is a list of open decisions, not a score for how good a paste is. A missing document remains an open item even if several other fields are complete. You can start an inquiry with those items unresolved rather than entering invented specifications.
RAYPCB ENGINEERING
Assembly SolderingSolder paste specification worksheet
Loading Solder paste specification worksheet…
Load the example only to see the output format. Project mode starts blank, and changing any input invalidates the previous result. The downloaded brief retains the declared requirements and open items. Attach it manually with the relevant drawing or material comparison; the Contact form does not automatically receive worksheet values. The worksheet neither recommends a commercial brand nor approves a substitution.
Use a trial that answers a specific question
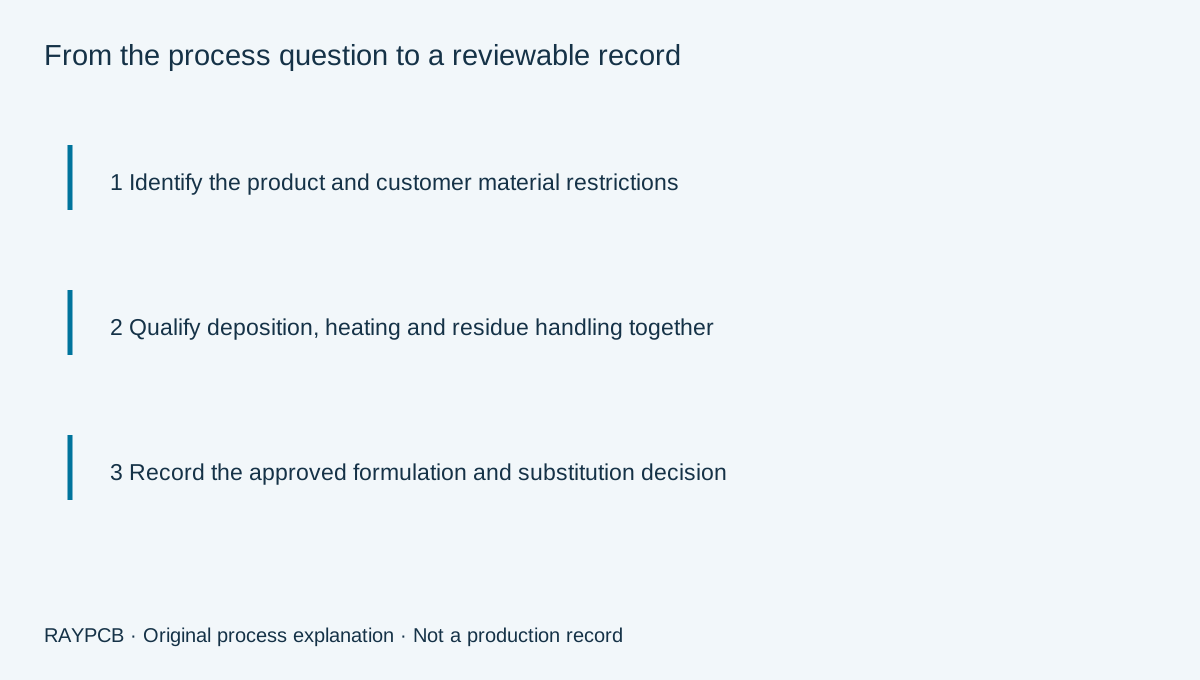
Define the purpose of the trial before measuring anything. A release problem at a small aperture, a residue concern under a component and a solder-joint thermal requirement need different evidence. The trial record should identify the board revision, stencil revision, paste lot, printer program, measured thermal profile and inspection method. Without those identifiers, a good result may be difficult to reproduce or compare with the next revision.
An illustrative trial might compare two approved candidate formulations on the same pad groups while keeping the board support and stencil constant. Record deposit measurements, interruptions, restart behavior and final joint evidence. If the stencil or thermal program changes too, identify that as a new combined condition rather than attributing the outcome to the paste alone. This is an experiment-planning example, not a claimed RAYPCB customer result.
Compare total process impact rather than price per container
Paste purchase cost is only one part of the economic decision. Container size, changeover frequency, expiry management, working waste, cleaning requirements and inspection effort can change the effective cost per accepted assembly. A lower unit price does not compensate for an unqualified formulation or an unstable restart condition. Conversely, a specialized material should have a defined technical reason, not simply a more impressive label.
For a quote, provide build quantities and expected repeat frequency alongside material restrictions. Separate a required customer-specified paste from a request for an engineering recommendation. Ask which qualification, cleaning, inspection and documentation activities are included in the assembly scope. These details support a meaningful PCB assembly inquiry without publishing an invented market price or forcing the visitor through a generic calculator.
Questions about solder paste selection
Is Type 5 always better than Type 4?
No. Powder selection serves a deposition requirement within a complete formulation. Confirm the aperture, method and supplier guidance, then evaluate the actual deposits and joints. A higher type number is not a universal quality rating.
Can a paste data sheet define the complete oven recipe?
It supplies material guidance. The actual assembly also introduces component, board and sensor-location constraints. A released oven setup needs measured product temperatures and a justified process window.
Do I need to know the exact paste before requesting assembly?
No. State any customer restrictions and identify the choice as unresolved. Provide the BOM, assembly drawing and intended use so the process team can review the material decision with the correct context.
Specification sources and document control
Use the IPC document revision table to locate the relevant solder-paste and flux standards, then obtain the authorized documents required by the project. This guide does not reproduce paid standard tables or assert a certification. Record the approved edition and the exact supplier documentation in the manufacturing release.
Bring the assembly and process evidence together
Send the board revision, construction, quantity and the assembly process question you need reviewed. Identify unresolved requirements so the response can address them.
Send requirements for reviewOptional: attach the downloaded worksheet manually. This guidance does not certify a design, approve a shipment or replace the applicable authorized standards.