
RAYPCB · Surface engineering
ENEPIG PCB Finish: Ni/Pd/Au, Wire Bonding, IPC & Cost
ENEPIG adds electroless palladium between nickel and gold. It is a candidate when a PCB must support demanding soldering and qualified wire-bond interfaces, but its value comes from controlled Ni/Pd/Au deposition and application testing—not a universal-finish label.
Send preliminary files or an existing fabrication note. Identify the finish decision you need help resolving.
A clear starting point for the finish decision
| Specification item | How to use it |
|---|---|
| Finish system | ENEPIG |
| Standards map | IPC-4556, with revision/amendment stated; board and assembly requirements also apply |
| Thickness planning | Historical planning windows: Ni 3–6 µm; Pd 0.05–0.30 µm; Au 0.03–0.07 µm. Do not treat these as an IPC-4556A acceptance table. |
| Main cost drivers | Added palladium process, three-metal metrology and application-specific bond verification. |
| Acceptance basis | Ordered revision, drawing, measurement, sampling and application-specific evidence. |
Thickness examples and selection guidance are not a complete IPC acceptance specification. State the contracted revision, measurement basis, sampling and application requirements on the order.
Shortlist by the interface your product needs
Choose the primary interface and the constraints that matter. The selector explains candidates and open questions; it does not rank finishes by a fabricated quality score. You can open the relevant finish page or go directly to an enquiry.
RAYPCB ENGINEERING
Surface FinishPCB Surface Finish Selector
Loading PCB Surface Finish Selector…
What the palladium layer changes
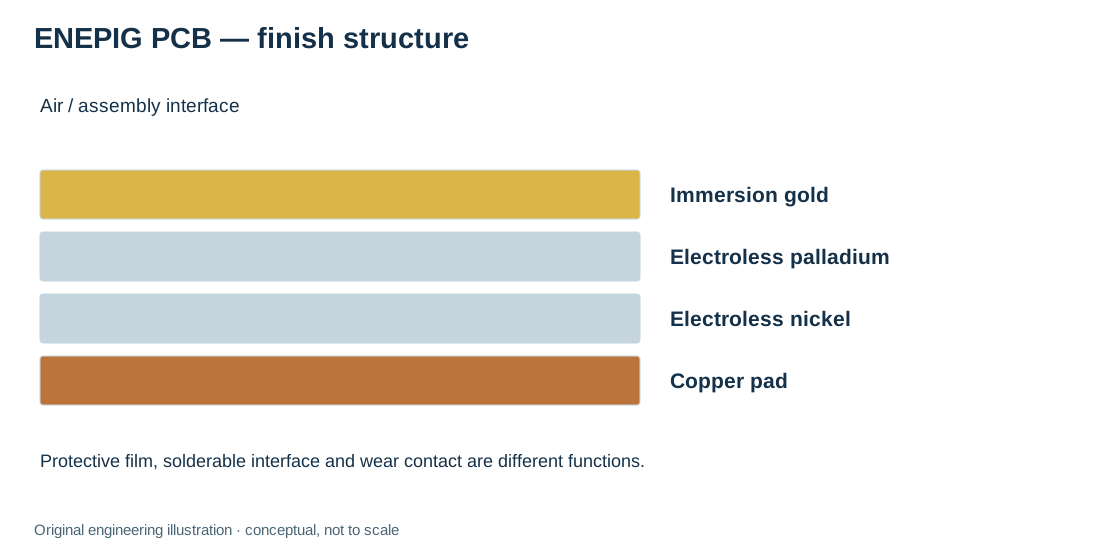
ENEPIG stands for electroless nickel electroless palladium immersion gold. Nickel forms a barrier over copper, palladium separates nickel from the gold process, and the gold cap provides the external surface before assembly. The exact deposit chemistry, composition and layer continuity influence the subsequent solder or bond interface.
The added layer distinguishes ENEPIG from ENIG. It can broaden the useful assembly routes, particularly when a design includes soldering and wire bonding. That does not mean every wire material, bonding machine setting or solder process is automatically qualified. A successful interface depends on the finished deposit and the assembly process working together.
Describe why palladium is needed in the RFQ. If the board only needs ordinary flat solderable lands, ENIG may be worth comparing. If the product has repeatedly mating contacts, electrolytic gold may address wear more directly. Choosing ENEPIG simply because it has more metal layers can add cost without resolving the actual functional requirement.
Metal-thickness readings and unit conversion
Convert readings and summarize one metal at a time. Enter your own comparison limits or leave both blank. The result describes those readings and does not determine IPC lot acceptance. Exact conversion: 1 µin = 0.0254 µm.
RAYPCB ENGINEERING
Surface FinishSurface Finish Engineering Workbench
Loading Surface Finish Engineering Workbench…
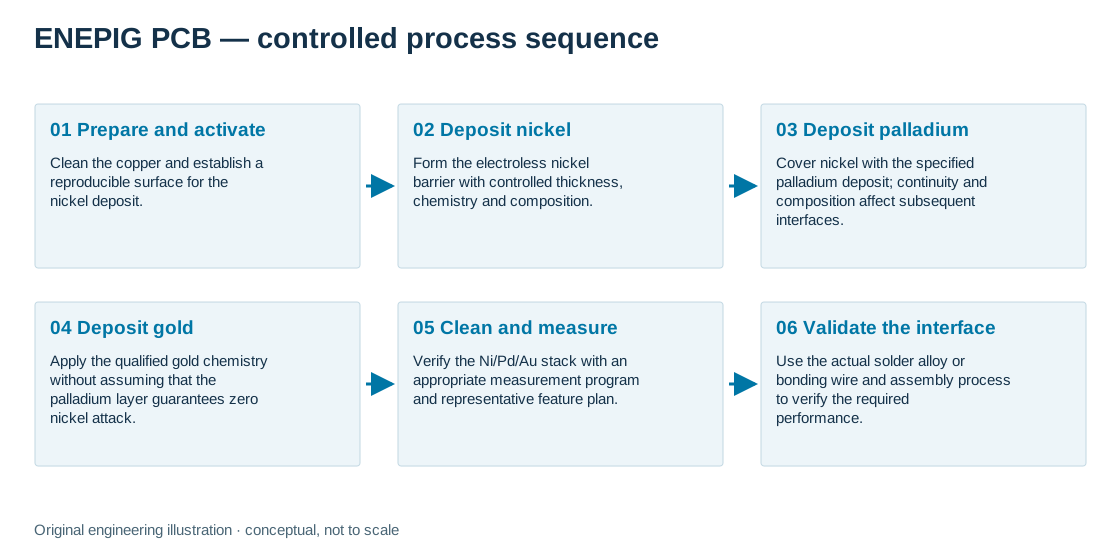
From surface preparation to a controlled release
Follow the sequence below. The optional step player is a conceptual explanation, not factory footage or a production recipe.
- Prepare and activate
Clean the copper and establish a reproducible surface for the nickel deposit.
- Deposit nickel
Form the electroless nickel barrier with controlled thickness, chemistry and composition.
- Deposit palladium
Cover nickel with the specified palladium deposit; continuity and composition affect subsequent interfaces.
- Deposit gold
Apply the qualified gold chemistry without assuming that the palladium layer guarantees zero nickel attack.
- Clean and measure
Verify the Ni/Pd/Au stack with an appropriate measurement program and representative feature plan.
- Validate the interface
Use the actual solder alloy or bonding wire and assembly process to verify the required performance.
Use the agreed IPC-4556 revision explicitly
IPC-4556 is the finish specification family for ENEPIG. The IPC ENEPIG task group identifies its scope, and the ANSI catalogue lists IPC-4556A-2025. State the purchased revision and any applicable amendment in the order rather than relying on an older article or a generic “latest IPC” phrase.
Historical planning windows often cited for discussion are nickel 3–6 µm, palladium 0.05–0.30 µm and gold 0.03–0.07 µm. This page does not present those values as a complete IPC-4556A acceptance table. The actual requirement depends on the contracted document, deposit system, application and measurement plan. Obtain the licensed standard for its detailed acceptance clauses.
Record the three layers separately. A gold reading does not verify palladium continuity or nickel composition. Solderability, bond performance, corrosion evaluation and thickness measurement answer different questions. The quotation should make clear which reports are included and which qualification activities need a separate scope. This avoids treating a material-stack name as proof that every acceptance test has been performed.
Wire bonding needs a specific process definition
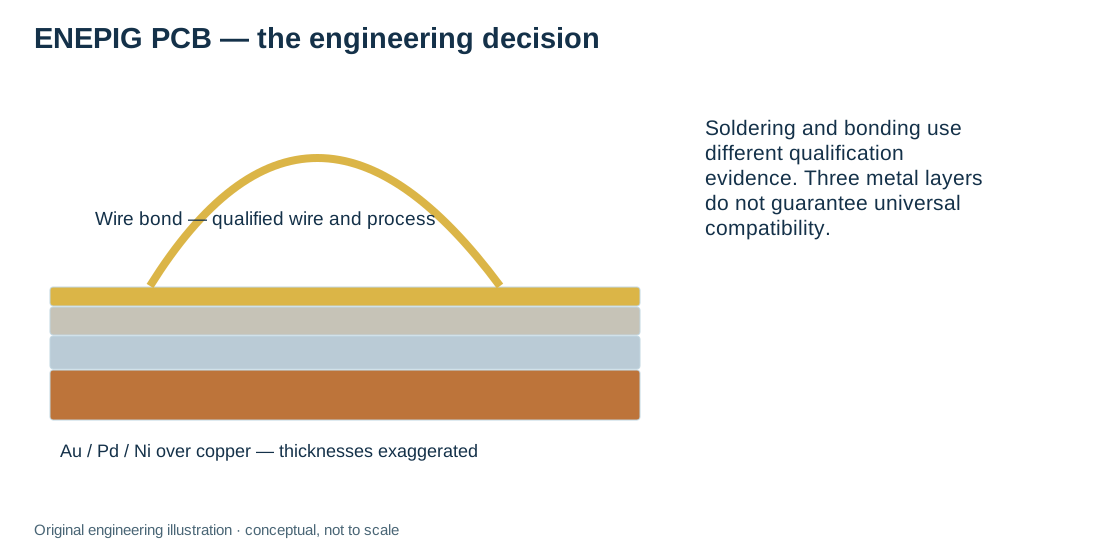
Identify the wire material, diameter, bond type, pad geometry and assembly thermal history. Gold-wire and aluminium-wire bonding are not identical processes. Tooling, surface condition, substrate support and process parameters all influence the resulting bond. The pad finish must be qualified with that actual combination.
Include bondability requirements before fabrication release. A coupon that mirrors the relevant pad geometry and processing history can support qualification, but it should not be assumed equivalent if the actual product has different support, contamination exposure or thermal cycles. Define how results will be related to the delivered board.
Agree the mechanical tests, ageing conditions and acceptance criteria required by the product. A photograph of a bonded wire only demonstrates that a wire was attached; it does not establish pull strength, failure mode or life. If assembly is supplied separately, keep the finish specification and bond-process requirements aligned between the board fabricator and the assembly provider.
ENEPIG and corrosion: reduced risk is not zero risk
The palladium layer changes the interaction between nickel and the gold chemistry, but it does not make process control optional. Nickel corrosion has still been observed in ENEPIG systems. The primary chemistry study from Uyemura discusses that limitation and the role of reduction-assisted gold deposition.
The practical response is to specify a controlled stack and appropriate evidence. Review layer continuity, composition, thickness, rinsing and the accepted corrosion evaluation. Do not use “black-pad free” as an absolute reliability guarantee. A well-qualified process can address a risk without proving that every possible failure mechanism has disappeared.
If the application is sensitive, agree the qualification plan before the first order. Preserve samples and the process traceability needed to investigate anomalies. A brittle solder joint or a weak bond may have multiple contributing causes, including the assembly route. Investigation should consider the full interface and its history rather than assigning every failure to a single metal layer.
Measurement of a three-metal finish
Use a measurement method and model appropriate for gold over palladium over nickel. An ENIG program configured for a two-metal stack is not automatically suitable. The instrument spot size, reference standards, calibration, acquisition and feature geometry should support the thickness range that the purchase order requires.
Identify both monitoring features and functional areas. Large pads make convenient measurement targets but may not represent every small or unusual geometry. If a coupon is used, state its role. Keep the lot, location, measured metal and unit with each reading so that results remain interpretable during receiving and later assembly.
The on-page tool summarizes one metal layer at a time against limits you enter. It deliberately avoids declaring an IPC pass from a handful of numbers. For a real acceptance decision, use the contracted sampling, capability and other criteria. When a reading lies near a boundary, discuss measurement uncertainty rather than rounding it into compliance.
Soldering, RF and mixed-function design choices
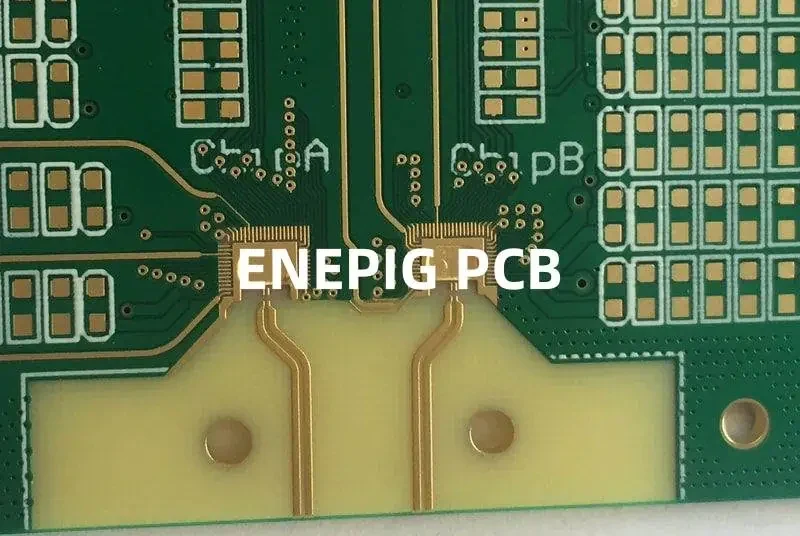
ENEPIG can be selected for a board that combines soldered components with qualified bond pads. The finish supplier's ENEPIG overview describes the intended interface applications. A supplier chemistry capability is not evidence that an arbitrary board layout, thermal cycle or bonding sequence is already validated.
Map the functions on the drawing. A test point, a solder land and a bonding pad may need different surface-history controls even when they share the same finish. Keep handling, cleaning, storage and assembly sequence visible in the process plan. A bond pad exposed to later flux or cleaning may not have the same condition as a freshly finished coupon.
For RF circuits, remember that ENEPIG still contains nickel. Adding palladium does not turn it into a nickel-free conductor. Review the finish with the RF PCB material and geometry choices and measure representative paths where loss matters. If the main objective is a thin nickel-free metallic surface, consider immersion silver together with its corrosion and handling requirements.
When the additional process cost is justified
Compared with a simpler finish, ENEPIG adds a palladium step, a three-layer measurement problem and potentially more demanding application verification. Precious-metal targets, exposed area, lot size, bath loading and qualification scope influence the quote. No universal percentage premium or saving can represent all orders.
Separate the first qualification build from recurring production. Bond trials or additional corrosion and measurement work may be non-recurring, while routine finish inspection remains part of the production route. Ask the quotation to identify those assumptions so the unit price does not hide a mismatch in included evidence.
Send the fabrication files, Ni/Pd/Au requirement, applicable standard revision, quantity and the soldering or wire-bonding process. Include the desired test reports and any mixed-finish boundaries. Request an ENEPIG process and quotation review if the finish is being selected for a specific interface challenge. If that challenge is still unclear, use the surface finish comparison to establish which function actually needs to be improved.
Compare finish allowances and prepare a useful RFQ
Use the same quantity, currency and included scope for both options. Enter a bare-board allowance only if you want it included; leaving it blank produces a finish-only comparison. Setup and inspection or packing are lot charges, while the finish allowance is per board. Enter zero only for a confirmed zero or already-included item.
The comparison exposes the arithmetic behind your inputs. It does not estimate a supplier tariff, promise a yield saving or approve a complex selective-finish route. Changing quantity or finish choice clears the affected allowances so an old assumption is not silently carried into a new scenario. Exact quotes require fabrication files and an agreed finish specification.
RAYPCB ENGINEERING
Surface FinishSurface Finish Cost Comparison
Loading Surface Finish Cost Comparison…
Keep the finish requirement with the design revision
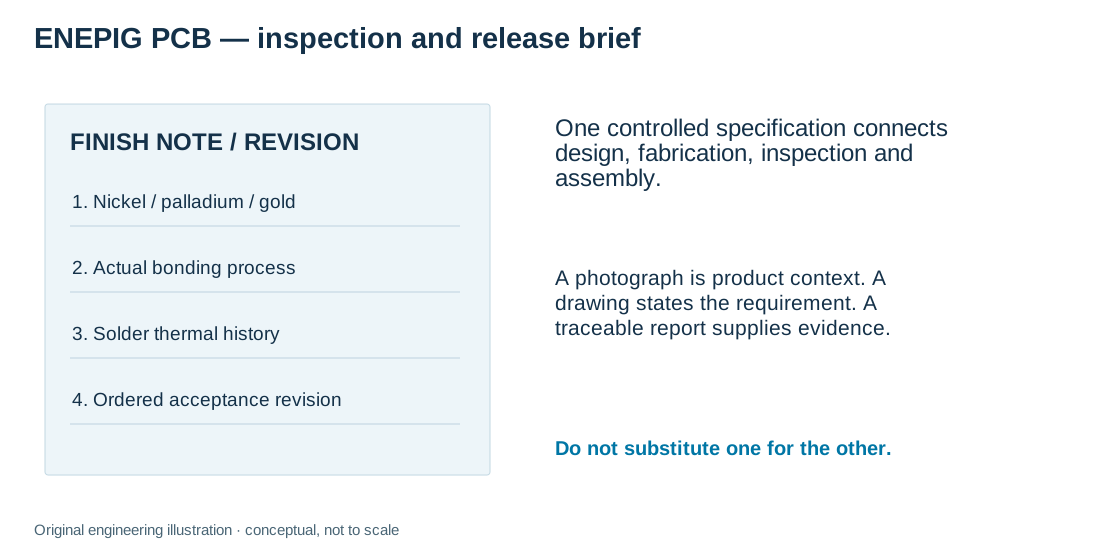
| Include in the enquiry | Why it matters |
|---|---|
| Fabrication files, revision and quantity | Keeps the quotation tied to the correct geometry and build. |
| Finish system and selective area map | Separates solder, bond and contact functions. |
| Standard revision, metal / film requirement and method | Makes the acceptance requirement interpretable. |
| Assembly sequence, storage and service exposure | Identifies the condition in which the interface must function. |
| Required reports and open decisions | Distinguishes supplied evidence from qualification still needed. |
Use the tool download or email draft to carry the current inputs into a discussion. Attach your fabrication data separately. The Contact button opens the enquiry page; it does not automatically transfer calculator parameters or upload files. Preliminary information is welcome when the finish still needs to be selected.
Questions engineers and buyers ask
Does ENEPIG guarantee zero black pad risk?
No. Palladium changes the interface, but deposition control and the relevant inspection and qualification remain necessary.
Is ENEPIG automatically suitable for every wire bond?
No. Specify and qualify the wire, bond method, pad geometry, thermal history and surface condition.
Can the ENIG XRF program be reused unchanged?
Do not assume so. ENEPIG needs an appropriate Ni/Pd/Au measurement model and supporting calibration.
Is ENEPIG nickel-free?
No. It contains a nickel layer beneath palladium and gold.
Continue with a related finish decision
Standards and original technical references
These references support scope and engineering context. Public previews do not contain every licensed acceptance clause. Use the ordered standard revision, agreed drawing and qualified supplier process for production acceptance.