
RAYPCB · SMT tooling
PCB Stencil & SMT Stencil: Design, Types and Cost
A PCB stencil is a patterned foil that places solder paste onto selected PCB lands before component placement and reflow. Choosing an SMT stencil means matching three things: the deposit the assembly needs, the smallest aperture that must release paste, and the printer or fixture that holds the foil. Use this page to compare constructions, check geometry and prepare an enquiry with a clear scope.
Preliminary files are welcome. Identify your board revision, printing equipment and the question you need to resolve.
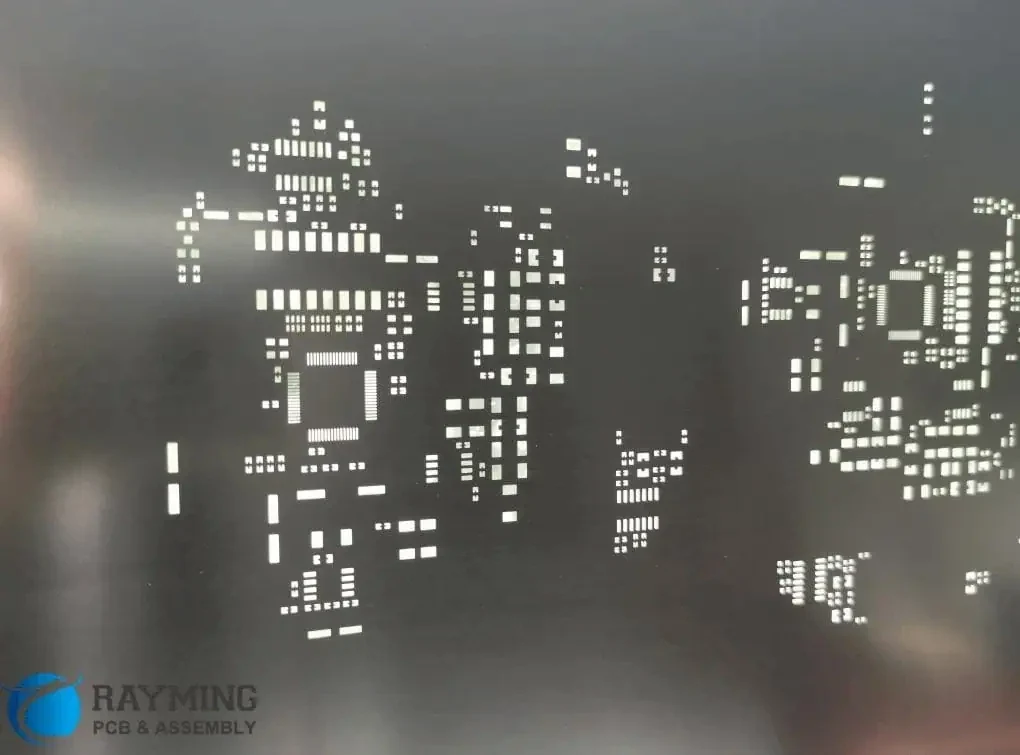
What to establish before the next decision
| Review item | Working requirement |
|---|---|
| Printed material | Identify solder paste, adhesive or another controlled application before selecting apertures. |
| Mounting | Specify frame or reusable holder; confirm usable area independently of outer dimensions. |
| Foil profile | Compare one thickness with local zones using the real aperture families. |
| Critical geometry | Review opening area, perimeter, thickness and package-specific patterns. |
| Release evidence | Agree tool inspection and print validation as separate tasks. |
Find the resource for your printing task
Select the available mounting equipment and the issue you need to resolve. The guide suggests relevant next pages without assigning an unsupported quality score or forcing you through a quotation form.
RAYPCB ENGINEERING
Stencil EngineeringStencil Route Selector
Loading Stencil Route Selector…
Start with the assembly, then choose the stencil
The solder paste layer is a manufacturing instruction, not simply a copy of every exposed copper feature. Test points, gold contacts, tooling holes and unpopulated positions may need no paste. A package's exposed pad may need several openings even though its copper land is continuous. This is why a stencil order should include the assembly variant and design revision, rather than only a screenshot of the board.
For a new product, identify the most difficult deposit families: fine-pitch perimeter leads, small chip components, bottom-terminated devices and large connector or power lands. Compare their requirements before selecting one foil thickness. A convenient thickness for the smallest opening may provide too little material elsewhere. A thick foil chosen for a large connector may make small openings difficult to release. The decision is a balance that the printing trial must verify.
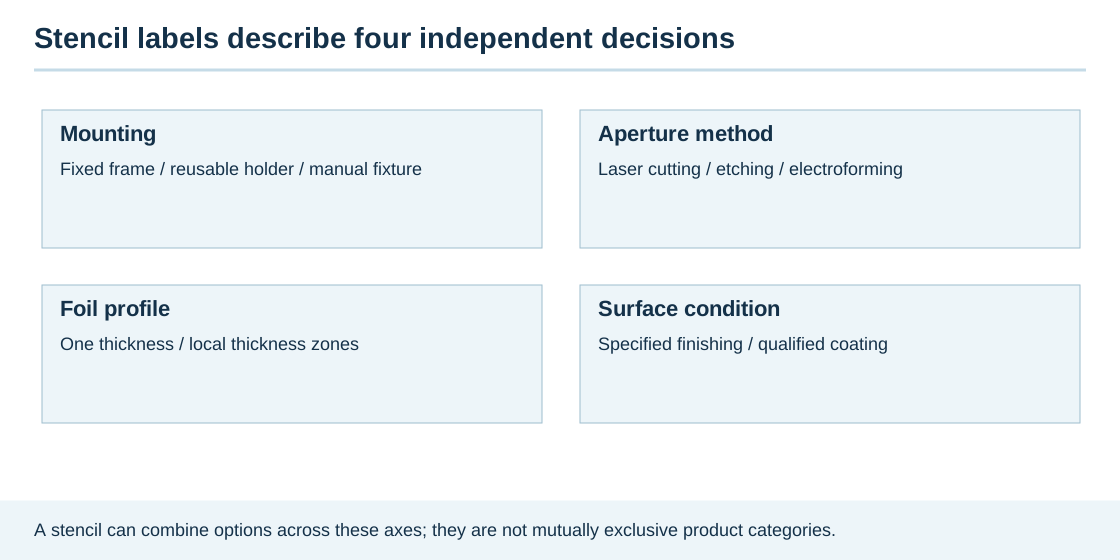
Compare stencil types on separate axes
Framed and frameless describe how the foil is held. Laser-cut, chemically etched and electroformed describe how apertures are made. Single-thickness and stepped describe the foil profile. Electropolishing and coatings describe additional surface treatments. These labels are not mutually exclusive product categories: a laser-cut stencil can be frameless, stepped and coated at the same time.
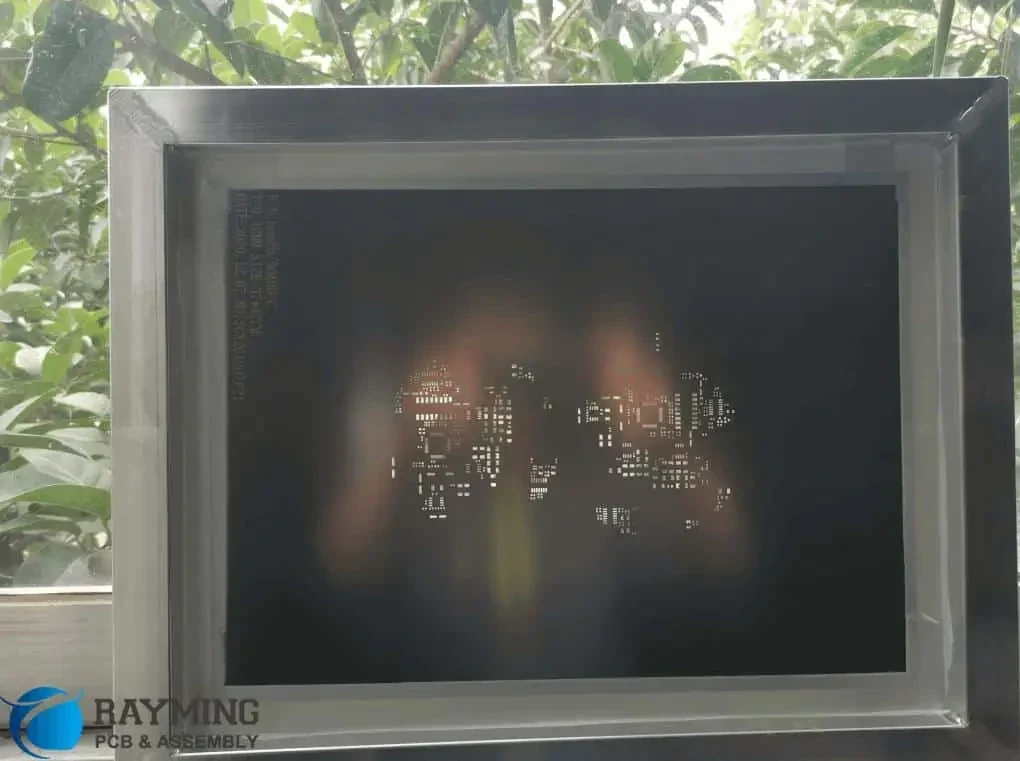
A fixed frame keeps the foil with its dedicated support assembly. A frameless foil uses a specified reusable tensioning system or a suitable manual fixture. It is incorrect to assume that all frameless foils are for hand printing. For mounting details, use the frameless stencil ordering guide. Where component groups require different deposits, compare the stepped stencil construction with aperture changes, dispensing or another qualified route. Do not buy extra process features before identifying the problem they are meant to solve.
Aperture, thickness and paste-volume workbench
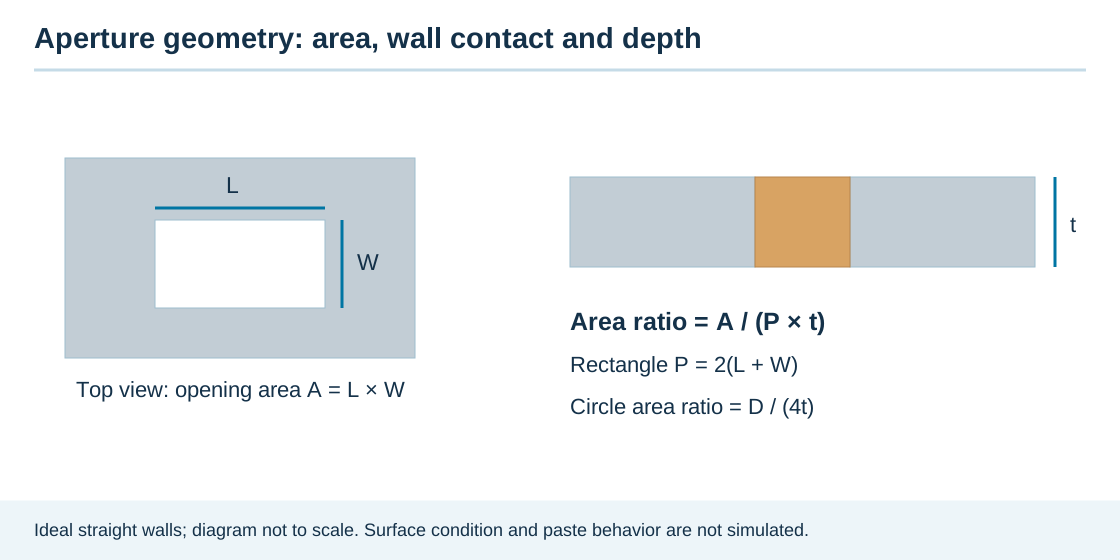
Enter the finished opening dimensions and local foil thickness. The rectangle uses A = L × W and P = 2(L + W). A circle uses A = πD²/4 and P = πD. For a rounded rectangle, A = LW − (4 − π)r² and P = 2(L + W) − (8 − 2π)r. The model assumes a constant section through the foil.
Area ratio is A/(P × t); geometric opening volume is A × t. Keep dimensions in millimetres, with foil thickness entered in micrometres: 100 µm = 0.10 mm. The thickness comparison holds the opening unchanged, so the tradeoff is visible. The maximum thickness at your entered target is a geometric ceiling for that target only, not a recommended or commercially available foil.
Transfer efficiency is an explicit scenario input. Multiplying geometric volume by that percentage estimates printed paste for the scenario; it does not calculate metal volume after reflow. The familiar 0.66 area-ratio reference is editable and must not be treated as an IPC pass certificate or a guarantee of paste release.
RAYPCB ENGINEERING
Stencil EngineeringStencil Design Workbench
Loading Stencil Design Workbench…
Thickness selection needs opening geometry
Component pitch gives useful context, but the aperture width and length determine the opening area. Thickness supplies the third dimension of geometric paste volume and also increases the wall area that the paste contacts. The design workbench therefore shows both volume and area ratio as thickness changes. It does not assign a universal thickness from a package name.
For a rectangular opening measuring 0.25 × 0.60 mm in 0.10 mm foil, geometric volume is 0.015 mm³ and area ratio is approximately 0.882. At 0.15 mm foil, the same opening has 0.0225 mm³ volume but an area ratio of approximately 0.588. The added volume comes with a more demanding release geometry. These are arithmetic examples, not approved apertures. Compare the actual paste, wall finish and process with the component manufacturer's attachment guidance.
Plan tooling cost without hiding the assumptions
The planner uses allowances you enter; it has no live supplier tariff. Enter the number of physical stencils or foils, not the number of boards. Per-stencil foil, mounting and special-process allowances are multiplied by that quantity. Engineering/setup and freight are added once for the lot.
Planning total = stencil count × (foil/cutting + mounting + special processes) + lot engineering + lot freight. Enter zero only for a confirmed included or zero-cost item. Blank fields remain unknown. Changing quantity, construction, mounting or currency clears the allowances so a previous scope is not silently reused. The optional assembly quantity allocates the same tooling total across a build; it does not change the tooling price.
The result excludes taxes, duties and any service you have not entered. A coating, local step or unusual interface requires a supplier review even when you have entered an allowance. If you do not have rates, use the direct enquiry button. The useful output is a clear scope and an honest list of open items, not a fabricated instant market price.
RAYPCB ENGINEERING
Stencil EngineeringStencil Cost and RFQ Planner
Loading Stencil Cost and RFQ Planner…
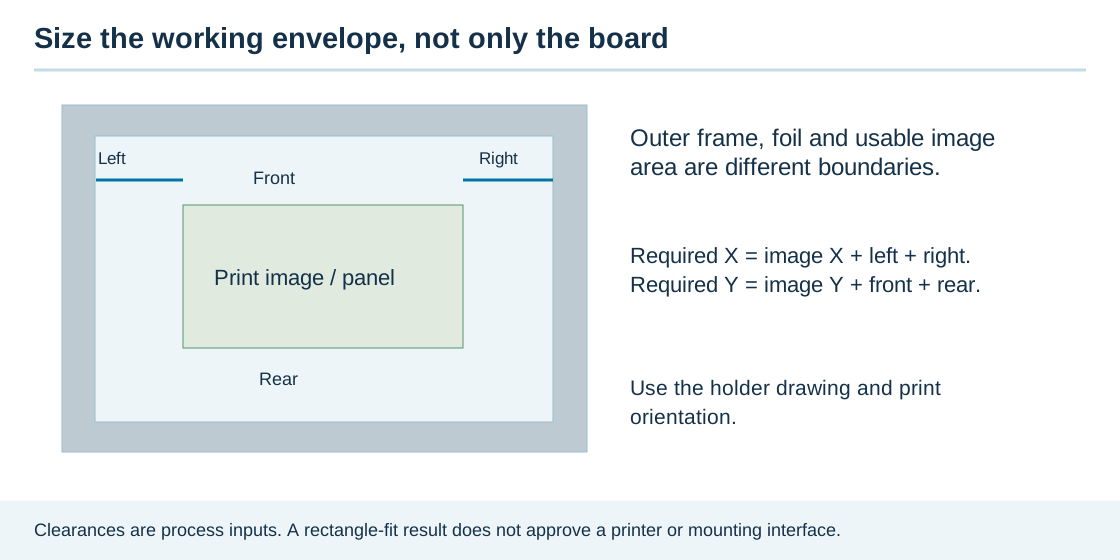
Size means more than the outside dimensions
Record outer frame size, foil size, usable image area and PCB or panel size separately. A frame that fits inside a printer can still leave insufficient blade travel or paste-roll clearance around the image. A foil that covers a small PCB may not match the clamping pattern of a reusable holder. Include the printer model or holder drawing in the enquiry.
Keep the production panel in its intended orientation. Rails, fiducials, tooling features and the direction of the printing stroke influence registration and support. Combining top and bottom patterns on one foil is a layout decision, not a free substitute for two stencils: both patterns must fit the usable area without interference, and the operator needs an unambiguous side reference. The SMT stencil selection guide provides a task-by-task sequence for resolving these details.
Follow the working sequence
The steps remain readable without animation. Use the optional player to follow one operation at a time; it starts paused and respects reduced-motion preferences. This is a conceptual explanation, not a production video.
- Support
Locate and stabilize the board or panel.
- Align
Match the approved stencil to the correct side.
- Print
Use the defined material and controlled recipe.
- Separate
Release the board without disturbing the deposit.
- Inspect
Check the printed material before placement.
- Continue
Release or correct according to the assembly process.
Aperture design and QFN thermal pads
An aperture reduction changes the paste pattern relative to the copper land. Uniform percentage reductions are not appropriate for every device or every dimension. For example, reducing both length and width to 90% leaves 81% of the original area. Specify whether a requested reduction concerns width, length or total area so that engineering and purchasing are discussing the same geometry.
Large exposed pads often use segmented openings to distribute paste. Window count, web width and edge margins jointly determine nominal coverage. That coverage does not predict the final void percentage. Vias, paste chemistry, placement and reflow also affect the result. Use the QFN aperture and exposed-pad guide for package-specific review, and the solder paste deposit workbench when the immediate task is understanding area ratio and volume rather than selecting a mounting format.
What changes the stencil price?
Compare quotations on a common scope: number of foils, image size, frame or holder interface, aperture-making method, local thickness changes, finishing, identification, inspection and packaging. Shipping can be significant when a frame is large compared with the board. A small frameless foil may reduce shipping volume, but only if compatible equipment is already available.
The cost planner accepts your own supplier allowances or internal budgets. It separates recurring foil costs from lot engineering and freight, and can distribute tooling cost across a planned assembly quantity. No live RAYPCB tariff is connected. Request a file-based quote if rates are unknown; completing a calculator is not required. For repeat products, include revision stability and the expected number of reorders when comparing the total ownership cost of different mounting systems.
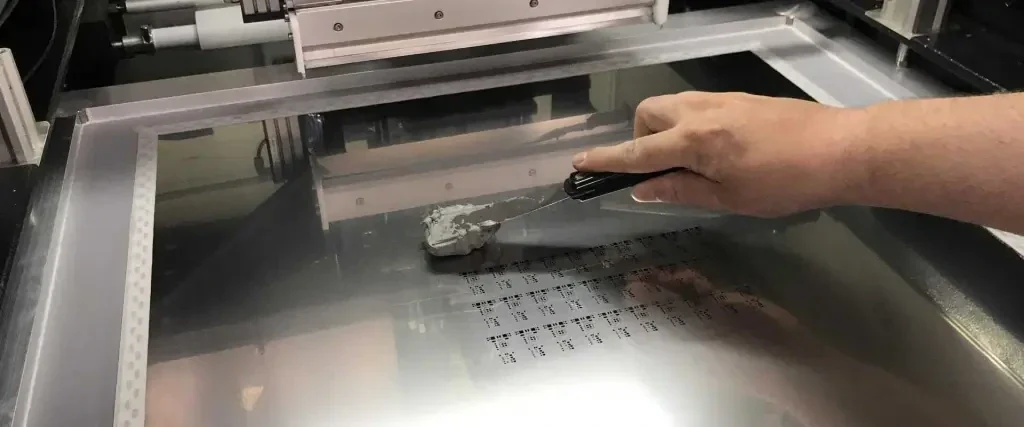
From a stencil enquiry to an assembly build
Send paste-layer data, board outline, assembly drawing and revision, along with stencil-side identification and the required mounting interface. If aperture optimization is requested, identify the critical packages and supply their manufacturer attachment notes. Agree who approves modifications and keep the approved stencil artwork with the PCB release.
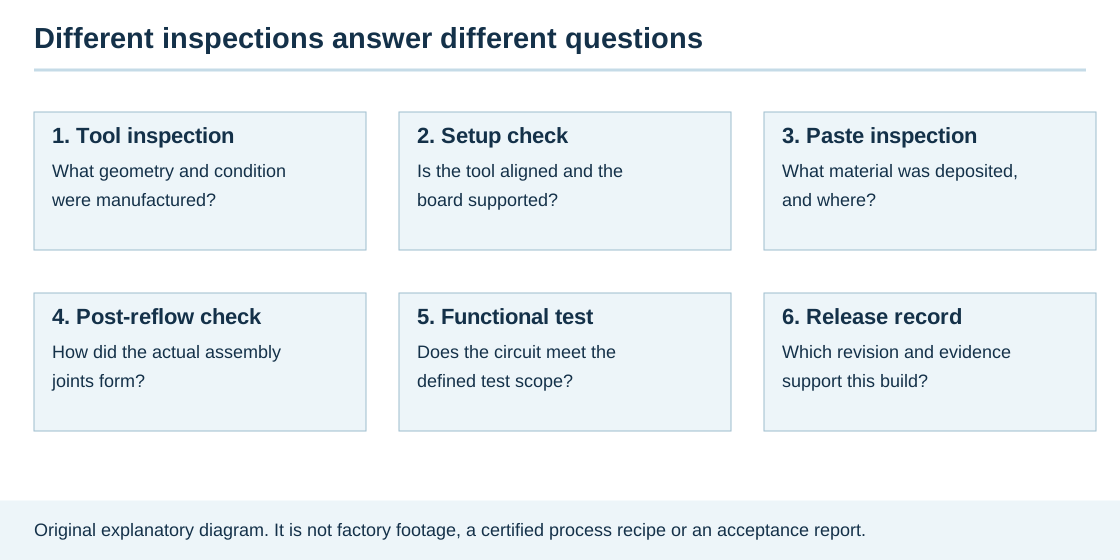
If you need populated boards, use PCB Assembly services to include procurement, placement, soldering and the agreed inspection or test scope. Stencil inspection checks the tool; solder paste inspection checks the deposited material; post-reflow inspection checks a later process state. None replaces the others. Keeping those responsibilities explicit makes an enquiry more useful than requesting a generic “high-quality stencil” without the files and process context.
Keep the enquiry connected to manufacturing evidence
Send a brief an engineer can act on
Include the paste artwork, board or panel outline, side and revision; describe the printer, holder or manual fixture. Identify critical components and the exact decision that remains open. For an existing process problem, add the observed location, relevant conditions and available inspection evidence. Keep files and photographs tied to the same revision.
State whether you need stencil fabrication only or a populated-board project. PCB Assembly services can address the broader scope of procurement, placement, soldering and agreed inspection or test. The assembly process guide explains how the printing step connects to the rest of the build.
Download the current tool brief or open an email draft when you want to share the calculation. Attach design files separately. The Contact link opens the existing enquiry page; it does not silently transmit calculator values or claim an integrated Gerber upload. You can enquire before completing a tool when your question is about the manufacturing route rather than a numeric result.
Questions about this stencil task
What is the difference between PCB stencil and SMT stencil?
In this context both terms describe tooling for material deposition during surface-mount assembly, usually solder paste. The useful specification is the material, aperture design, foil construction and mounting interface. A keyword alone does not define an order.
Can you quote before I have selected a thickness?
Yes, you can request a design and quotation review with preliminary files and critical component details. Mark the thickness as open rather than inventing a value. The engineer needs the actual paste geometry and assembly context to evaluate candidates.
Does this calculator approve a stencil for production?
No. It makes its stated geometry or arithmetic visible. It does not inspect your files, predict paste release or certify compliance with an IPC standard. Use the result alongside the actual drawing, component guidance, qualified process and agreed inspection evidence.
What information helps if I am unsure about the next step?
Send the current design revision and describe the unresolved task: mounting fit, deposit geometry, process behavior or quotation scope. Include the relevant equipment and component details. Preliminary information is acceptable when its status is clear; approval of a production tool requires the agreed final data.
Continue with the next useful decision
Original engineering and standards references
Use component and process documents in their stated application context. Public IPC contents establish scope, not every licensed clause. Specify the agreed standard revision and acceptance requirements on the order; this guide does not claim universal IPC certification for a geometry calculation.