
RAYPCB · Design to manufacturing
PCB DFM: check the risks before you release the files
Design for manufacturability connects your PCB layout, fabrication data and assembly requirements to the process that will build them. Check critical geometry, identify missing decisions and prepare a clear engineering review request.
Have an unresolved layout question? Send preliminary files and identify the revision. You can enquire without completing the tool.
What is PCB DFM—and what should it tell you?
PCB DFM is the review of a printed circuit board design and its manufacturing data against the intended fabrication process. Its useful output is a set of specific findings, the reason each matters and a documented action. It should help resolve ambiguous files and manufacturing risks before tooling or production begins.
A review needs more than the smallest trace on the board. The same feature may need different treatment with heavier copper, a different hole structure or a special surface finish. Start with the actual build requirements and the rigid PCB capability tables; confirm which limits apply together. Published individual limits do not establish feasibility for every combination.
| Review | Primary question | Typical evidence |
|---|---|---|
| CAD DRC | Does the design meet the rules configured in the CAD project? | Connectivity, clearances and constrained objects inside the design database. |
| Fabrication DFM | Can the released data be built by the intended process? | Gerber/drill data, layer mapping, stackup, drawing, tolerances and process rules. |
| DFA | Can the chosen components be assembled and inspected? | BOM, land patterns, paste data, placement, component access and process needs. |
| DFT | Can the agreed faults or functions be tested? | Test access, programming, fixtures, coverage expectations and acceptance criteria. |
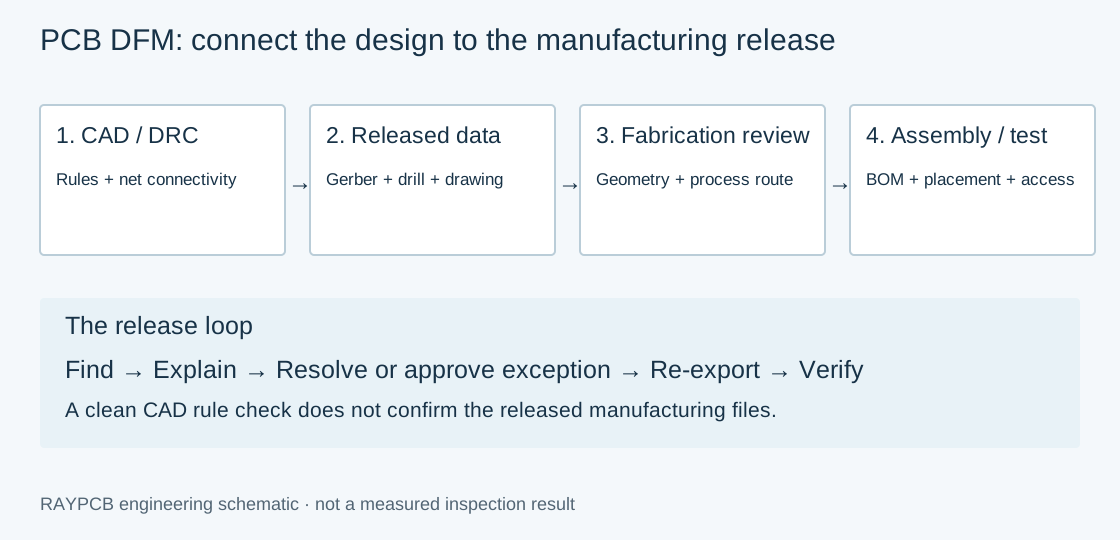
PCB DFM online tool: geometry and release preflight
Use the workbench before you send the package. Enter dimensions from your layout or drawing and the limits agreed for your construction. The worked example explains the calculations; its values are not RAYPCB manufacturing specifications.
What this tool actually checks
Six entered-parameter checks: trace width, copper spacing, routed-edge clearance, remaining annular ring, through-hole aspect ratio and nominal solder mask web. It also records 15 self-reported file and release checks. It does not read Gerber geometry, detect shorts or approve manufacture.
RAYPCB ENGINEERING
Quote and DFMPCB DFM Geometry and Release Preflight
Loading PCB DFM Geometry and Release Preflight…
For a real board-wide review, submit the released fabrication data. No account or file upload is required to use this preflight.
PCB DFM checklist: the checks that change a build decision
| Area | Review in the released files | Decision to resolve |
|---|---|---|
| Copper geometry | Minimum trace and spacing, isolated copper, narrow thermal spokes and local neck-downs. | Which layer and copper process control the rule? Does a proposed change affect current or impedance? |
| Holes and slots | PTH/NPTH intent, drill size, finished-hole tolerance, slots, annular rings and drill-to-copper. | Confirm plated versus non-plated features, lead fit, registration allowance and mechanical clearances. |
| Stackup | Layer order, copper weights, total thickness, dielectric construction and impedance notes. | Approve a manufacturable stackup and material/substitution policy before critical geometry is frozen. |
| Mask and legend | Mask openings, retained webs, mask-to-copper registration and legend over exposed pads. | Keep required solderable surfaces open; preserve readable reference and polarity marks. |
| Outline and panel | Closed outline, routed cutouts, score lines, break tabs, copper setbacks and tooling rails. | Identify the delivered unit and who owns panelization; avoid conflicting outline definitions. |
| Assembly | BOM/placement agreement, DNP, orientation, paste openings, supports and component clearances. | Resolve package or placement ambiguity before stencil and assembly preparation. |
| Test and release | Netlist comparison when applicable, test access, revision consistency and approved changes. | Define what inspection/test will verify and retain the approved final release. |
A minimum-spacing rule is not a complete electrical-insulation design rule. Operating voltage, environment and the relevant product requirements can demand different clearances or creepage. Similarly, a trace that can be etched may still be unsuitable for its current or signal requirement. Keep manufacturing, electrical and safety reviews connected without treating one as proof of the others.
Hole checks: use a tolerance budget, not a nominal picture
For a circular pad and drilled hole, the nominal radial ring is half the difference between their diameters. To explore registration, subtract a radial allowance. Use a minimum pad diameter and maximum drilled diameter when those tolerances are known. Finished-hole size after plating is a separate drawing requirement; do not silently substitute it for the drill tool diameter. For a compliant connector, compare the complete press-fit hole tolerance window with its application specification.
Worked example: minimum pad 0.60 mm, maximum drilled diameter 0.35 mm and radial registration allowance 0.05 mm give (0.60 − 0.35) / 2 − 0.05 = 0.075 mm remaining ring. Against an entered 0.10 mm project rule, the tool asks for review. The example does not establish an IPC class or an allowable breakout.
Increasing pad size may reduce nearby spacing. Reducing a hole may conflict with component lead fit. A useful finding therefore records both the affected geometry and the constraints on the proposed change.
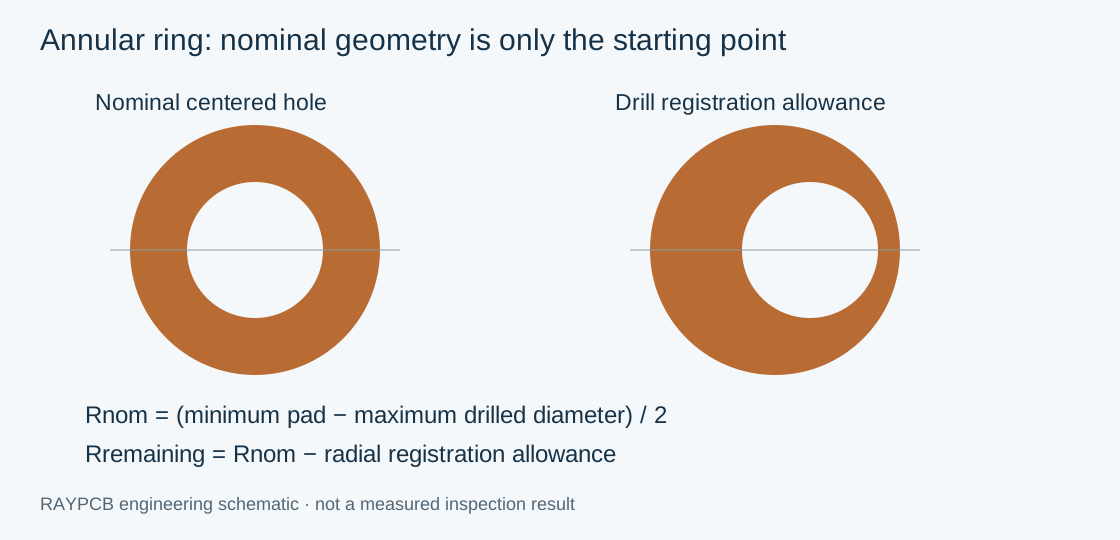
Drill-to-unrelated-copper clearance is different from annular ring. Evaluate the actual hole boundary, nearby copper on every relevant layer, drill tolerance and layer registration. Inner-layer antipads and thermal connections also need review. The online tool calculates one entered circular-pad budget; it does not discover every hole or nearby conductor in a board.
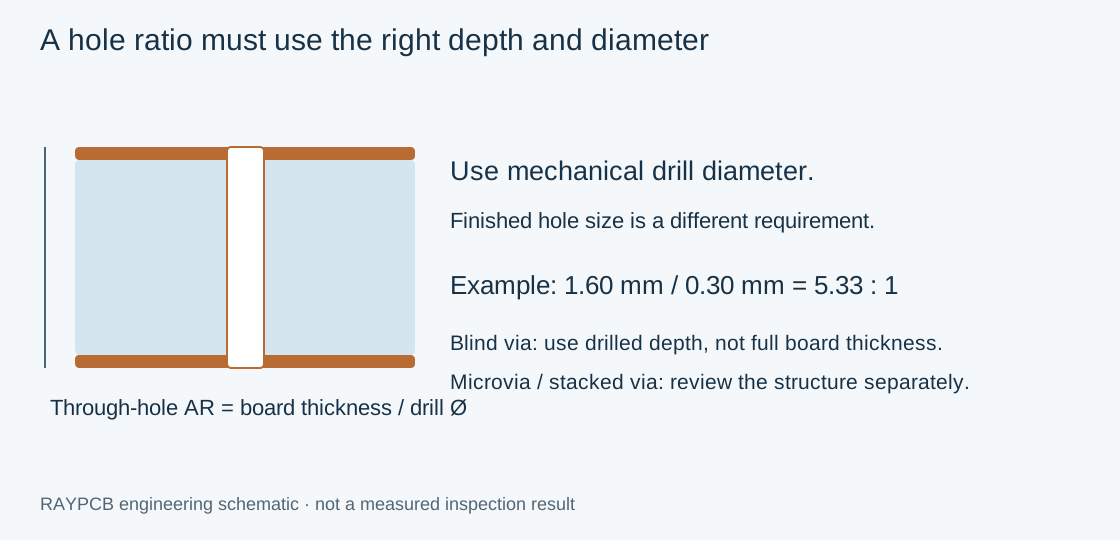
For the illustrated through-hole, 1.60 mm board thickness divided by a 0.30 mm mechanical drill gives 5.33:1. Whether that is acceptable depends on the qualified drilling and plating route. A blind-hole calculation uses its drilled depth, while laser microvias and stacked structures require additional structural review. Select the special-route option in the tool to avoid receiving a through-hole comparison for these constructions.
Mask, copper and legend: resolve what must remain exposed
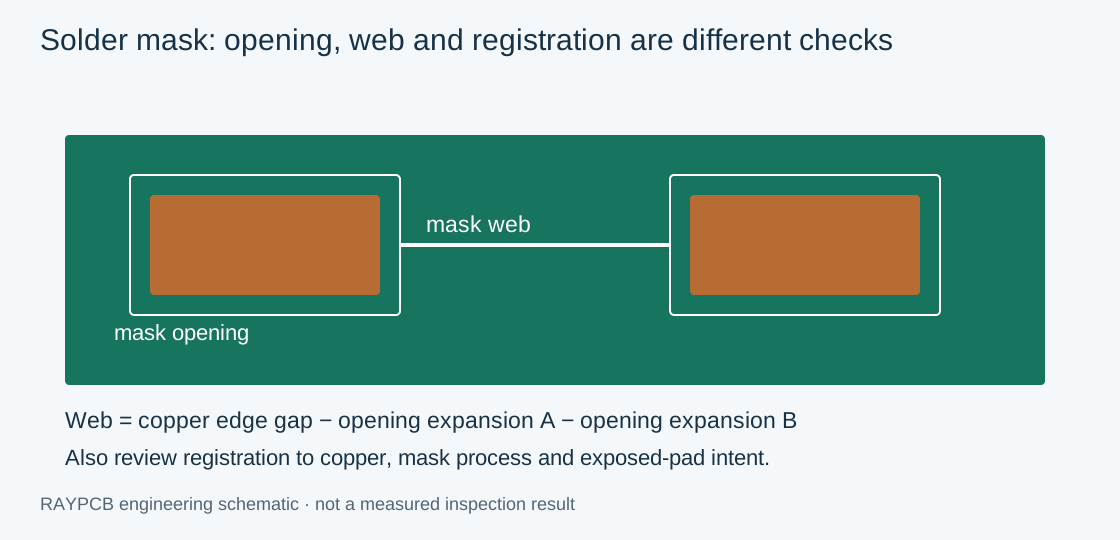
A solder mask opening exposes copper; expansion describes how its boundary differs from the copper feature. The web is the retained mask between neighboring openings. For two separately expanded edges, nominal web = copper edge gap − expansion A − expansion B. With a 0.15 mm gap and 0.05 mm expansion on each edge, the nominal web is 0.05 mm.
That number alone does not establish a reliable mask feature. Registration, process resolution, material, geometry and the agreed artwork affect the result. If a web cannot be retained, discuss whether a shared opening is acceptable for the component and assembly process. Do not quietly merge openings where the change can affect solder bridging or pad definition.
Legend should support assembly and inspection without contaminating intended solderable surfaces. Check polarity and pin-one marks, clipping around openings, and readability after component placement. If the fabricator proposes clipping text, confirm that useful identification survives. Avoid treating a generic recommendation about text size as a guaranteed limit for every legend process.
Confirm the construction before tuning fine geometry
Include the layer sequence, finished board thickness and tolerance, copper requirements, material constraints and any controlled-impedance instructions. A material name by itself does not define a stackup. For multilayer work, coordinate the multilayer construction and stackup before choosing a fine-line target.
For controlled nets, specify the target impedance, tolerance, reference layers and relevant test or coupon requirements. Use the PCB impedance calculator and design guide to explore geometry, then obtain confirmation against the actual fabrication stackup. Changing a trace solely to satisfy a manufacturing check can change its electrical behavior.
Heavy copper, fine-pitch via-in-pad, sequential lamination, flex bend regions and metal-based constructions need process-specific reviews. Label those features in the fabrication notes instead of expecting them to be inferred from a conventional Gerber layer set. An unresolved special requirement is a reason to ask an engineering question early, not to declare the entire design impossible.
What a useful DFM issue report looks like
Ask for findings you can locate and act on: the design revision, layer or feature, measured condition, applicable rule and its source, proposed disposition, owner and closure evidence. Severity should describe the consequence or missing decision; a red marker without context is difficult to resolve.
Illustrative report below: these are teaching examples, not customer data or results from a RAYPCB manufacturing inspection.
| Finding | Evidence / concern | Proposed disposition | Closure evidence |
|---|---|---|---|
| F-01 · Hole ring | Example circular pad budget leaves 0.075 mm; project rule entered as 0.10 mm. | Designer and fabricator review pad, hole and registration assumptions; check neighboring spacing. | Approved geometry and re-exported layers; repeat the check. |
| F-02 · File ambiguity | Drawing calls for a plated slot, but the supplied drill package does not identify slot plating. | Confirm the intended plated feature and issue one unambiguous drawing/drill release. | Matching revision, slot definition and CAM interpretation. |
| F-03 · Assembly query | An exposed-pad component has no confirmed paste-window requirement. | Review the component application guidance and stencil proposal. | Approved paste data and assembly instruction tied to the component revision. |
A response can approve a specific proposed change, request a corrected file, or document an accepted exception with the responsible parties. Preserve the original and final revisions. If CAM data is modified, identify which changes affect the design and obtain the appropriate approval; do not assume an automated repair is electrically neutral.
Close the review before releasing the next revision
This optional step player illustrates the review loop. The complete sequence stays visible without JavaScript. It starts paused; use the controls to advance, and keep the final file set tied to the decision record.
- Define the build
Record material, stackup, copper, holes, finish, quantity and the intended assembly or test scope.
- Export and reopen
Generate the final fabrication package. Inspect layer mapping, units, polarity and outline in a suitable viewer.
- Review findings
Locate each issue and compare the actual feature with the applicable process rule.
- Agree the disposition
Assign an owner. Approve a specific change, supply missing information or record an agreed exception.
- Verify the release
Re-export after edits, recheck affected features and remove superseded alternatives from the production package.
When PCB DFM becomes an assembly or test question
For component clearances, package selection and BOM-to-placement consistency, use the PCB Design for Assembly (DFA) guide and tools before the populated-board release.
A bare board can satisfy its fabrication drawing while remaining difficult to populate. Small component-to-component gaps, inaccessible joints, thermal imbalance or mismatched land patterns need an assembly review. Compare the package manufacturer's recommendations with the actual footprint and paste definition. The PCB stencil design workbench supports aperture and thickness planning; it does not replace package-specific guidance.
For a populated build, send the BOM with clear MPNs and DNP instructions, placement data, assembly drawing and any programming or test requirements. A coordinate file alone cannot resolve an ambiguous component orientation. Identify the origin, board side convention and revision.
PCB Assembly services cover a different scope from bare-board fabrication. Agree how solder-joint inspection, electrical testing and functional verification will be used. The comparison of AOI, X-ray, ICT and functional test helps distinguish their purposes and gaps; no single method proves all product functions.
How DFM choices affect cost and lead time
DFM creates value when it resolves a real process constraint or avoids an unclear release. Trace and spacing requirements, drill structures, copper weight, stackup, special via processing and panel utilization can change the manufacturing route. The effect is specific to the job; there is no credible universal percentage saving from “passing DFM.”
Ask for a matched comparison when evaluating a change: keep quantity, delivery basis, materials, finish and test scope constant, then identify the cost driver being changed. A larger hole may simplify one operation but fail a mechanical requirement. Fewer layers may reduce one cost while making routing or electrical performance unacceptable.
Before adopting a cost-driven change, use the fabrication design trade-off and payback review to keep functional requirements, validation work and affected inventory visible beside the proposed saving.
Separate the time waiting for a design decision from the agreed manufacturing lead time. Send the needed delivery date with the enquiry so feasibility can be reviewed. This page does not promise a fixed DFM turnaround or an automatic instant quotation. A complete, internally consistent file package gives the team a better basis for both questions.
Prepare a file package an engineer can review
Use the PCB file-format and export guide to identify each manufacturing output and prepare a revision manifest. If the original design is missing, first define the evidence and validation scope with the PCB-to-schematic recovery workflow.
For PCB fabrication
- Gerber layers with an unambiguous layer map and board outline.
- Drill/rout data with PTH, NPTH, slots and units identified.
- Fabrication drawing: dimensions, tolerances, stackup, material, copper and finish.
- Impedance requirements and a netlist where applicable and agreed.
- Board revision, quantity, required date and highlighted open questions.
Add for assembly
- BOM, approved alternatives and DNP instructions.
- Placement data, origin, rotations, board sides and assembly drawings.
- Paste layers and critical package or soldering instructions.
- Programming, test, inspection and first-build acceptance requirements.
- Any constraints on substitutions or engineering changes.
If you use another manufacturing data format, confirm acceptance before relying on it. Include one authoritative release rather than several unexplained alternatives. Use a PCB prototype build when the next task is to validate the design, and record what that build needs to prove.
Have the files—or just one difficult feature?
Send the available revision and ask the specific question. Attach the downloaded tool brief if it helps explain your geometry or open decisions. The enquiry page opens separately; this page does not upload files or silently transfer your inputs.
PCB DFM questions
Does a clean DRC result mean my PCB is manufacturable?
It means the checks you ran found no violations of the configured rules. It does not prove that all necessary rules were configured, the exported data matches the design, or the complete construction fits the intended manufacturing route.
Can this online tool check my Gerber files?
No. It screens dimensions and limits entered by you, and records self-reported readiness items. It does not parse Gerber or drill geometry. Submit the released files for a board-wide engineering review; use a CAD or Gerber viewer to inspect exports first.
Which IPC standard should I specify?
The applicable design, qualification/performance and acceptability documents have different roles. For rigid boards, discuss the appropriate IPC-2220-series design requirements, IPC-6012 performance requirements and IPC-A-600 acceptability criteria, including the agreed revisions, class and exceptions. A generic “IPC compliant” statement is not a complete purchasing specification.
Are the tool example limits RAYPCB capabilities?
No. They are illustrative inputs chosen to demonstrate the calculations and review flags. Replace them with limits confirmed for your stackup, copper and process, and record the source. The tool never grants production approval.
Does PCB DFM include BOM and functional testing?
Fabrication DFM focuses on the board data and build route. BOM, placement and soldering belong to the assembly review; test requirements must be agreed separately. State the requested scope so a bare-board review is not mistaken for complete product verification.
What should I do after changing a flagged feature?
Check interactions with neighboring copper, mechanics and electrical requirements, then regenerate the affected manufacturing outputs. Keep the approved revision and issue closure together. Editing a CAD object without replacing its old exported files leaves a release mismatch.
Will the online preflight save or upload my design information?
This tool processes entered values locally and does not send them to analytics or a server. A download stays on your device. An email draft contains a short summary that you can edit; it is sent only when you send it in your mail application. The separate Contact page has its own submission process.
Separate connectivity intent from file consistency
For questions about opens, shorts or the difference between a net and a netlist, read the PCB nets explanation and connectivity lab. Provide the intended revision and relevant references when requesting a manufacturing review.
Primary engineering references
Use these original sources for the roles of standards, exported manufacturing data and CAD/CAM checks. Apply the requirements for your actual product and agreed process; the examples on this page do not reproduce a licensed acceptance standard.

