
BGA Assembly: Process & Inspection
Plan the joints you cannot inspect from the top of the board.
BGA assembly mounts a ball-grid-array component onto a PCB. This page covers board attachment, process preparation and inspection; it does not describe manufacturing the semiconductor package itself. Package-specific assembly guidance and the actual board construction govern the build.
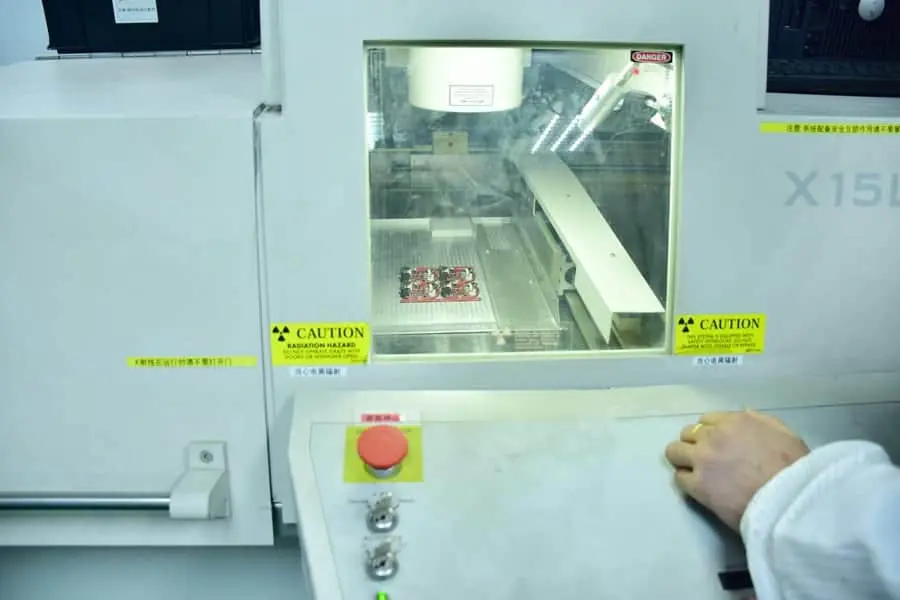
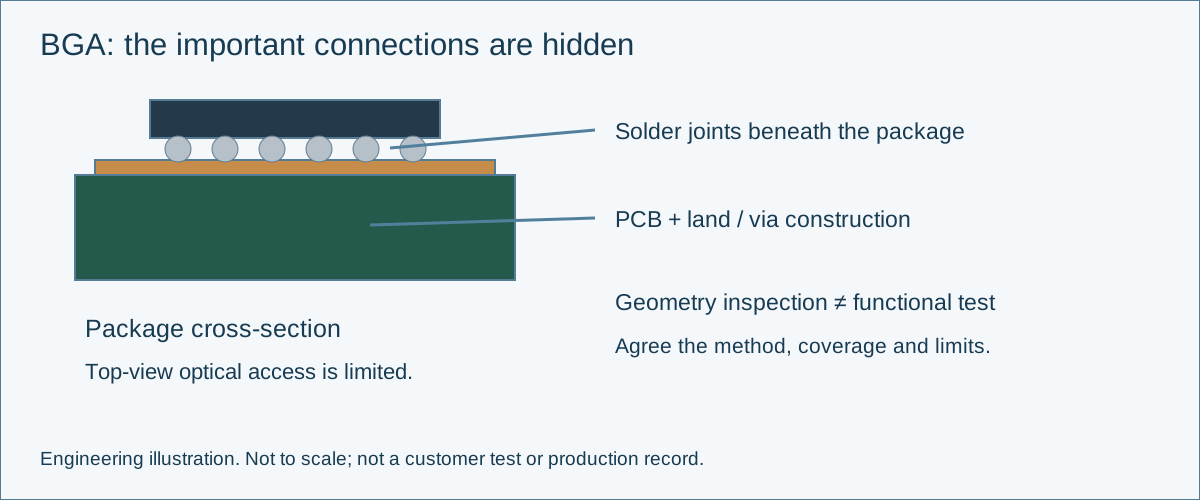
Hidden joints need a defined inspection strategy
Before placement: align package, footprint and board
Review HDI fabrication choices for dense BGA escape routing.
Identify the exact device and package drawing. Review the land pattern, solder-mask definition, via treatment, board support and the stencil strategy. For fine-pitch escape routing, fabrication choices must be resolved before they become assembly questions. Stacked packages add another solder interface: use the PoP package-pair, height and inspection review when the design uses package on package.
| Device identity | Manufacturer part number and package-specific attachment guidance |
|---|---|
| Board construction | Pad / mask geometry, via-in-pad treatment and local copper / thermal behavior |
| Moisture handling | Follow the package label and applicable handling procedure; do not assume every part needs baking |
| Stencil preparation | Assess aperture geometry and paste process together; a ratio is not a release guarantee |
From paste printing to a controlled release
Print paste, verify the deposit using the agreed inspection method, place the device and reflow with a profile developed for the actual assembly. A universal temperature curve cannot account for all components, board mass and solder materials. Inspection and any rework disposition should remain linked to the build record.
| Paste / placement | Check the deposit and placement against the established process |
|---|---|
| Reflow | Respect device and board limits with an appropriate measured process |
| Inspection | Review hidden-joint evidence and follow up on ambiguous indications |
| Electrical / functional test | Use the defined test plan; an X-ray image does not prove circuit function |
Compare stencil aperture geometry
Optional planning aid. You can request a file-based quote directly without completing this tool.
RAYPCB ENGINEERING
Assembly PlanningCompare stencil aperture geometry
Loading Compare stencil aperture geometry…
The planner needs JavaScript. The process tables on this page remain available. Send the listed parameters through Contact for engineering review.
What X-ray can—and cannot—tell you
X-ray can support assessment of hidden-joint geometry and indications such as bridging or voiding. Detection depends on the equipment, viewing method and joint geometry. An apparently acceptable two-dimensional image is not proof that every joint is electrically or mechanically sound.
| Optical inspection | Visible placement, polarity and accessible assembly features |
|---|---|
| X-ray inspection | Hidden-joint geometry within the capability of the inspection method |
| Electrical / functional test | Specified circuit behavior; coverage depends on access and the test design |
| Additional analysis | Required where an unresolved indication or failure needs deeper investigation |
A useful geometry example
A circular aperture of 0.30 mm diameter in a 0.10 mm stencil has an area ratio of 0.75: opening area divided by aperture-wall area. This arithmetic example is not a stencil recommendation for a particular BGA. Paste, wall finish, separation behavior and package guidance still matter.
| Circular aperture | Area ratio = diameter / (4 × stencil thickness) |
|---|---|
| Rectangular aperture | Area ratio = length × width / [2 × thickness × (length + width)] |
| Rework scope | Replacing a device requires its own thermal and inspection plan; it is not part of every assembly quote |
Prepare a reviewable enquiry
Send the current revision, quantity and the requirements that matter to your build. If something is preliminary, identify it. Exact price, schedule and acceptance scope are confirmed through the project review.
Download the editable CSV worksheet · Opens in Excel or another spreadsheet editor. No sign-in required.
Review quality and supplier-evidence requirements; check the assembly capability review. Equipment photographs illustrate the process; they do not replace a job-specific acceptance record.
Get a quoteCommon questions
Is this BGA chip manufacturing?
No. It covers mounting packaged BGA components onto printed circuit boards. Semiconductor packaging is a different manufacturing activity.
Can AOI inspect every BGA solder joint?
Conventional top-view optical inspection cannot directly see all joints underneath the package. Agree the appropriate hidden-joint and electrical test coverage.
Does a good X-ray prove a reliable BGA assembly?
No single image establishes lifetime reliability or complete electrical function. Interpret inspection results alongside the process, acceptance criteria and test plan.
Can the calculator choose my stencil thickness?
It compares aperture geometry only. Choose a stencil strategy using the package guidance and a qualified assembly process.
Continue with the part of the build you need
PCB Assembly service overview · Discuss your files with RAYPCB
Technical reference: IPC explains assembly process and acceptance standards. Specify the applicable revision and class for the order; this reference is not a certification claim. Texas Instruments: Flip Chip BGA Package Reference Guide provides package-related background; use the current guidance for your exact component.

