
RAYPCB · Route selection · engineering comparison
Blind vias vs buried vias: choose by the connection
Compare physical access, routing, fabrication sequence and verification. Classify a layer span and identify what to ask before choosing a via route.
Preliminary files and open process questions are welcome.
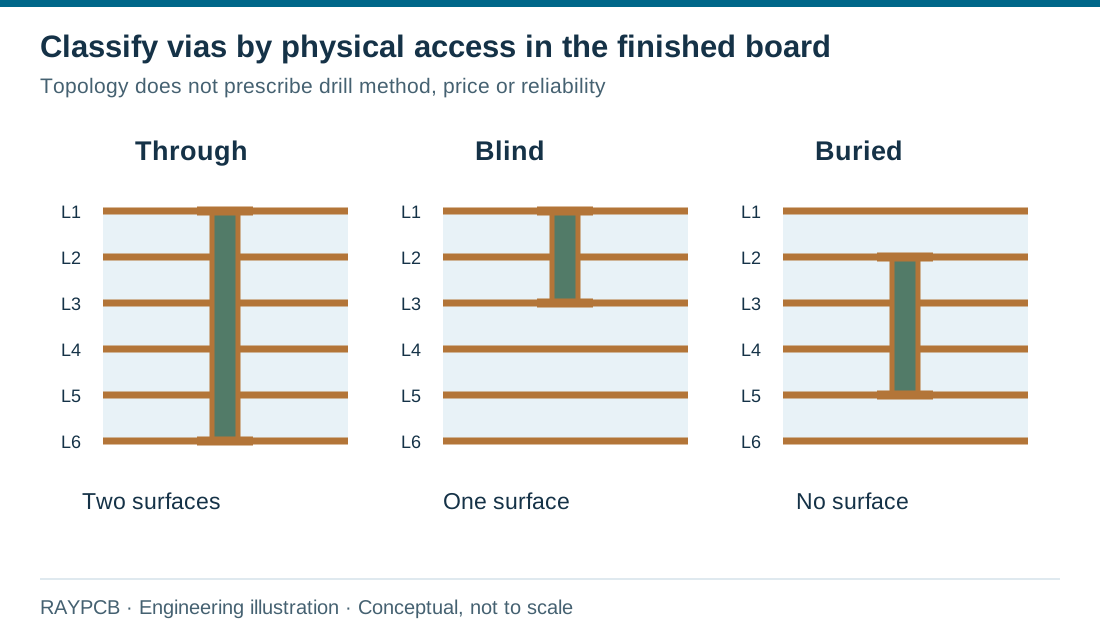
Blind vias and buried vias differ in physical access
A blind via reaches an internal layer from one finished board surface. A buried via connects internal layers without opening on either finished surface. A through via reaches both surfaces. These terms describe physical extent and access; they do not, by themselves, select a drilling method, set the cost or establish reliability.
Choose between constructions by the connection you need and the manufacturing sequence that can produce it. A dense surface escape, an internal routing bottleneck and an unused through-hole stub are different design problems. They may lead to different solutions even when the board has the same number of layers.
This page is a route-selection guide. Once the decision is clearer, use the dedicated blind-via construction page or buried-via subassembly page for dimensional planning and an enquiry brief. The objective is to make a useful manufacturing decision, not to choose the most elaborate structure available.
Compare the features that change the design task
| Question | Blind via | Buried via | Through-via baseline |
|---|---|---|---|
| Finished-surface access | One side | Neither side | Both sides |
| Physical endpoints | Surface and internal layer | Two internal layers | Opposite finished surfaces |
| Main planning task | Entry, target and accessible drilling route | Internal subassembly and enclosure sequence | Full-board hole and unused barrel review |
| Routing opportunity | Avoid occupying some deeper layers | Keep layers outside the internal span free | Simpler baseline if space and performance allow |
| Process question | How is the target reached and plated? | When is the internal pair formed and checked? | Does the conventional route meet requirements? |
| Inspection question | Which hidden features need evidence? | What must be verified before enclosure? | What board and interconnect evidence is required? |
| Cost comparison | Complete route, setup and verification | Complete subassembly sequence and verification | Complete baseline with any required extra work |
The table is deliberately not a ranking of “good, better, best.” A construction is useful when it meets the product’s electrical, mechanical and manufacturing requirements with an acceptable risk and cost. A simpler route can be the better engineering choice if the more complex route solves no demonstrated problem.
Classify a physical layer span
Enter the final layer count and the two physical endpoints. The classifier reports through, blind or buried based only on whether those endpoints reach the finished surfaces. It accepts either direction, rejects identical endpoints and does not infer a drilling technology or an electrical netlist.
RAYPCB ENGINEERING
Special Process EngineeringPhysical Via Span Classifier
Loading Physical Via Span Classifier…
An eight-layer board with physical endpoints L1 and L3 has a blind span. L3 and L6 form a buried span. L1 and L8 form a through span. These examples explain the naming rule; they do not approve those spans for a proposed stackup or assign them a price.
The distinction matters when a through via connects a signal to an internal trace. Its electrical connection can leave on L3 even though its barrel continues to L8. The physical structure remains through, and the unused portion may require separate review. Entering only the active electrical layers into a physical classifier would misdescribe that hole.
Separate the connection list from the hole extent
The netlist identifies intended electrical connections. The fabrication drawing identifies the actual physical barrel and its clearances. Both are needed. A through via can contact an internal signal layer, avoid other layers through antipads and continue beyond the active path. A topology label cannot tell you which intermediate copper features are connected or isolated.
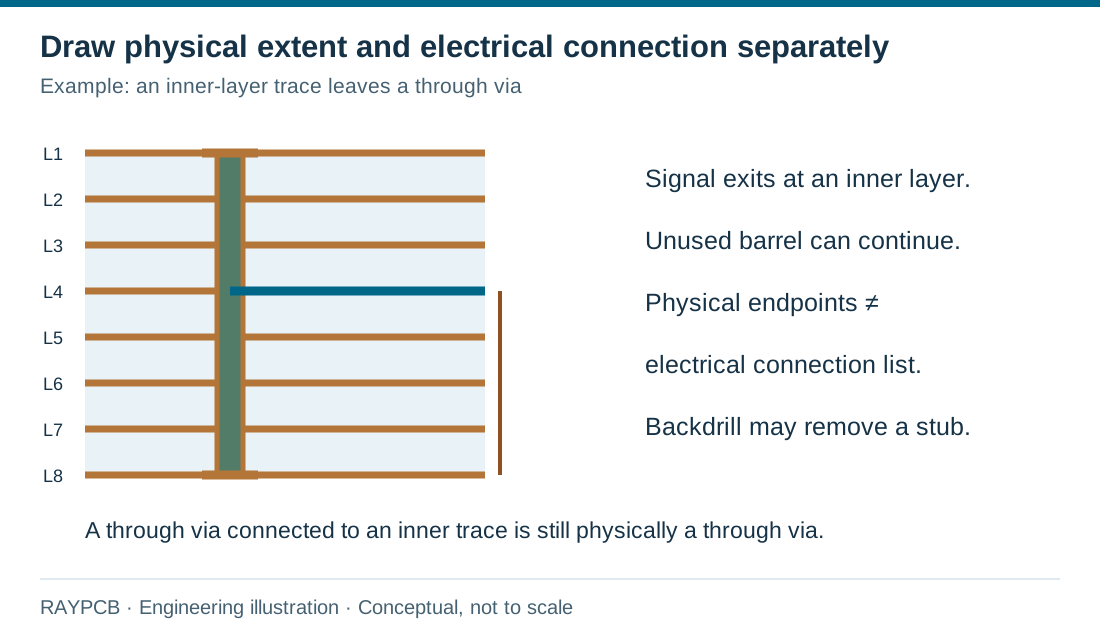
For a high-speed transition, review the barrel, lands, antipads, references and return path as a structure. A shorter physical span can reduce some unused geometry, but it does not automatically guarantee a particular impedance or loss result. The complete channel includes traces, connectors, packages and other transitions.
If the dominant issue is an unused through-hole stub, compare PCB backdrilling with a different span or routing layer. Backdrilling removes a selected barrel portion with depth and radial constraints. It is not simply another name for a buried via, and it needs its own manufacturing definition.
Start with the constraint you can demonstrate
Consider a fine-pitch device that cannot escape with the current through-via geometry. The next step is to compare land patterns, trace/space, routing layers and surface-to-inner connections. A blind construction may open useful channels, but the process and landing geometry must be reviewed. Changing the package fanout or stackup may also solve the problem.
Consider a congested internal routing region with little reason for the connection to occupy outer layers. A buried pair may release space outside its span. Before selecting it, show that the required subassembly and other drill pairs form a coherent build. The benefit is local routing freedom, while the cost and verification apply to the complete board.
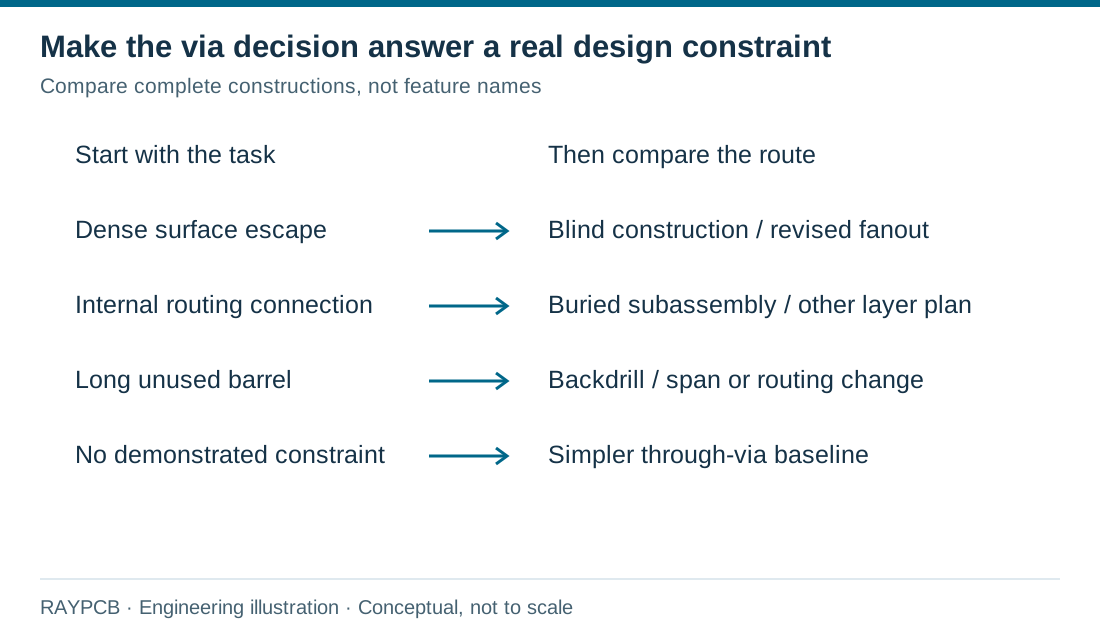
Consider a board that already routes and meets its electrical requirements with through vias. Adding blind or buried structures for appearance or perceived sophistication can introduce unnecessary constraints. Keep a documented baseline so that the proposed change has a measurable purpose: space recovered, a channel problem addressed, a board dimension reduced or another concrete benefit.
The comparison should make design effort visible too. A small fabrication saving can be outweighed by extensive rerouting, a new qualification campaign or a difficult late change. Conversely, a process increment can be justified if it produces a better total product outcome. Record the decision basis rather than treating the initial board quote as the only metric.
Read the stackup as a manufacturing plan
Blind and buried structures depend on access at the relevant manufacturing stage. Ask when each pair is drilled, prepared, plated and treated, and when later layers enclose it. A final list of copper layers is not a complete sequence. The HDI stackup and lamination guide helps organize this information.
CAD software can represent layer spans and drill types, but representation is not process qualification. Altium’s via-definition documentation provides a useful example of how design data describes these spans. Confirm the proposed route with the fabricator and check that exported files preserve the intended definitions.
Review all structures together. A board may combine through holes, blind features, buried pairs and via-in-pad locations. A change that looks small in one footprint may alter the build sequence or treatment requirements elsewhere. Keep the layer names, material definitions, drill map and fabrication notes synchronized as the design evolves.
Microvia and via-in-pad answer different questions
Blind and buried describe finished-board access. Microvia describes a defined construction category under the applicable technical requirements. Via-in-pad describes the placement of a via within a component land. Stacked and staggered describe the arrangement of successive connections. These terms can apply together, but none should silently stand in for the others.
For example, saying “BGA via in pad” does not tell the fabricator whether the hole is a through structure or a blind structure, nor does it fully specify filling and capping. Use the BGA via-in-pad design guide for that package interface. Saying “buried” likewise does not establish whether a particular treatment or internal buildup has been qualified.
Keep the vocabulary tied to the drawing. Ask for the physical span, drilling method, dimensional convention, treatment and finished condition. This avoids discussions in which design, purchasing and manufacturing all use the same short term while imagining different structures.
Compare evidence, not a technology ranking
There is no universal rule that buried vias are more reliable than blind vias, or that a visible opening is inherently a weakness. Materials, interfaces, geometry, processing and service conditions determine the relevant risks. Qualification evidence should represent the actual construction and the product’s requirements.
For microvia-containing routes, IPC’s published reliability warning reinforces the need for careful evaluation of hidden structures. It does not provide a one-line ranking that can replace engineering review. Use the HDI microvia review to organize the questions and evidence.
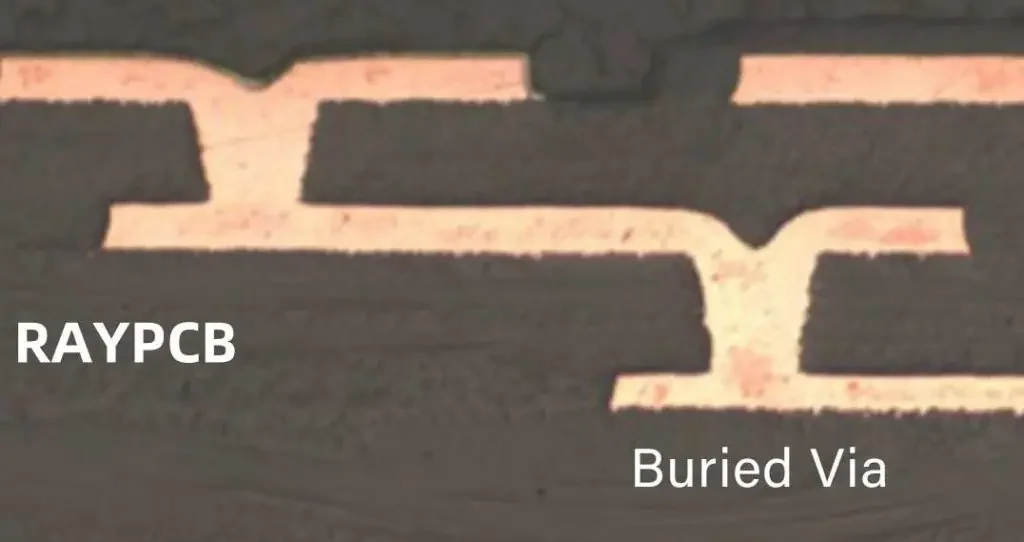
Decide what each test establishes. Final continuity checks intended electrical connectivity at the time of test. A section shows selected internal geometry. A stress or reliability test evaluates a specified exposure and measurement. None should be casually described as proof of every aspect of quality. Keep the scope and construction identity with the result.
Compare alternatives on the same commercial basis
Cost depends on the full route: materials, board dimensions, layer structure, drilling operations, filling, lamination, registration, panel utilization and verification. Fixed percentages for “blind” or “buried” can conceal these differences. A lower layer count can still cost more if it introduces a demanding process sequence.
Prepare two controlled alternatives when a decision is open. Keep quantity, acceptable-board definition, finish, inspection and delivery scope consistent, then identify the structural changes. Separate setup and qualification from recurring fabrication. Ask what is excluded so that a price for an unverified prototype is not compared with a production-ready, fully documented build.
| Compare this | Keep constant where possible | Explain any change |
|---|---|---|
| Bare-board scope | Quantity, outline, finish and acceptable delivery | Material or stackup alternative |
| Engineering effort | Same release maturity | Rerouting or development work |
| Verification | Product requirements and required evidence | New coupons, sections or qualification |
| Assembly interface | Package and final land requirements | Changed pad, fill or cap condition |
| Repeat production | Agreed revision and evidence | Approved substitutions or process changes |
Use the process-specific budget briefs on the blind-via and buried-via pages once an alternative is defined. They accept sourced allowances and can produce a technical request with costs blank. This comparison page avoids a generic price calculator because topology alone cannot supply a credible rate.
Write a short decision record before committing
Record the original constraint, baseline construction, alternatives considered, required evidence and the selected route. Include the reason alternatives were rejected. This record helps a later engineer distinguish a deliberate manufacturing requirement from a historical choice that may no longer be necessary after a redesign.
Ask the fabricator which dimensions and sequence details are still open. Approve any proposed change against both the electrical design and assembly interface. Keep the final stackup, drill map and fabrication notes together, and verify exported outputs rather than relying only on a CAD screenshot.
The HDI PCB page provides the closest manufacturing route for these structures. The broader PCB manufacturing overview covers the complete board service. A focused enquiry includes the design problem and the alternatives you can accept, allowing the discussion to move beyond a list of via names.
Questions that clarify the choice
Can one PCB contain through, blind and buried vias?
Yes, a design can combine them, subject to a reviewed construction. Every physical span and treatment must fit the agreed manufacturing sequence. Combining labels in a CAD file is not sufficient evidence of feasibility.
Is a via connected to an inner trace automatically blind?
No. The barrel may continue through to the opposite surface. Classify the physical extent separately from the electrical connection, then review any unused span and the complete signal path.
Should I choose the smallest possible via everywhere?
No. Select geometry that meets the local routing or electrical task within a qualified process. Unnecessary feature reduction can increase manufacturing and verification demands without producing a useful product benefit.
Which route should I send for quotation first?
Send the simplest credible baseline and identify the constraint it cannot meet, if any. Include a controlled alternative when available. A manufacturer can give a more useful comparison when the task, stackup and acceptance scope are explicit.
Discuss your via strategy
Send the fabrication revision, stackup, quantity and the specific process question. Include connector or package requirements, mechanical drawings and the inspection evidence you need.
Tool use is optional. Attach any downloaded brief manually; Contact does not automatically receive worksheet inputs. References reviewed September 2026. Illustrations are explanatory, and photographs are not process qualification records.