Preliminary files and open process questions are welcome.
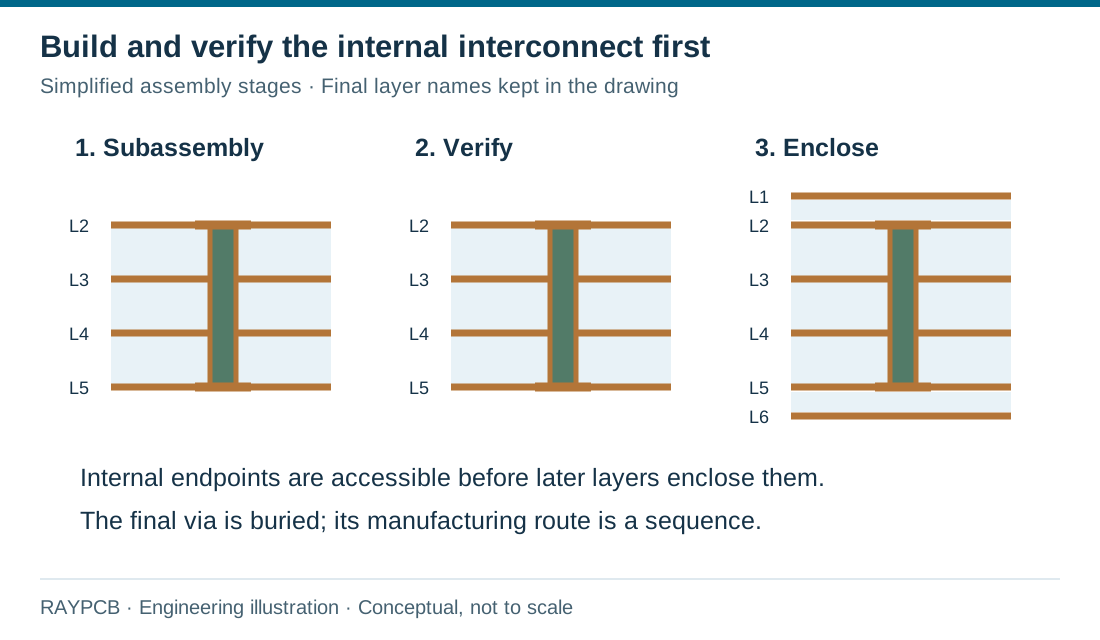
A buried via is formed while its subassembly is accessible. Additional layers later enclose it; the number of shown layers does not specify lamination cycles.
What is a buried via in a PCB?
A buried via connects internal layers and does not open on either finished PCB surface. It is formed while an internal subassembly is accessible, then enclosed by later layers. The key manufacturing question is therefore not only where the connection sits, but when it is drilled, plated, treated and verified during the build.
Buried vias can reserve routing space on layers outside their physical span. They also introduce a construction and verification sequence that must be agreed before release. A final board drawing with two internal endpoints is incomplete if it does not explain a feasible route for producing them.
This page focuses on internal subassembly planning. For a surface-to-inner connection, use blind vias. For a comparison before choosing a structure, use the blind-versus-buried via guide. The HDI PCB hub connects these decisions to the complete board construction.
Follow the connection through the build
The explanation below shows a simplified internal connection moving through four stages. It starts paused and can be stepped manually. It is an engineering illustration, not a factory recording or a claim that every buried-via board follows an identical process. Filling, intermediate processing and additional layer builds depend on the actual construction.
RAYPCB ENGINEERING
Buried Via Build Explorer
Special Process Engineering
Loading Buried Via Build Explorer…
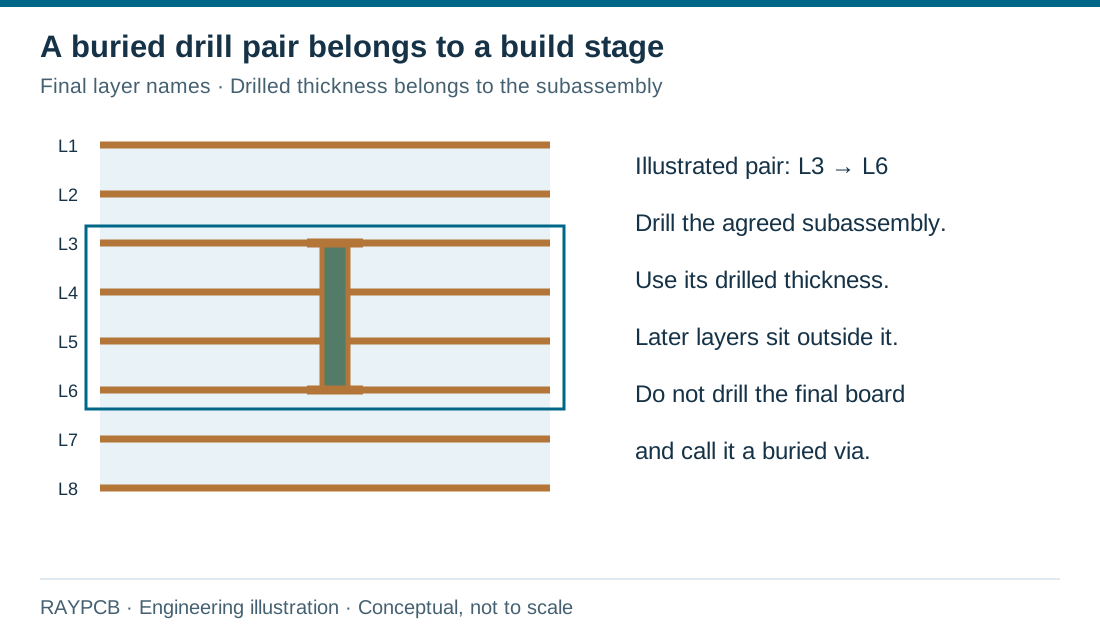
Name layers using the final electrical stackup throughout the discussion. A subassembly may temporarily expose layers that will later become internal. Without stable layer names, a drawing can confuse a manufacturing face with the finished top or bottom surface. Keep the drill pair, subassembly identity and final layer mapping in the same record.
01 / BUILD STAGE
Identify the internal structure before drilling
Select the internal layers that must be joined and define the laminate structure between them. The drilled thickness belongs to that subassembly, not necessarily to the finished board. Include the copper and dielectric details used for manufacturing and the tolerances relevant to the drilling and plating route.
Internal endpoints and the subassembly drilling thickness are separate inputs. A final stackup must show how each internal pair is manufactured.
For a finished eight-layer board, a proposed L3-to-L6 pair encloses four named copper layers, with two finished layers outside the span on each side. Those counts describe the geometry. They do not tell you how many lamination cycles are required or whether other requested pairs can be built in the same sequence.
The HDI stackup and lamination guide helps organize the full build. Review all drill pairs together, including any through holes and later blind structures. A individually plausible internal connection can still conflict with the proposed overall sequence when several structures share the same board.
Check the internal pair and subassembly ratio
The worksheet requires two different internal endpoints in their final layer order. It reports the layers included in the span, the finished layers outside it and the ratio of the entered maximum drilled subassembly thickness to minimum drill diameter. It rejects a pair that reaches a finished surface because that is not a buried span in this model.
RAYPCB ENGINEERING
Buried Via Subassembly Worksheet
Special Process Engineering
Loading Buried Via Subassembly Worksheet…
The illustrative L3-to-L6 example uses a 0.8 mm drilled subassembly thickness and a 0.25 mm drill diameter, producing a ratio of 3.2. This is arithmetic, not a capability statement. The fabricator must review the actual material, geometry, preparation, plating and acceptance requirements. The tool does not derive physical thickness from the number of copper layers.
Use the ratio to make the question precise: what construction and drilled dimension does the proposed process use? Do not use it as a universal acceptance threshold. If the manufacturing team proposes a different subassembly, update the worksheet basis and the drawing together rather than keeping a result from the previous sequence.
02 / BUILD STAGE
Drill and metallize while the pair is accessible
The internal subassembly must provide access for the intended operation. Review drilling, hole preparation, metallization and the specified copper connection with the actual construction. The target geometry and registration requirements need to survive the relevant processing, and unrelated conductors must retain their required isolation.
If the route needs filling or other treatment before further buildup, define that requirement explicitly. Different fill and protection methods serve different tasks. A statement that a via is buried does not by itself specify a fill material, a copper-filled structure or the required surface condition before lamination.
Use the IPC-4761 public guide extract to clarify treatment terminology, then agree the actual drawing requirements and applicable standard revision. The public extract is not a substitute for the full acceptance document. Numerical limits should come from the contracted specification and qualified process, not an invented generic rule.
03 / BUILD STAGE
Laminate without losing the construction history
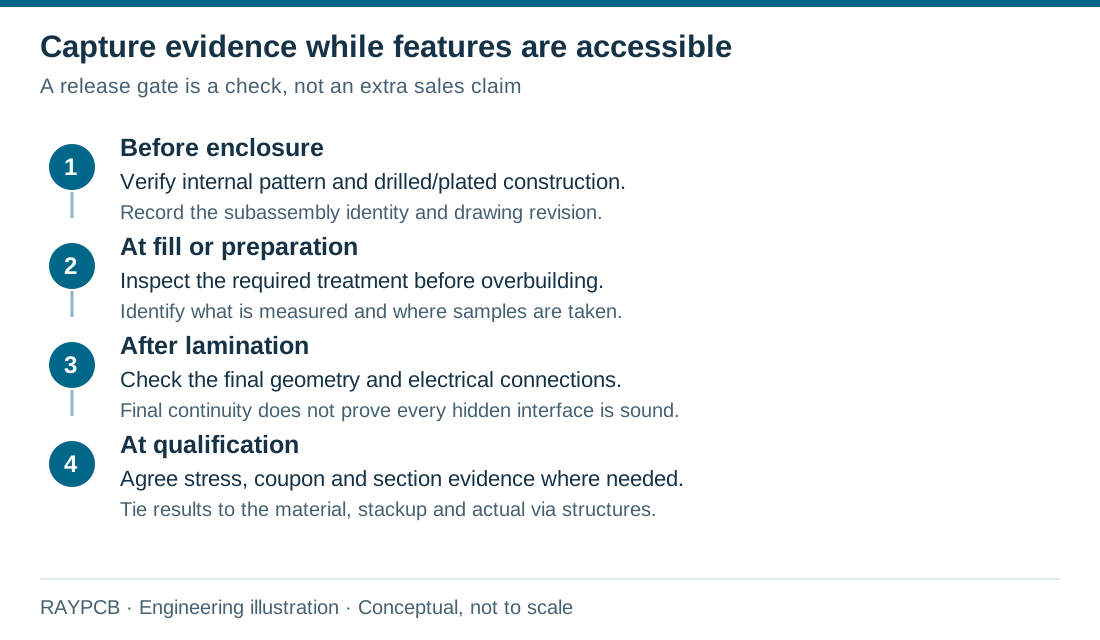
Before enclosing the subassembly, verify the features that are easier to assess while accessible. Record the layer pair, drilling operation, treatment and revision so that later inspection can be traced to the internal structure. Once the remaining layers are added, the outside of the board no longer shows where the buried connection begins and ends.
Additional lamination exposes the existing internal structure to another manufacturing stage. Review material compatibility, copper distribution, registration and any required preparation of the subassembly. A change to the sequence can affect more than the named buried via, including neighboring structures and the electrical stackup.
Existing RAYPCB HDI product image. Stackup, drilling sequence and internal connections are specified separately.
Continue with the agreed external features and final board processing after enclosure. Through holes or surface connections added later should not be confused with the earlier internal drill pair. Keep the final manufacturing package explicit about which files and inspection records belong to each operation.
04 / BUILD STAGE
Plan evidence around access and risk
Final connectivity is important, but it does not independently establish every hidden interface’s condition or long-term behavior. Define the appropriate in-process checks and final evidence before production. When a section or coupon is used, identify the structure it represents and the reason it is relevant to the product.
Buried-via verification is planned around accessibility. Product qualification uses the agreed construction and acceptance documents.
The IPC standards directory helps identify the applicable design, performance and acceptance documents. The order should name the agreed document revisions, class where applicable and special drawing requirements. Avoid a general “IPC compliant” label that leaves the actual buried construction and evidence undefined.
Where the design includes microvia interfaces, consult the HDI microvia review rather than assuming all internal connections have the same reliability considerations. Qualification should represent the actual material and via sequence. Evidence from a different stackup can be useful background, but it is not automatically proof for the new one.
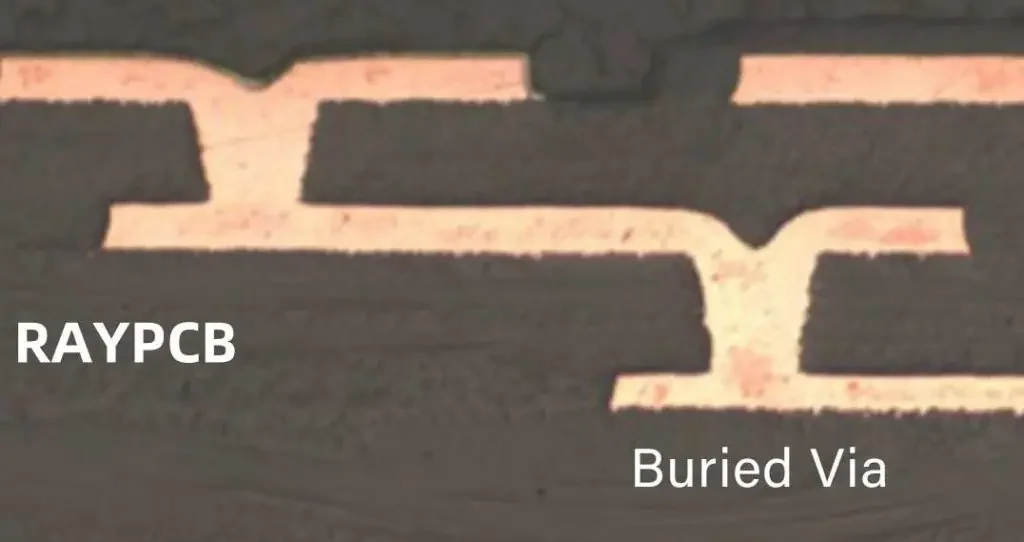
Existing illustrative section image from RAYPCB’s buried-via page. No lot, scale or acceptance record is supplied; it is not qualification evidence.
The section image illustrates why internal connections need a different view from an external product photograph. It is not supplied as a lot-specific acceptance record. For a real order, agree how images, measurements and electrical results will be identified and reviewed so that evidence supports an actual decision.
Evaluate routing benefit against the full construction
An internal-only connection can leave outer layers available for other routing or placement tasks. That benefit is valuable when it resolves a demonstrated congestion problem. Count the space actually recovered and consider whether a revised layer assignment or another routing approach can meet the same objective with a simpler process.
Avoid treating buried vias as an automatic signal-integrity upgrade. The electrical result depends on the pads, antipads, barrel, reference transitions and complete channel. A short-looking internal connection still needs an appropriate return path. Conversely, a well-designed through-via route may already satisfy the application without the added internal build complexity.
For power and thermal uses, define the real conductive geometry and material properties. Do not assign a solid-metal cross-section to a plated hollow barrel or assume that internal placement alone improves heat removal. The question should be tied to current distribution or heat flow in the actual product rather than to the attractiveness of the via label.
Design reason
Useful comparison
Evidence to retain
Internal routing congestion
Buried pair versus changed routing layers
Completed escape or routing study
Surface space constraint
Internal connection versus external fanout
Placement and available-area review
Channel transition
Candidate via geometries and reference paths
Electrical model and verification plan
Process simplification
Combined versus separate subassemblies
Fabricator-reviewed build sequence
What drives buried-via manufacturing cost?
The relevant scope can include internal drilling, metallization, filling, subassembly handling, lamination, registration and verification. Cost depends on the number and arrangement of drill pairs, not just the count of vias. Several connections that share one planned subassembly can differ substantially from a set that requires additional build stages.
Compare complete construction alternatives. A design with fewer finished layers is not necessarily cheaper if its process sequence becomes more demanding. Ask how a proposed change affects setup, recurring fabrication, inspection and delivery planning. Avoid fixed percentage rules that ignore the actual material and route.
RAYPCB ENGINEERING
Buried Vias Budget and RFQ Brief
Special Process Engineering
Loading Buried Vias Budget and RFQ Brief…
The budget brief uses dated allowances that you enter. It separates recurring board scope, setup and verification; it does not contain calibrated market rates. Leave costs blank for a technical enquiry. State whether the amounts cover the entire PCB or only the buried-via increment, and identify excluded assembly, freight and qualification work.
Make every drill pair traceable
Provide the final stackup, subassembly drawing, drill-pair list, hole and land dimensions, material requirements, treatment notes and acceptance plan. Include quantities and any alternatives the design team can accept. If a span or material is still open, mark it as an engineering question so that the quotation is not based on a false assumption.
Review the manufacturing outputs after export. Verify that the correct pair names, hole classifications and file revisions accompany the artwork. A screenshot of a CAD stackup is useful discussion material but does not replace controlled fabrication data. Keep agreed changes in the package that will be used for repeat production.
The broader PCB manufacturing overview explains the full service route. A productive buried-via enquiry adds the internal construction and the problem it solves, giving the manufacturing team enough information to review feasibility, cost and evidence without guessing at the intended sequence.
Buried-via questions before release
Can a buried via be drilled through the completed board?
A true buried connection has no opening on either finished surface. Its internal structure is formed while the relevant subassembly is accessible and then enclosed. A secondary operation on a finished through hole is a different construction and needs its own definition.
Does the number of layers outside the span equal lamination cycles?
No. Those are geometric layer counts. The actual build sequence depends on the materials and all requested interconnect structures. The worksheet deliberately reports no automatic lamination-cycle prediction.
Are buried vias always more reliable than blind vias?
No general ranking follows from the names. Reliability depends on the specific structure, process and service conditions. Compare qualified constructions and the evidence required for the product, not just which surfaces can see the hole.
Can ordinary final inspection verify the whole buried structure?
External inspection cannot directly view every internal interface. Agree the necessary in-process checks, sections, coupons, electrical tests and qualification evidence according to the actual requirement. Each method should have a clearly stated purpose.
Review your buried-via stackup
Send the fabrication revision, stackup, quantity and the specific process question. Include connector or package requirements, mechanical drawings and the inspection evidence you need.
Tool use is optional. Attach any downloaded brief manually; Contact does not automatically receive worksheet inputs. References reviewed September 2026. Illustrations are explanatory, and photographs are not process qualification records.