RAYPCB · ENGINEERING GUIDE
PCB Assembly Mistakes: Prevent Errors Before the Build
PCB assembly mistakes often begin before components reach the line. Conflicting revisions, unclear polarity, unsuitable footprints, missing test requirements and undocumented substitutions can create errors that inspection finds only after time and material have been consumed. A useful prevention review connects each risk to an owner and a verifiable release check.
This guide focuses on avoidable handoff and execution errors. It complements defect-specific investigation pages rather than diagnosing every failed board from a symptom list. The online brief identifies open release items for discussion.
Release one coherent data package
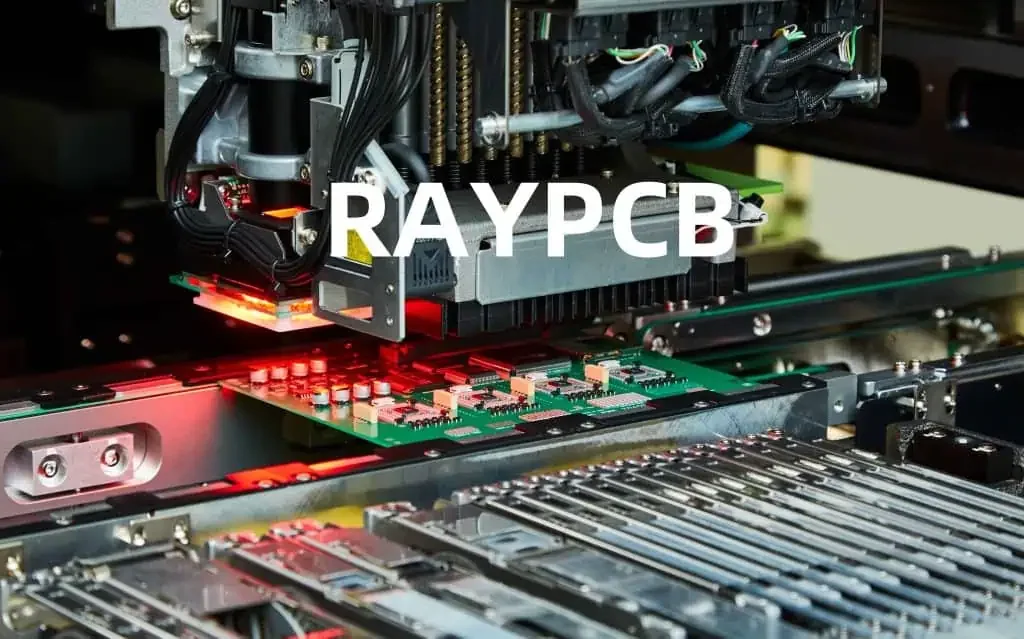
Confirm that BOM, placement data, fabrication files, assembly drawing and test information refer to the same revision. Record fitted and not-fitted options explicitly. A component listed in one file and omitted from another needs resolution before programming equipment.
Use the required assembly-files guide for the package structure. Keep superseded files out of the active release instead of relying on filenames such as final or latest.
Verify package, orientation and polarity
Match the exact component ordering code and package to the footprint and assembly instruction. Similar names or nominal values can conceal different dimensions, pinouts or polarity conventions. Placement rotation conventions must be interpreted consistently with the actual CAD data.
Mark ambiguous parts on the assembly drawing and resolve them before the first build. Silkscreen can help but should not be the only authority when it conflicts with the schematic, footprint or component documentation.
| Review item | What to establish |
|---|---|
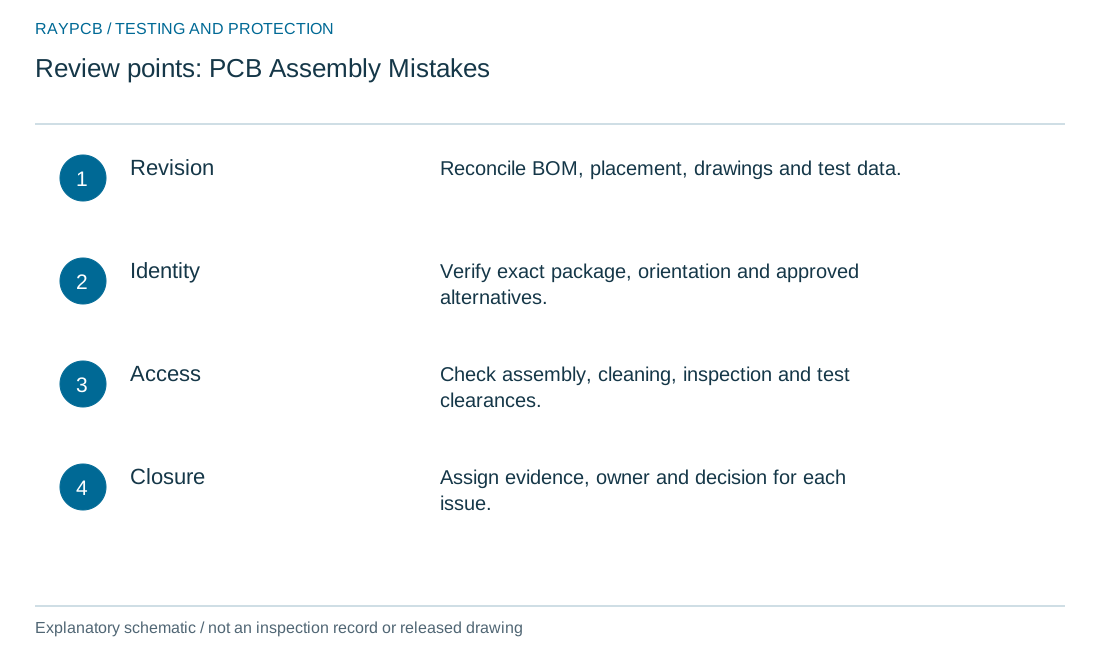
| Revision | Reconcile BOM, placement, drawings and test data. |
| Identity | Verify exact package, orientation and approved alternatives. |
| Access | Check assembly, cleaning, inspection and test clearances. |
| Closure | Assign evidence, owner and decision for each issue. |
Review physical access and process compatibility
Tall parts, close spacing, panel edges and underside components can affect printing, placement, soldering, cleaning and test access. A layout that passes electrical design-rule checks may still create assembly difficulties.
Use design for assembly for the wider layout review. Document approved compromises and the extra operations they require rather than assuming a special fixture or manual step is included automatically.
Control substitutions and material handling
Approved alternatives need defined identity and technical review. A replacement with the same nominal value can differ in package, thermal behavior or functional characteristics. Keep the decision linked to the BOM revision and production record.
Storage, moisture handling, solderability and ESD controls must follow the actual material and component requirements. Do not use one generic handling instruction for every part family or infer suitability from an unopened reel alone.
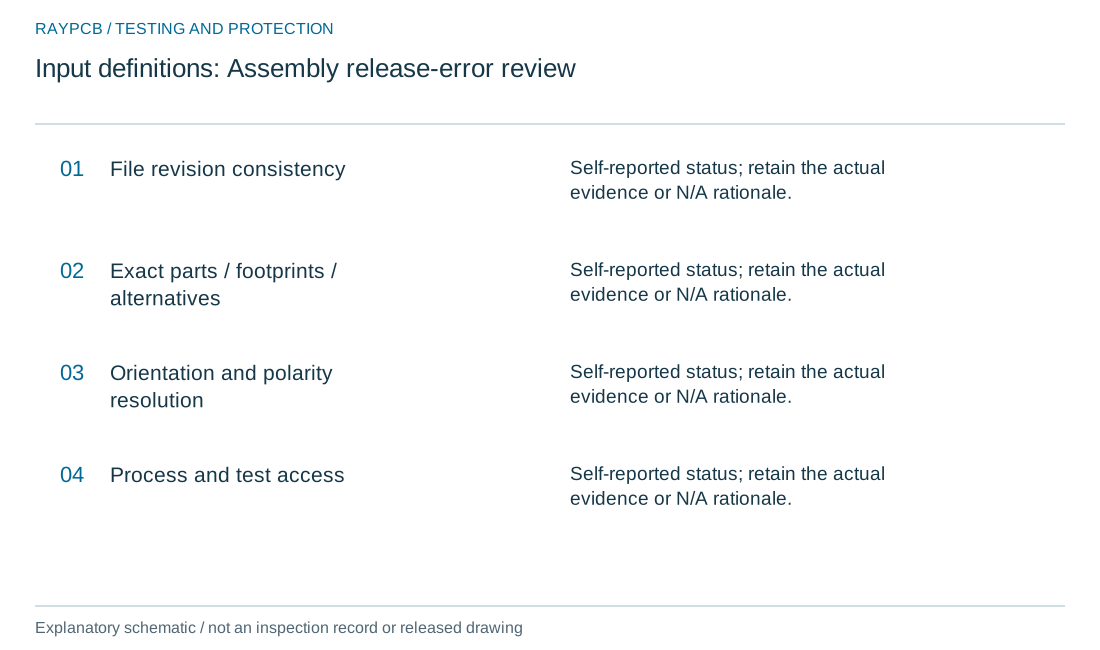
Assembly release-error review
Assembly release-error review
Use the current inputs and keep the assumptions
Choose the engineering question before entering numbers. Fields begin blank. Load example fills teaching values so you can understand the model; those values are not recommended dimensions, process settings or market prices. The example label remains visible after edits. Reset before preparing a record based entirely on your own project data.
Use the displayed units and keep a reference for each input. Counts must describe the same scope, and measurements must share the declared conditions. A threshold entered by you remains your supplied review condition. The website does not turn it into an IPC limit or an approved product requirement. If the necessary value is unknown, obtain the evidence rather than replacing it with an attractive assumption.
Read the result and its limitations together. An access fraction is not fault coverage, a cost allowance is not a quotation, and a completed evidence checklist is not a safety or quality approval. Negative margins remain visible where the model permits them. They identify a conflict in the entered scenario rather than silently adjusting the result.
Changing an input invalidates the result and disables its download until you run the tool again. The text record contains the inputs, result and limitations. Processing stays in your browser; no CAD files, instruments or certificates are read. No data is automatically transferred to the enquiry form. Download and attach the record manually if useful, or contact RAYPCB directly without completing the tool.
| Input | What to establish before using it |
|---|---|
| Review reference | Use a nonconfidential revision or scope reference. |
| File revision consistency | Self-reported status; retain the actual evidence or N/A rationale. |
| Exact parts / footprints / alternatives | Self-reported status; retain the actual evidence or N/A rationale. |
| Orientation and polarity resolution | Self-reported status; retain the actual evidence or N/A rationale. |
| Process and test access | Self-reported status; retain the actual evidence or N/A rationale. |
| First-article approval and closure | Self-reported status; retain the actual evidence or N/A rationale. |
| Next action / record reference | Use a nonconfidential reference; this tool does not verify the record. |
Make first-article review useful
Check the features most likely to reveal a release error: component identity, polarity, variant population, critical placement and the intended test behavior. Agree who can authorize continuation and how unresolved questions hold the affected scope.
The first article should validate the released setup, not become an undocumented opportunity to change production data. Record corrections in the controlled files so later units and repeat orders receive the same resolved instructions.
Example: a correct value with the wrong package
An illustrative purchase substitution preserves resistance but changes the package footprint. If procurement, layout and placement files are reviewed independently, the incompatibility can reach the line. The prevention is a joined identity-and-footprint check, not simply stronger final inspection.
When a mistake does occur, preserve the affected revision and identify how it escaped. Correct the system that allowed the mismatch rather than treating operator vigilance as the only control.
Convert findings into a clear build handoff
List each open issue with its location, evidence, responsible owner and required decision. Separate manufacturing questions from product-design decisions. Do not mark a concern closed because someone has acknowledged receiving it.
For the production route, continue to PCB assembly. When the issue has already produced failures, the failure-analysis guide provides the next evidence-preserving step. The checklist can support a direct enquiry but remains self-reported.
Questions to resolve before the next build
Can final inspection compensate for inconsistent release files? It may catch some consequences, but it cannot reliably infer which conflicting file expresses the design intent. Resolve revisions and options before the build. Final inspection should verify the released product, not force the operator to choose between contradictory BOM, placement and drawing information.
Should every finding trigger a full redesign? Distinguish a documentation correction, manufacturing adjustment, approved deviation and necessary design change. Assign the decision to the proper owner and verify the result at an appropriate scale. The important control is that the resolution reaches the released files and repeat-order process. An informal email that never updates the production package can leave the same mistake waiting for the next build.
Use findings to improve the controlled release
Make the investigation reproducible before making it broader. Record the exact symptom, product revision, conditions and observations already made. Identify which statements are measured, which are reported by the customer and which are hypotheses. This prevents an early guess from becoming the accepted explanation without supporting evidence.
Preserve the specimen's value. Cleaning, probing, powering, flexing, reheating and component removal can change the condition being investigated. Plan those actions under qualified procedures and document interventions. Where possible, retain an unaltered sample and a suitable comparison unit so that later methods still have meaningful evidence to examine.
Use the schematic and construction to interpret readings. Parallel paths, active devices, stored charge and the measurement interface can affect an observation. A familiar meter indication is not enough to identify a failed component. State the electrical path, instrument mode, reference and board state so another reviewer can understand the result.
Choose the next method to distinguish explanations. If two plausible mechanisms predict the same observation, repeating that observation may add little. Ask what evidence would separate them and whether obtaining it would destroy information needed for another method. This keeps the investigation purposeful rather than turning it into a checklist of every available laboratory technique.
Contain the operational problem while preserving technical uncertainty. Production may need a hold, additional screening or replacement material before the root cause is fully established. Record the basis and limits of that containment separately. A temporary action that restores operation does not automatically prove the cause or prevent recurrence.
Verify the remedy against the supported mechanism. A repaired board that passes one check may still require additional inspection or testing after the intervention. Update the relevant design, supplier requirement or process control when the cause is confirmed. Keep the original failure and repair history visible instead of replacing it with a final pass flag.
Prepare the enquiry around the decision needed. State whether the goal is identifying a defect, choosing a repair, evaluating a lot or preventing recurrence. Include the evidence already available and the sample constraints. RAYPCB can then review the manufacturing-related scope while specialist analysis, product safety decisions or unresolved design requirements remain clearly assigned.
Standards, source context and limits
Use each reference for its stated scope. Equipment and material documentation applies to the identified product and conditions. A published study describes its own specimens and methods; its settings are not universal production limits. Public standard summaries and revision tables do not replace the controlled normative document.
Agree the applicable standards, revisions, product class where relevant, measurement methods and exceptions before production. Distinguish printed-board requirements, assembly workmanship, laboratory competence and finished-product certification. A method name or photograph does not establish that a supplier holds an accreditation or that a particular test is included in an order.
Archive photographs illustrate relevant boards, equipment or operations from the existing RAYPCB website. They are not evidence of current equipment ownership or results from your project. Original diagrams explain concepts and measurement boundaries; they are not inspection records or released manufacturing drawings. Confirm the actual service and reporting scope in the project review.