RAYPCB · ENGINEERING GUIDE
Wireless Module PCB Assembly: Files, RF Checks and Release
Wireless module PCB assembly combines ordinary assembly controls with antenna, RF path, firmware and test requirements. A board can power up and communicate over a short bench distance while still having a weak antenna connection, an incorrect module variant or a configuration that differs from the intended product. The useful manufacturing question is therefore broader than whether the module was soldered onto the board.
This page helps engineers and purchasers prepare a repeatable wireless build. Use the handoff worksheet to record evidence, open items and responsibility. It does not inspect CAD files, qualify a radio or approve a product for a market. If you already have a complete release, go directly to the PCB assembly service or send the build requirements.
Identify the exact module and the build boundary
Begin with the complete manufacturer part number and hardware variant. Modules with similar names may use different antenna interfaces, integrated antennas, memory options or approved firmware configurations. A purchasing description such as Bluetooth module is insufficient when the footprint or antenna arrangement depends on a suffix. Keep the approved source and substitution policy in the BOM.
State whether the build includes only the carrier PCB, the antenna and cable, a programmed module, or a fully enclosed product. A bare carrier with a temporary test antenna is a different assembly from the finished product with a battery and housing. If final assembly happens elsewhere, identify which team owns the last RF verification and which parts of that test can be performed at board level.
Separate prototype flexibility from production interchangeability. An engineering sample can contain a deliberate alternate part or a hand-tuned matching value, but those exceptions need a record. Do not let a successful prototype become the only instruction for a repeat order. The released BOM, placement file, drawing and software package should describe the configuration that produced the accepted evidence.
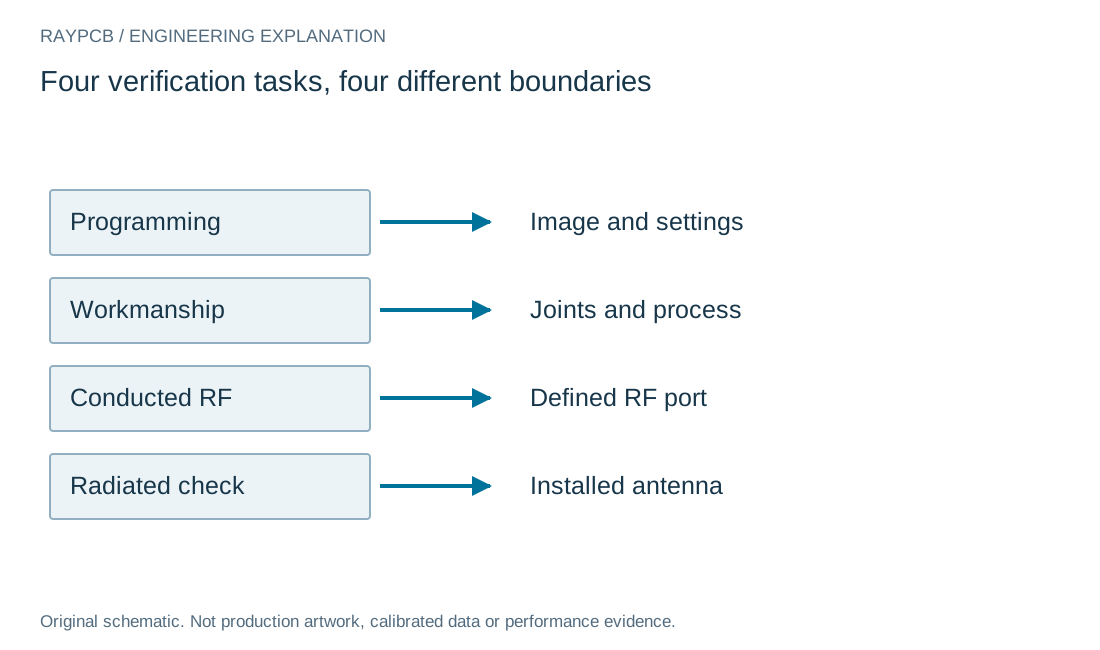
Wireless build verification map
| Task | Typical evidence to define | Boundary |
|---|---|---|
| Programming | Image identity, configuration and programming result | Does not establish antenna performance |
| Assembly inspection | Joint-access method and agreed criteria | Does not replace functional RF checks |
| Conducted RF | Port, settings, correction and acceptance method | May exclude installed antenna |
| Radiated check | Fixture or environment and assembled configuration | Scope depends on correlated test design |
Wireless assembly RF handoff record
Wireless assembly RF handoff record
Use the current inputs and keep the assumptions
Enter your own values or use Load example to explore the clearly labeled teaching inputs. The example is not a measured RAYPCB project. Clear for my inputs starts a separate record. Fields identify the units and the physical boundary; missing or unsupported values need correction before a result is generated.
Changing an input invalidates the previous output and disables its download until you generate a new result. A worksheet cannot inspect a board, validate an instrument setup or approve manufacture. Keep its assumptions with any copied number.
Download the current text result if it helps explain a design question. The file stays on your device. Attach or paste it manually when contacting the team; no project information is automatically transferred to the Contact form. Completing this tool is optional.
| Input | What to establish before using it |
|---|---|
| Review reference | Nonconfidential scope or revision. |
| Exact module, antenna variant and approved BOM | Choose the evidence state, not an approval. |
| Handling, paste, reflow, cleaning and rework limits | Choose the evidence state, not an approval. |
| Product firmware, test image and configuration | Choose the evidence state, not an approval. |
| Workmanship, conducted and radiated test scopes | Choose the evidence state, not an approval. |
| Fixture revision, serial records and open-item owners | Choose the evidence state, not an approval. |
| Next action / evidence reference | Nonconfidential reference only; no files are inspected. |
Optional cost comparison from your own allowances
Use a quotation or a clearly labeled internal assumption for each input. Keep the quantity, construction and inspection scope the same when comparing alternatives. This uncalibrated planning model adds entered values; it contains no current market rates and does not issue a RAYPCB quotation. You can contact the team without completing it.
Entered construction and verification budget
Prepare files that explain the RF details
Provide the board fabrication release, BOM, centroid or placement data, assembly drawing and relevant schematic pages. Include polarity and orientation details that are easy to misinterpret from a footprint alone. Identify the module pin-one convention, connector orientation and any components intentionally not populated. Keep revision identifiers consistent across the files.
For an external antenna, specify the connector and cable part numbers, mating direction, retention and routing. Show whether a cable may cross the antenna area or lie against a shield. If a through-hole antenna is fitted, include its finished height and mechanical orientation; the through-hole antenna guide explains why solderability and RF positioning are related but separate requirements.
For a matching network, distinguish fitted values, tuning placeholders and reserved alternatives. A component shown in the schematic may be omitted intentionally, but the assembly file must say so. Identify any tuning procedure that occurs after initial assembly and who authorizes its final values. A general note saying optimize RF does not define a repeatable production operation.
| Review item | What to establish |
|---|---|
| Identity | Full module part number, antenna variant, BOM alternatives and revision are controlled. |
| Assembly | Handling, paste, orientation, reflow and rework limits refer to the selected part. |
| Verification | Programming, workmanship, conducted RF and radiated checks have distinct scopes. |
| Release | Fixture revision, software, traceability and open-item owners are recorded. |
Treat the antenna area as controlled geometry
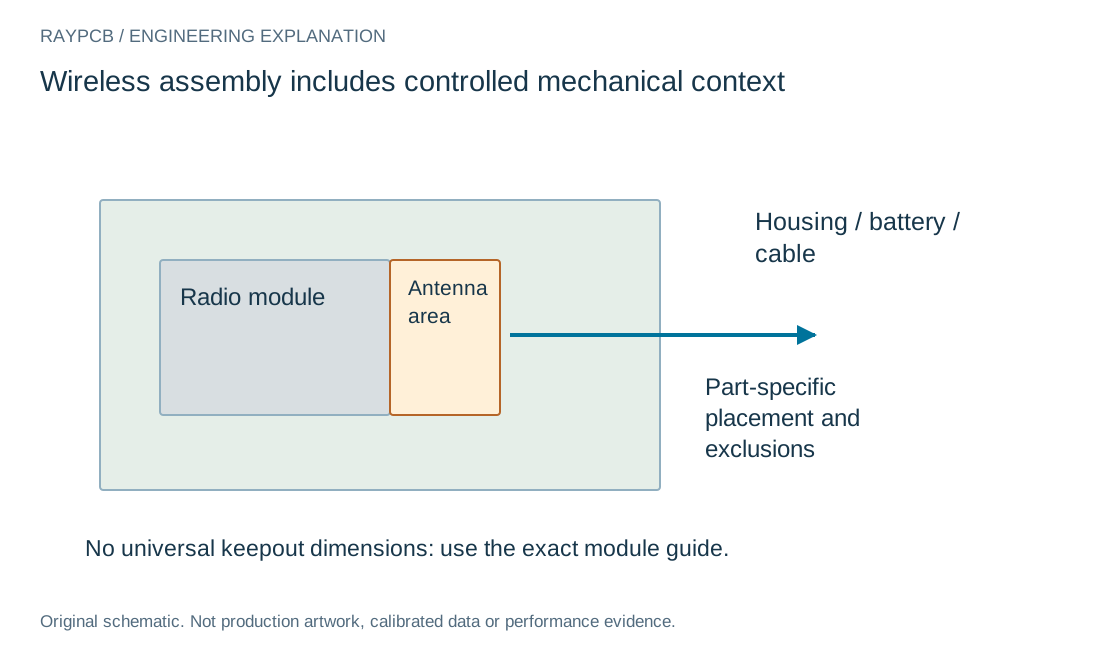
Read the integration guidance for the exact module and antenna variant. Some products require specific board-edge placement and restricted copper or component areas; others use a different ground arrangement. Do not apply a universal keepout rectangle across every module. Board size, layer construction and surrounding metal can all differ from the vendor evaluation setup.
Mark the antenna zone in the assembly and mechanical review. Screws, shields, display cables, battery tabs, adhesive, coating and enclosure walls may be introduced after the electrical layout is complete. A mounting feature that does not violate a conventional spacing rule can still alter the installed RF behavior. Include the final mechanical state in verification planning.
The Bluetooth antenna layout guide is useful for the antenna matching and packet-test task; the present page focuses on making the chosen construction repeatable. If the product uses cellular radio, confirm the specific technology and bands rather than substituting the word wireless for every requirement. The GSM integration guide keeps legacy network and antenna questions distinct from a generic assembly request.
Plan handling, paste, placement and reflow together
Use the module manufacturer's current handling and soldering information for the selected part. Moisture sensitivity, storage, baking restrictions, reflow exposure and cleaning compatibility can vary. A rule from another module family is not a safe substitute. Record how the material is received, stored and released to the line, including any relevant exposure history.
Review the land pattern and paste definition with the module geometry and assembly process. Large ground pads, castellated edges, bottom pads and shielded packages can require different inspection access. The paste stencil is part of the process definition; it should not be inferred solely from the copper opening. Identify the drawing or approved process record that controls it.
Measure or establish a suitable thermal profile on a representative assembly. The module, nearby connectors, shields and large copper areas affect the thermal context. Confirm limits for the actual parts and allowed process exposures before deciding the assembly sequence. If a second reflow or localized rework is proposed, evaluate it against those limits instead of assuming that every wireless module supports the same number of cycles.
Choose inspection methods for the joints you actually have
Visible solder joints can be assessed using appropriate optical access and agreed workmanship requirements. Hidden interfaces may require another inspection method or process evidence. Inspection planning starts with package construction and the faults of concern. It should not be a list of every available machine regardless of whether the method can reveal the relevant joint.
Distinguish assembly workmanship from RF performance. A visually acceptable joint does not prove a feed transition has the intended impedance, and an RF link does not prove all joints meet the agreed acceptance criteria. Keep both evidence streams in the traveler. When an inspection method has limited access beneath a shield or module, state that limitation and identify the complementary control.
Agree the applicable assembly standard, class, revision and any customer-specific requirements before release. This page does not reproduce IPC acceptance tables or claim that selecting a class in a tool certifies the product. The PCB assembly standards guide provides context for organizing that discussion with the manufacturing team.
Separate programming, conducted checks and radiated checks
A wireless production test can contain several distinct tasks. Programming confirms that the intended image and configuration were written. Electrical checks establish supply and interface behavior. Conducted RF checks examine a defined port where suitable access exists. Radiated checks include the installed antenna and its environment. None of these automatically replaces all the others.
Define test firmware, operating mode, channel settings, power configuration and the result to save. A generic association or pairing event may not exercise the worst operating condition or detect a marginal RF path. Conversely, a detailed characterization sequence can be too slow for routine production. Select the screen against demonstrated fault coverage and preserve the correlation with engineering characterization.
u-blox's NORA-W40 integration manual is one example of a vendor document that separates integration, soldering and product testing. Its instructions apply to the specified module family and revision, not to every radio. Obtain the equivalent current document for the exact part in your BOM and retain the relevant test configuration with the release.
Keep fixtures and software from becoming hidden variables
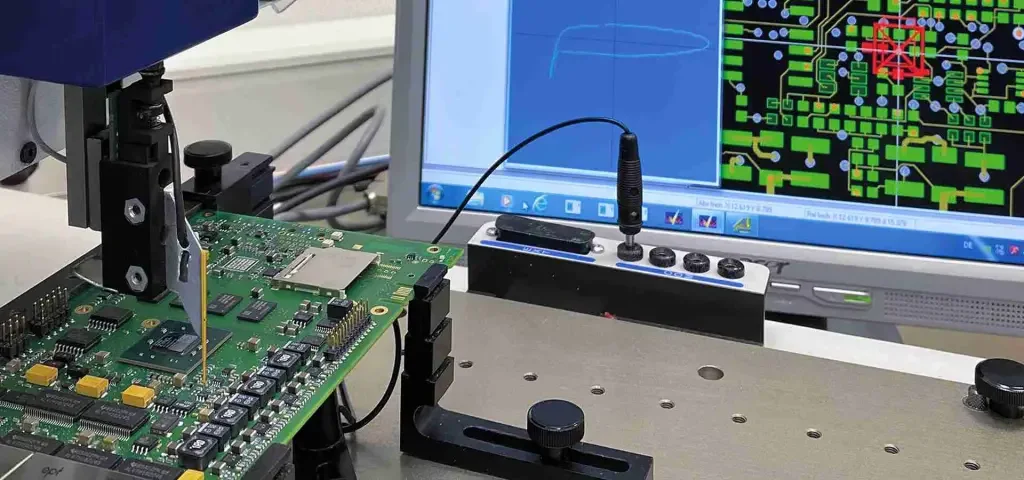
Define the fixture interface and how it contacts the board or RF path. Probe wear, connector cycles, cable routing, shielding and reference units can affect repeatability. Identify a verification routine for the fixture and the action when it fails that check. Otherwise a fixture problem can be recorded as a batch of bad boards or conceal a real process change.
Version the test software and configuration separately from the product firmware when appropriate. Record which combinations were approved. A change in driver, instrument command sequence or measurement bandwidth may change the result even if no copper or components changed. Keep enough information to reproduce a decision without retaining unnecessary customer design data in a general reporting system.
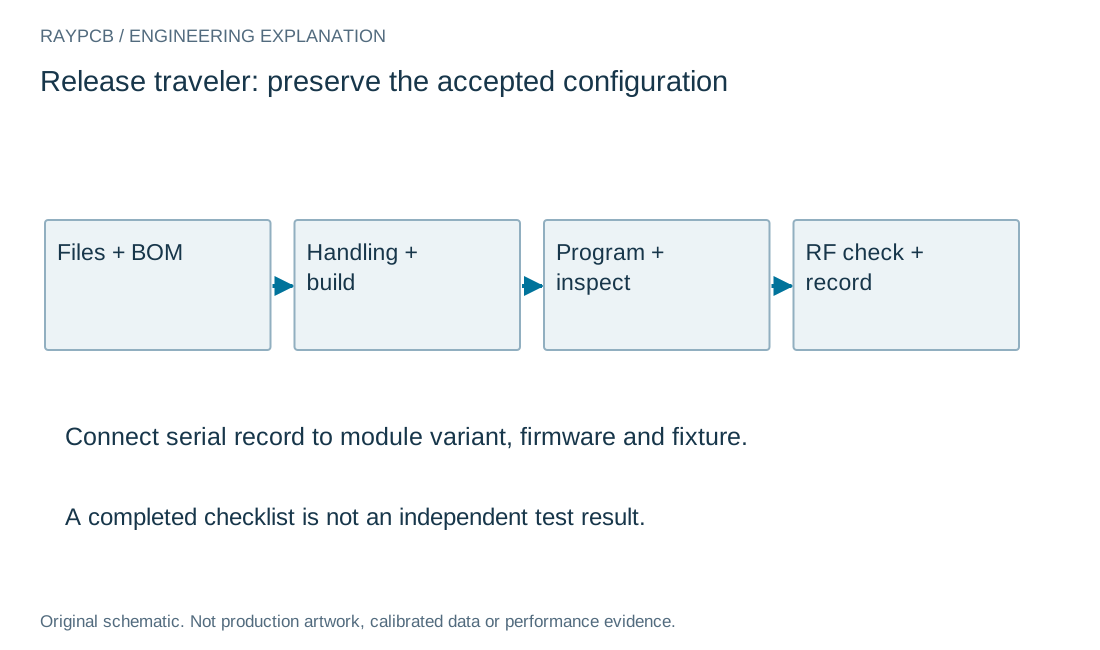
Serial-number traceability should connect the assembly revision, fitted module variant, programmed image and required test outcome. Decide the necessary retention and access arrangements with the customer. Do not assume that more data is always better; preserve the records that support the agreed quality and service tasks while avoiding secrets in public worksheets or analytics.
Estimate cost from the actual assembly and test scope
The optional budget worksheet sums your own unit and lot allowances. It contains no hidden market rates or automatic module prices. Separate recurring board or assembly cost from programming setup, fixtures, RF characterization and the selected production test. Comparing two suppliers is only meaningful when the quantity and included tasks match.
For example, a quote including antenna cable installation and a defined radiated screen cannot be fairly compared with a quote for soldering the module alone. Ask which fixtures are reusable, which records are delivered and what happens to units requiring tuning or rework. Avoid converting an uncharacterized yield assumption into a promised delivered unit price.
To request a build review, send the current files, complete BOM, quantity, intended enclosure state and required programming and test scope. List unresolved antenna, component or process decisions plainly. You do not need to finish the worksheet before contacting RAYPCB. Downloaded summaries stay on your device and must be attached manually if they help explain the request.
Make the repeat build match the accepted configuration
Keep the module variant, antenna and cable, board revision, fitted tuning values and programmed image together. A purchasing substitute or enclosure change may require a new RF review even when the assembly still powers up.
Separate open design questions from released production instructions. Identify who will resolve each remaining item and which verification establishes acceptance. A complete document checklist is useful for coordination, but it does not prove that the actual joints, programming or radio performance meet the requirement.
Standards, source context and limits
Use the current document for the exact selected component, construction and test method. A vendor application note is not a universal fabrication rule. Agree any applicable acceptance standard and edition for the project; these public references do not certify a board or reproduce licensed acceptance criteria.
Photographs are identified as existing site archive context. They do not establish current factory ownership, calibrated results or a customer's product performance. Original diagrams explain the named engineering boundary and are not production artwork or field-solver output.