
RAYPCB · ENGINEERING GUIDE
Electromechanical Assembly: Align the PCB, Harness and Enclosure
Electromechanical assembly brings electronic boards together with wiring, connectors, mounting hardware and mechanical parts. Successful integration requires more than a PCB outline that fits inside a nominal enclosure. The design must allow the parts to mate, preserve the intended electrical paths and remain accessible for assembly, testing and service.
This page is a tolerance and integration workbench. It complements the box-build assembly service with practical questions about datums, stack dimensions, harness routes and acceptance. The local fit calculator evaluates a signed, one-dimensional worst-case stack; it does not perform a three-dimensional interference check or approve a connector design.
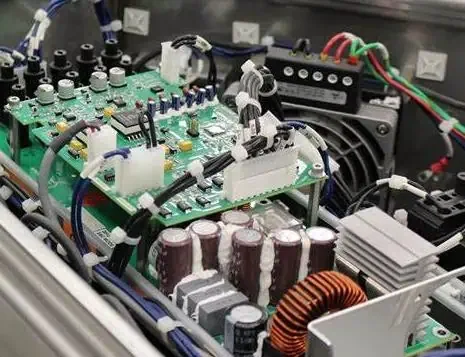
Start from common datums and the assembly sequence
Identify the mechanical references used by the PCB, enclosure, bracket and mating connector. A dimension measured from the board edge cannot be combined blindly with another measured from a housing centerline. Put the references on the controlled drawings and establish how the assembly is located before fastening.
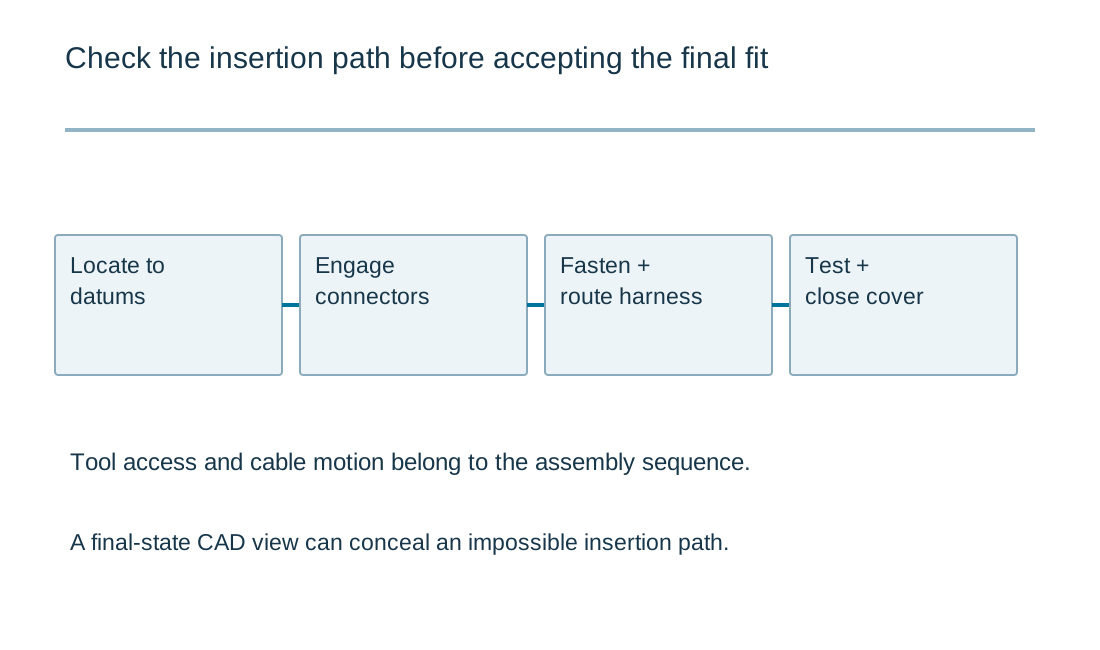
Walk through the installation sequence. Check whether a connector must be engaged before the board is secured, whether a tool can reach each fastener and whether a harness can be routed without forcing the board. A final-state CAD image may conceal an impossible insertion path or an inaccessible test point.
Define the delivered configuration through the electronic module assembly guide. It matters whether the supplier installs the enclosure, supplies an open subassembly or only prepares the PCBA. The responsible team must own the fit at each handoff rather than assuming another party will adjust the parts during production.
Dimensional evidence before integration
| Question | Controlled input | Worksheet limitation |
|---|---|---|
| Does the stack fit? | Common datum and signed nominal dimensions | One-dimensional symmetric worst-case bounds |
| Can the connector mate? | Exact drawings and engagement conditions | No 3D insertion or angularity model |
| Can the assembly be serviced? | Harness route and tool access | No motion or strain simulation |
| Does heat transfer as intended? | Actual interfaces and installed conditions | A gap result is not a thermal model |
Use a signed stack to expose the dimensional question
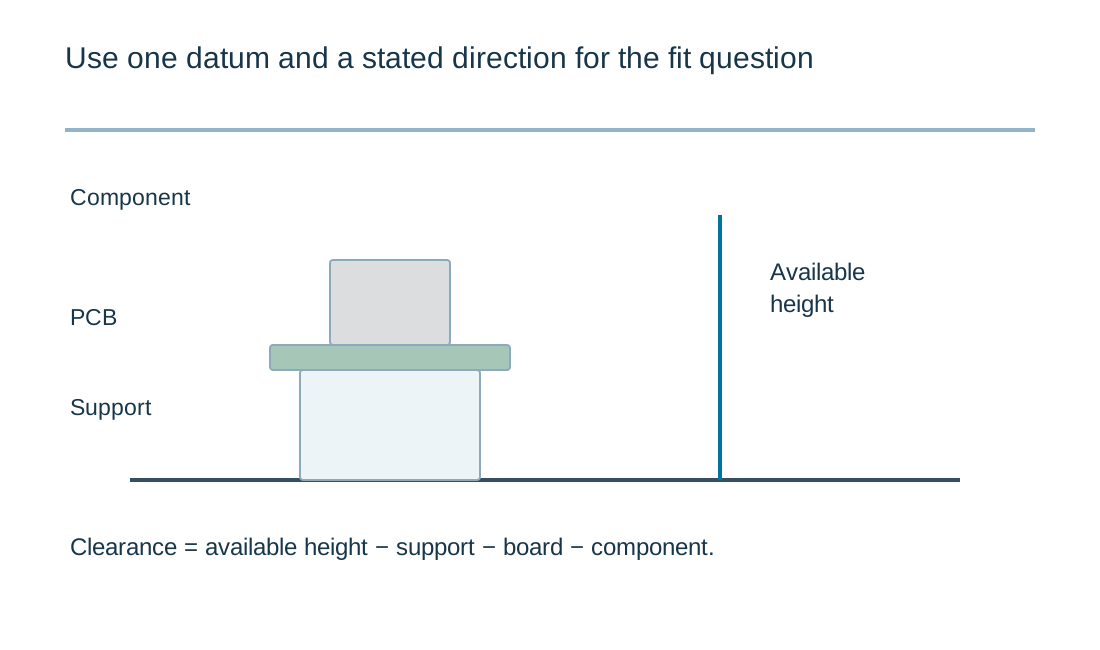
Choose one direction and define the result you want: clearance, mating height or another linear relationship. Assign a sign to each nominal contribution according to that direction. For independent drawing limits treated as worst-case bounds, the nominal result is the signed sum and the total bound is the sum of the absolute tolerances.
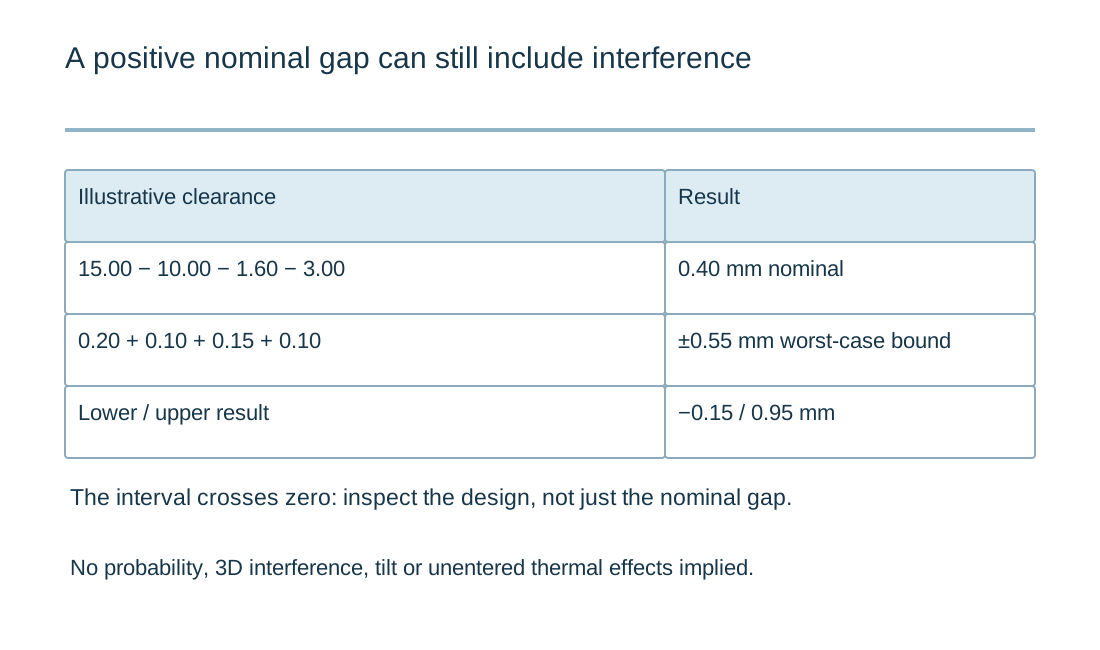
As a teaching example, suppose a 10.00 ±0.10 mm support, a 1.60 ±0.15 mm board and a 3.00 ±0.10 mm component stack must fit below a 15.00 ±0.20 mm available height. Define clearance as enclosure height minus the three occupied dimensions. Nominal clearance is 0.40 mm; the worst-case bound is ±0.55 mm, giving −0.15 to 0.95 mm.
That interval exposes a possible interference under the entered limits. It does not predict the probability of interference or include board bow, tilt, fastener compression, thermal expansion or other unentered effects. Do not substitute root-sum-square tolerances without a justified statistical model and acceptance process. The worksheet makes the simple stack visible so the next mechanical review can be specific.
| Review item | What to establish |
|---|---|
| Datums and sequence | Common references, insertion path, fastening order and tool access. |
| Dimensional model | Signed nominal contributions, worst-case bounds and omitted effects. |
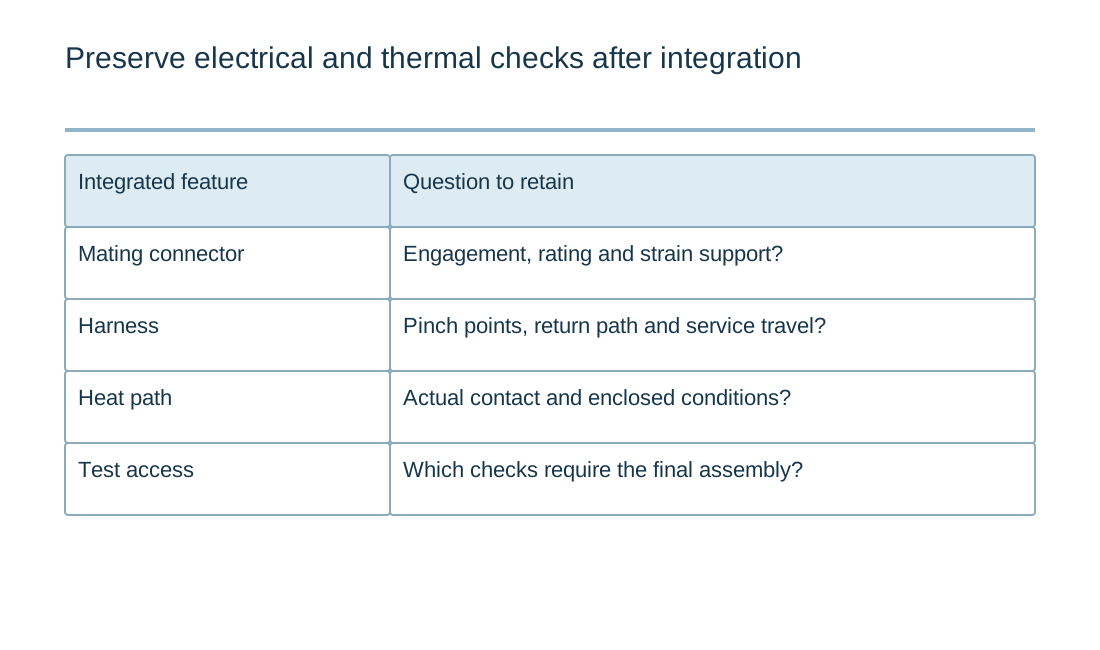
| Connectors | Exact mating parts, engagement conditions, ratings and strain support. |
| Harness and heat | Routing, service motion, return paths and assembled thermal conditions. |
| Release scope | Included parts, fixtures, integration tests, records and final configuration. |
Mechanical stack interval comparison
Mechanical stack interval comparison
Use the current inputs and keep the assumptions
Load the example to see the units and record format, then clear it before entering your own revision. Example values are illustrative and do not select components or establish acceptance limits. Every field needs an intentional value; a blank number is not treated as zero. For CSV input, retain the header and put one item on each row. Quoted cells can contain commas, but duplicate headers and malformed rows are rejected.
Generate a result only after checking the measurement boundary, operating condition and units. Editing an input invalidates the old result and disables its download until you calculate again. An edited example stays labeled as an example. The report is created locally; it does not upload a design, send an enquiry or populate the Contact form. Attach it manually if it helps explain a requirement. You can contact RAYPCB without completing the tool.
| Input | What to establish before using it |
|---|---|
| Review reference | Use a nonconfidential revision label. |
| Signed dimension stack · CSV | Use signed nominal contributions along a defined datum; tolerances are nonnegative symmetric bounds. |
| Permitted stack minimum · mm | From the actual enclosure/interface drawing. |
| Permitted stack maximum · mm | Same datum and operating condition as the stack; no automatic assembly approval. |
Optional cost comparison from your own allowances
Use a quotation or a clearly labeled internal assumption for each input. Keep the quantity, construction and inspection scope the same when comparing alternatives. This uncalibrated planning model adds entered values; it contains no current market rates and does not issue a RAYPCB quotation. You can contact the team without completing it.
Assembly scope allowance comparison
Review connector mating as an electrical and mechanical task
Use the exact connector and mating-part drawings, including allowable engagement, orientation and applicable mounting requirements. Check whether the assembly constrains the connector in a way the selected parts permit. A board edge or housing opening can be correctly located while the contact engagement remains outside the required condition.
Electrical ratings also depend on the exact part and operating conditions. Consider current sharing, temperature rise, insulation conditions and the number of simultaneously loaded contacts as required by the selected documentation. Do not infer a whole connector's usable power from a single nominal contact rating.
Assign strain relief and support where cables and connectors experience installation or service loads. The solder joints should not be assumed to absorb every external load. Confirm the intended mechanical load path with the responsible designer, and keep the assembly instruction consistent with the released arrangement.
Route harnesses with installation and service in mind
Define connector orientation, wire identification, routing constraints and required support. Keep moving or removable parts in view. A harness that reaches comfortably on a bench may become pinched when the cover closes or strained when a service panel opens. Review the actual installation sequence and permitted service motion.
Separate power, sensitive signals and any specified shielding or grounding relationships according to the circuit and system requirements. This is not a universal instruction to place every cable in a different bundle; the intended return paths and interference mechanisms must guide the arrangement. Record shield termination and chassis connections explicitly.
For motion equipment, the robot-arm electronics guide adds feedback and moving-interface considerations. A harness continuity test is useful but does not establish performance throughout motion, repeated service or the final electromagnetic environment. Identify those integration tests separately.
Preserve thermal and test access after assembly
Evaluate heat flow in the assembled configuration. A component with adequate open-bench behavior may face different airflow and neighboring temperatures inside the enclosure. Interfaces intended to conduct heat need controlled contact conditions; a nominal gap calculation alone does not establish thermal resistance or compression of an interface material.
Plan electrical measurements and programming before covers or brackets obstruct access. Decide which tests occur on the open PCBA, which occur on the subassembly and which require the complete unit. Record final switch positions, installed jumpers and software configuration after testing so the shipped state is unambiguous.
The industrial manufacturing release guide helps allocate these observations to a controlled record. Inspection of fasteners, connector engagement and labels complements electrical testing. None should be silently substituted for a test that requires the assembled product under representative operation.
Request a quotation with a complete integration boundary
Supply board files, BOM, mechanical drawings, harness definitions and a delivery index. Identify customer-supplied parts and the exact mating items required for fit checks. State acceptance criteria and which fixtures, tools or software are supplied by the customer versus developed for the project.
The optional budget worksheet uses entered preparation, unit and test allowances. It does not estimate a current market price from the number of boards or fasteners. Compare scenarios at the same quantity, currency and delivered scope; enclosure work and integration tests must be treated consistently.
Attach a tolerance worksheet when it explains an unresolved fit question, but preserve the controlled drawings as the source of dimensions. A focused enquiry might ask about assembly access, test-fixture requirements or a mating stack that crosses zero clearance. That is more useful than a general request to make the electronics fit after the parts arrive.
Make interface responsibility explicit
A module has two useful boundaries: the physical object delivered by the supplier and the functions accepted at that boundary. These may not match a drawing of one circuit board. Harnesses, brackets, programming and final installation can belong to different parties, so name their owners before treating a subassembly as complete.
Tie dimensions to common datums and electrical requirements to defined connector pins and operating states. Agree which tests occur before enclosure integration and which need the assembled product. Reserve access for those later checks. When a mating item changes, review the interface contract even if the PCB artwork remains identical. A small, specific open-item list is more useful than an overall readiness percentage because it shows which decision actually prevents release or quotation.
Standards, source context and limits
Use the exact device, system and material documents relevant to the released design. A public reference design demonstrates a particular implementation under its stated conditions; changing its parts, layout, enclosure or firmware creates a different verification task. Standards summaries here identify the type of evidence to request, not every clause of a licensed standard. Component qualification, board workmanship, product validation and regulatory acceptance are separate decisions.
For fabrication scope and the agreed construction requirements, see PCB manufacturing.