
RAYPCB · Assembly engineering guide
How to Choose an SMT Stencil: Size, Thickness and Process Fit
Choose an SMT stencil by resolving the equipment interface, required deposits, aperture geometry and production controls in that order. Component pitch is a useful clue, but it is not a complete thickness specification. This guide gives engineers and buyers a decision sequence that ends with a reviewable order rather than a universal recommendation detached from the actual board.
Preliminary files are welcome. Identify your board revision, printing equipment and the question you need to resolve.
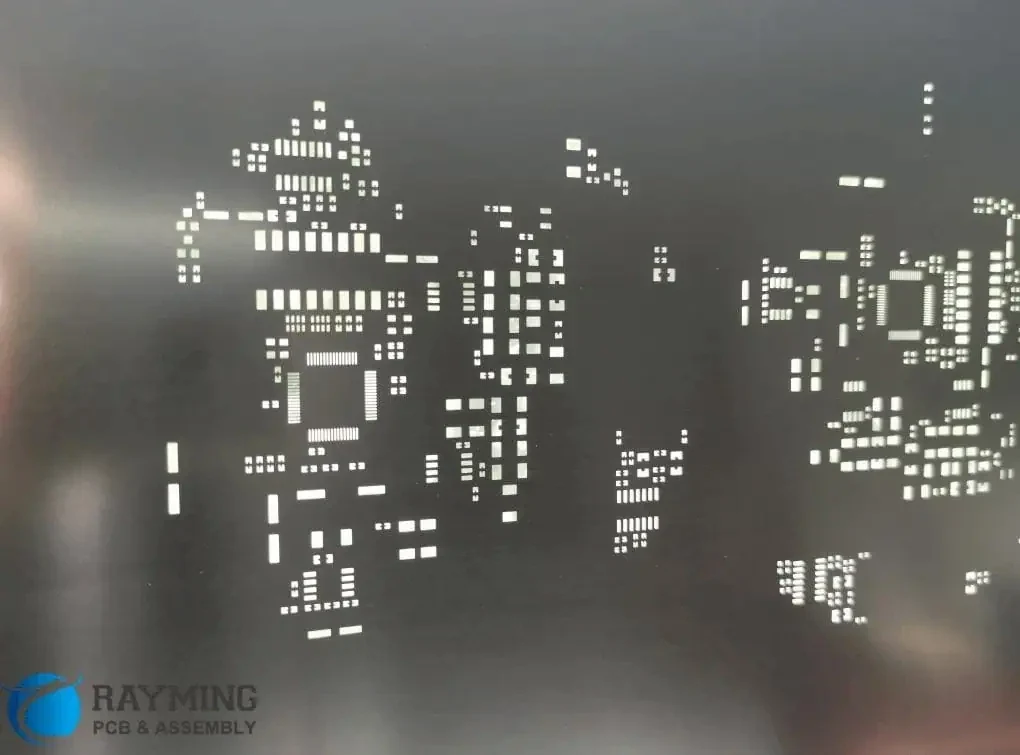
What to establish before the next decision
| Review item | Working requirement |
|---|---|
| First decision | Confirm material, board revision and actual production panel or image. |
| Second decision | Match the holder and usable area before approving a foil outline. |
| Third decision | Compare thickness against actual aperture geometry and required deposit. |
| Fourth decision | Resolve mixed deposits and any local step with the printing team. |
| Final decision | Compare matched quote scope, approve artwork and preserve the revision trail. |
Find the resource for your printing task
Select the available mounting equipment and the issue you need to resolve. The guide suggests relevant next pages without assigning an unsupported quality score or forcing you through a quotation form.
RAYPCB ENGINEERING
Stencil EngineeringStencil Route Selector
Loading Stencil Route Selector…
Step 1: define the printing task
Identify the material being printed, the board revision, the production panel and the assembly side. For solder paste, determine which component groups create the most demanding deposits. Include no-fit variants and large exposed pads. A stencil chosen for an early prototype can be inappropriate for a later panel or a different component population even when the board family name is unchanged.
Separate the desired deliverable from the process decision. You may need a foil, a framed stencil, a replacement tool or a complete assembly build. The PCB Stencil hub compares the product routes, while this guide concentrates on the order in which to resolve the technical questions. A clear task prevents a purchasing form from becoming the accidental design authority.
Step 2: confirm the printer or fixture interface
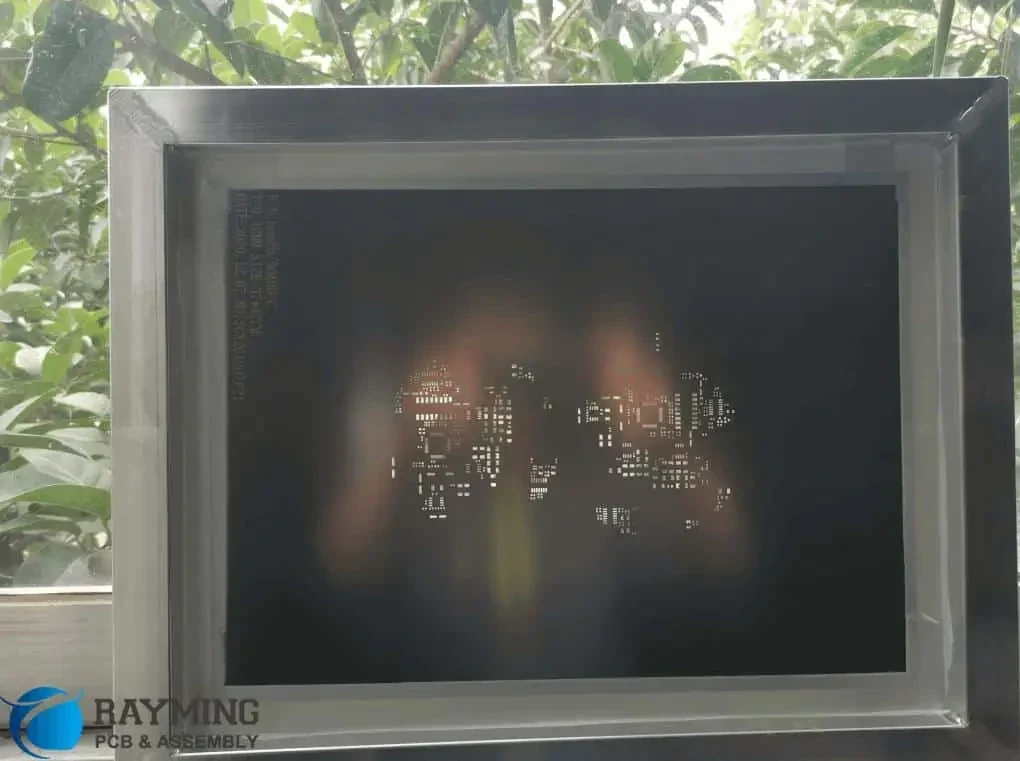
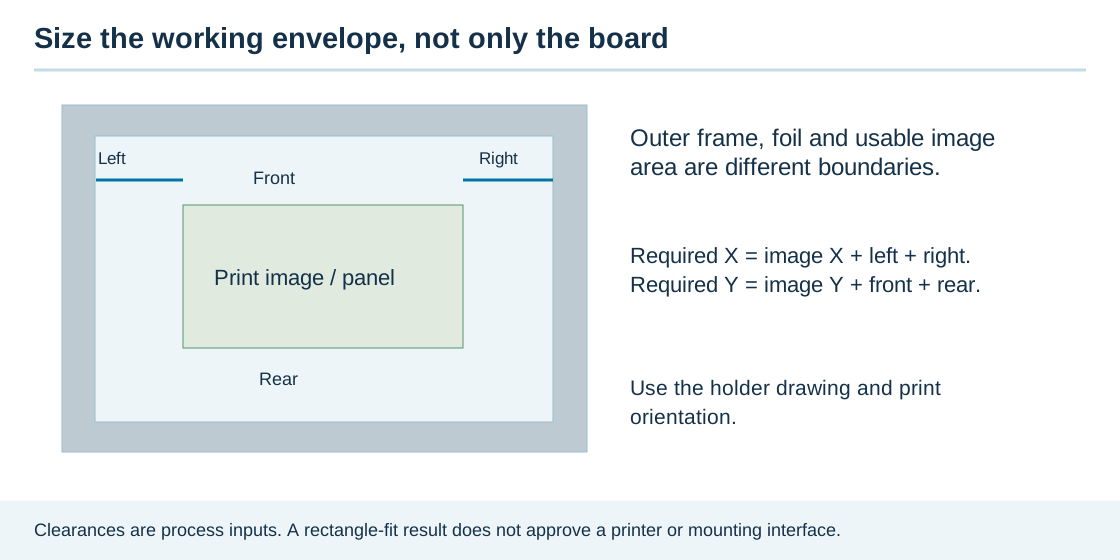
Record the accepted frame or foil format, usable image area and locating features. For a tensioning system, use the actual interface drawing. For a manual fixture, define how the board and stencil are held and supported. Do not assume that two foils with the same outside dimensions mount the same way.
The dimensional tool adds the image and your required clearances before comparing them with the usable rectangle. It does not use the outer frame as a substitute for usable area. Include blade travel and paste-roll clearances from the actual process. If the equipment is not yet chosen, use the stencil printer guide before approving a custom outline that might constrain the eventual setup.
Stencil usable-area and clearance checker
Use the complete print image or panel envelope in its planned orientation. Enter independent left, right, front and rear clearances from the intended holder and printing process. Required X equals image X plus left and right clearance; required Y equals image Y plus front and rear clearance. Remaining space equals your usable dimension minus that requirement.
For example, a 100 × 80 mm image with 20 mm left/right and 30 mm front/rear clearances needs a 140 × 140 mm rectangle. In a 250 × 200 mm usable area, the remaining dimensions are 110 and 60 mm. These margins are arithmetic examples, not recommended machine clearances.
The checker does not rotate the image, select a catalogue frame, analyze tension or evaluate blade travel. It also does not parse a Gerber file. Use the result to clarify dimensions before sending the actual printer or holder drawing for review. A geometric fit is one part of compatibility, not an approval of the complete setup.
RAYPCB ENGINEERING
Stencil EngineeringStencil Design Workbench
Loading Stencil Design Workbench…
Step 3: compare candidate thicknesses with actual apertures
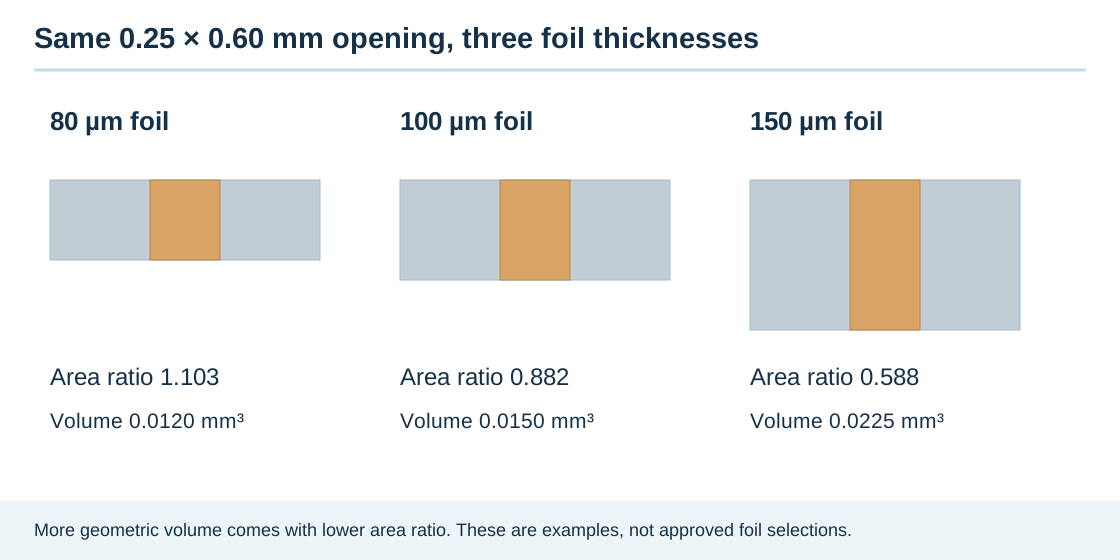
Use the minimum opening dimensions and the required deposit volume, not just the component pitch. Area ratio compares opening area with the aperture-wall area. Thicker foil increases volume but also increases that wall area. A design with one easy aperture group and one demanding group should not be represented by a single board-average dimension.
Review several candidate thicknesses in the aperture and deposit workbench. Treat familiar thickness values as candidates rather than factory promises. If the smallest opening requires a thinner foil, check what happens to the larger lands. The correct next action may be an aperture change, a package-specific pattern, a local step or a review of another deposition route.
Step 4: resolve conflicting deposit requirements
Mixed component populations can require different amounts or distributions of material. A stepped stencil is one possible response, but it introduces a transition that must work with blade travel and board contact. It should be selected because the geometry and process support the intended benefit, not simply because a board contains both small and large packages.
For an exposed thermal pad, begin with the component manufacturer's attachment guidance and a deliberate window pattern. The QFN stencil design page provides a coverage calculation that keeps dimensions visible. For local thickness, the stepped stencil guide helps define zones and faces. These are distinct engineering tasks and should not be compressed into an automatic “advanced stencil” option.
Follow the working sequence
The steps remain readable without animation. Use the optional player to follow one operation at a time; it starts paused and respects reduced-motion preferences. This is a conceptual explanation, not a production video.
- Support
Locate and stabilize the board or panel.
- Align
Match the approved stencil to the correct side.
- Print
Use the defined material and controlled recipe.
- Separate
Release the board without disturbing the deposit.
- Inspect
Check the printed material before placement.
- Continue
Release or correct according to the assembly process.
Step 5: choose manufacturing and finishing from evidence
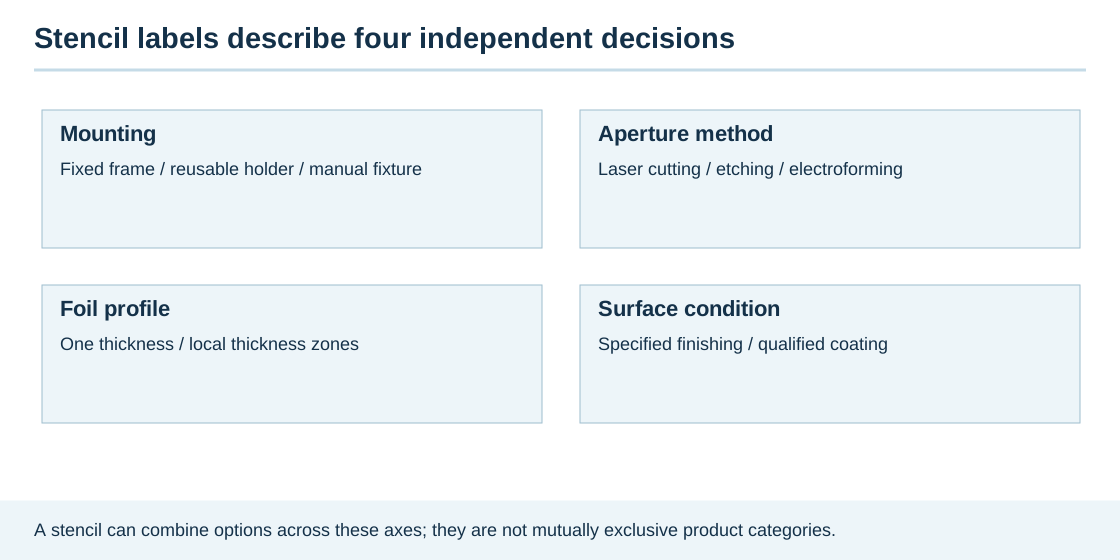
Laser cutting, chemical etching and electroforming are different aperture-making routes. Their suitability depends on the proposed geometry and the supplier's process. Surface treatment and coating choices add another dimension to the comparison. Ask what the finished tool will be and how the critical apertures will be checked.
Use the method comparison guide to structure that discussion. Avoid selecting a process from unsupported claims about universal minimum pitch or guaranteed print life. If a special coating is proposed, include cleaning compatibility and the intended maintenance plan. A feature that cannot be maintained in the available process may not deliver its expected benefit.
Step 6: define the inspection and qualification task
Specify what is required for tool acceptance: identity, dimensions, thickness, mounting and any special evidence. Then define the printing trial separately. A stencil inspection report does not demonstrate the paste deposit on your board, while one attractive first print does not establish repeatability through a production run.
Select representative aperture groups and an inspection recipe appropriate to the planned process. Include relevant repeat-print or restart conditions. Keep measured results with the stencil revision and material identity. For stepped tools, compare zones separately. For hidden-joint packages, define the downstream inspection scope so a good print is not mistaken for complete assembly qualification.
Step 7: compare cost on a common scope
Obtain comparable quotations for foil processing, mounting, optional steps or treatments, engineering, inspection and freight. Confirm the number of stencils and whether top and bottom use separate foils. A board quantity is not a stencil quantity, and a combined two-side layout requires its own fit and operating review.
Include existing equipment in the comparison. A frameless foil can be attractive when a compatible holder is already available, but a new holder and additional setup work change that calculation. Use the allowance-based planner in the PCB Stencil hub if you have rates to compare, or request a direct file review if you do not. No calculator should invent a market price to fill a missing quotation.
Step 8: freeze the decision and preserve a revision trail
Before release, confirm side, orientation, panelization, critical aperture changes and mounting details against the approved files. Name who owns the final artwork. Keep the stencil identifier, drawing and process recipe together, and withdraw superseded tooling from the released set. These controls are especially valuable when a board moves from prototype to repeated assembly lots.
Use the custom stencil RFQ guide to prepare the final handoff. If the broader need is populated boards, continue to PCB Assembly with the complete project scope. The best selection is one that the manufacturer and assembly team can interpret consistently, verify with appropriate evidence and reproduce when the next approved order arrives.
Keep the cost discussion tied to the actual task
If this review changes the stencil construction, ask for a quotation against the resulting artwork and equipment interface. Separate the physical tool from engineering work, any special inspection and freight. A change in aperture design can affect the scope even when the outside board dimensions remain identical.
For an allowance-based calculation, use the PCB Stencil hub and cost planner. That tool deliberately uses your entered rates rather than presenting unverified tariffs as current prices. A process improvement should also be assessed against evidence from the actual assembly; this page does not assign a monetary saving to a hypothetical yield increase. If the immediate requirement is engineering help or a complete build, proceed directly to an enquiry.
Send a brief an engineer can act on
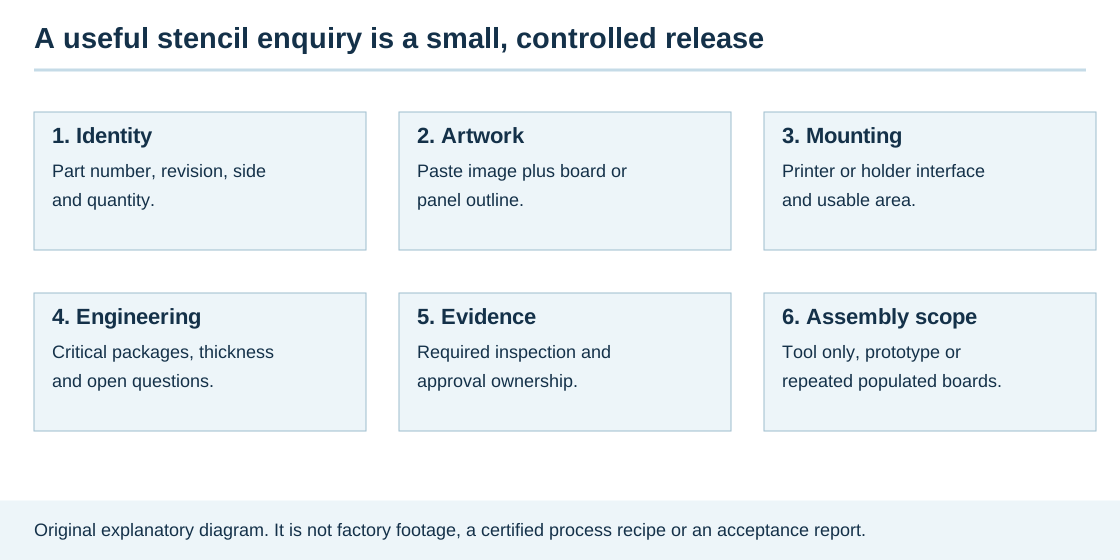
Include the paste artwork, board or panel outline, side and revision; describe the printer, holder or manual fixture. Identify critical components and the exact decision that remains open. For an existing process problem, add the observed location, relevant conditions and available inspection evidence. Keep files and photographs tied to the same revision.
State whether you need stencil fabrication only or a populated-board project. PCB Assembly services can address the broader scope of procurement, placement, soldering and agreed inspection or test. The assembly process guide explains how the printing step connects to the rest of the build.
Download the current tool brief or open an email draft when you want to share the calculation. Attach design files separately. The Contact link opens the existing enquiry page; it does not silently transmit calculator values or claim an integrated Gerber upload. You can enquire before completing a tool when your question is about the manufacturing route rather than a numeric result.
Questions about this stencil task
Can I select thickness from component pitch alone?
Pitch is useful context but does not define opening area, wall contact or required deposit. Compare the actual aperture families and package guidance. Then verify the candidate thickness in the intended process rather than treating a pitch table as automatic approval.
What if I do not know the printer interface yet?
Keep mounting and outside dimensions open until the equipment or holder is identified. You can still review package and aperture requirements. Ordering a custom outline too early can create a foil that prints the right pattern but cannot be mounted usefully.
Does this calculator approve a stencil for production?
No. It makes its stated geometry or arithmetic visible. It does not inspect your files, predict paste release or certify compliance with an IPC standard. Use the result alongside the actual drawing, component guidance, qualified process and agreed inspection evidence.
What information helps if I am unsure about the next step?
Send the current design revision and describe the unresolved task: mounting fit, deposit geometry, process behavior or quotation scope. Include the relevant equipment and component details. Preliminary information is acceptable when its status is clear; approval of a production tool requires the agreed final data.
Continue with the next useful decision
Original engineering and standards references
Use component and process documents in their stated application context. Public IPC contents establish scope, not every licensed clause. Specify the agreed standard revision and acceptance requirements on the order; this guide does not claim universal IPC certification for a geometry calculation.