
RAYPCB / Production transition
PCB prototype to production: decide with evidence
Connect design learning, pilot findings, supply readiness and acceptance records to a controlled release. A larger quantity alone does not establish readiness.
Move from prototype to production when the evidence supports a repeatable build
The transition from PCB prototype to production should be based on a controlled design, resolved build findings, a workable supply plan and a defined verification process. Quantity alone is not the release criterion. Ten boards can be a repeat production order, while several hundred boards may still be an experimental build with unresolved design risks.
A prototype asks a question: does the circuit behave as intended, does the board fit, or can a proposed construction meet the requirement? Production asks whether the approved configuration can be built and accepted consistently. The transition record should connect the learning results to the configuration that will actually be ordered again.
Use PCB prototype manufacturing for the first-build route. This guide addresses the decision after learning: which issues remain, who owns them and what must be recorded before committing to repeat supply. It does not impose a universal number of samples or approve a product for sale.
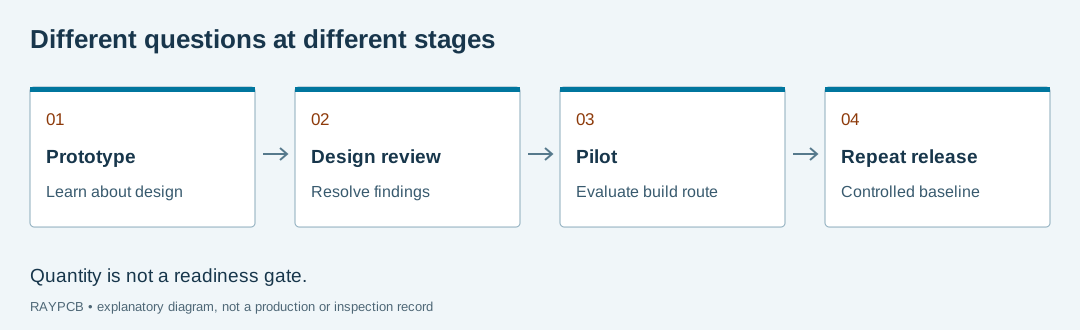
First define what the prototype was meant to prove
Separate design verification from fabrication and assembly acceptance. A bare board can meet its agreed manufacturing specification while the assembled circuit still needs functional evaluation. Likewise, a prototype working once on a bench does not establish performance across all intended conditions or demonstrate a repeatable production process.
Write a short question-to-evidence list. Mechanical fit may need a controlled enclosure comparison. Signal behavior may need a measurement against defined limits and conditions. Thermal performance needs the relevant loads, environment and measurement method. Manufacturing review may identify features that require a revised stackup or assembly process. Keep the evidence attached to the actual tested revision.
Do not carry an unexplained prototype deviation into the production baseline. A hand modification, substitute component or temporary firmware image can be useful during learning. Document it and decide whether it becomes part of the design, is removed, or remains a narrowly authorized exception. Otherwise, the successful prototype and the released files may describe different products.
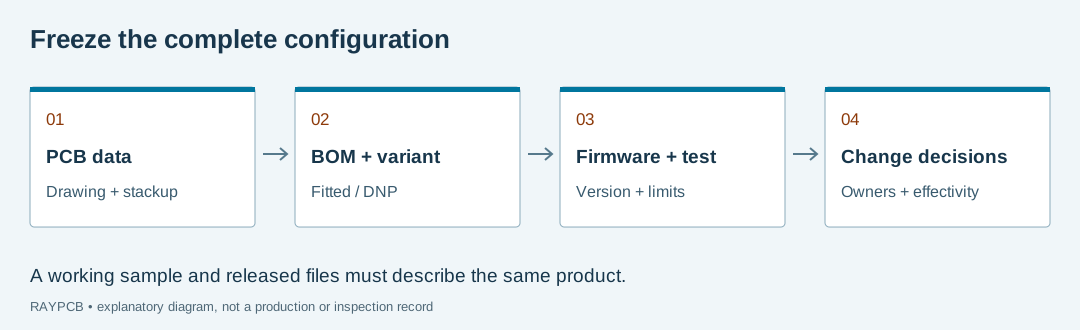
Freeze a complete configuration—not just a Gerber ZIP
Identify the fabrication data, drawing, stackup, BOM, assembly drawing, placement file and firmware as applicable. Include variant rules, programmed identifiers, labels and any special process instructions. The release should say which revision of each item belongs together. A single board revision can be associated with several assembly variants, so a clear variant identifier matters.
Keep approved engineering dispositions with the release. If the fabricator adjusted artwork or the assembler used an approved substitute, record whether that change is reflected in the new files. Recreating production from an old email thread is a weak control. A readable release index helps procurement, manufacturing and quality use the same configuration.
| Question | Useful evidence | Who must decide |
|---|---|---|
| Does the design meet its intended requirements? | Defined tests, conditions, results and unresolved limitations | Design/product owner |
| Which configuration is released? | File index and approved change record | Configuration owner |
| What did the pilot reveal? | Build findings and disposition of exceptions | Manufacturing and quality owners |
| Can the BOM be supplied? | Availability assumptions and approved alternatives | Procurement and design owners |
| How will units be accepted? | Inspection/test plan, limits and records | Quality and test owners |
| How will later changes work? | Effective point, inventory plan and approval path | Program and commercial owners |
Use a pilot to learn about the intended manufacturing route
A pilot should answer questions about the planned production setup, material kit, tooling and inspection route. Record where it differs from the expected repeat build. A manually reworked prototype may not reveal the same issues as the intended automated assembly route, while an early pilot with temporary fixtures may not establish the final test throughput.
Choose pilot quantity and sampling based on the product, risk and question being investigated. There is no universal batch size that proves readiness. Explain what the run can and cannot establish. A small pilot may expose a placement-file problem without providing enough evidence to estimate a stable long-term defect rate.
Close findings with a disposition, not just a color on a checklist. State whether the design changed, the process changed, a requirement was clarified or an exception was approved. Identify the owner and the evidence of closure. If another build is needed to confirm the correction, keep that action open rather than declaring the issue resolved after editing the drawing.
Review supply continuity before scaling the commitment
Check whether the prototype relied on a small quantity of readily available parts that cannot support the intended release schedule. Confirm exact manufacturer part numbers, approved alternatives and any parts with uncertain availability. A distributor stock observation is time-sensitive and is not a future allocation. Record the date and basis of the supply assumptions.
Separate a forecast from a purchase authorization. A supplier may need visibility of likely demand without being authorized to buy the entire forecast. Agree which materials can be purchased, in what quantities and with whose approval. Minimum pack quantities and long-lead commitments can create unused inventory if the design changes.
The component responsibility guide helps allocate sourcing, alternatives and shortages. For continuing OEM programs, electronic contract manufacturing provides the wider context of release schedules, change control and supply responsibilities.
Prepare a transition decision record
Use the six-item worksheet to identify evidence and open actions. It deliberately avoids a readiness percentage: one unresolved critical item can matter more than several completed administrative items. Refer to actual documents rather than checking a box because a meeting occurred.
RAYPCB ENGINEERING
Procurement and HandoffPrototype-to-production decision record
Loading Prototype-to-production decision record…
The optional worksheet needs JavaScript. Use the readable checklist above or contact RAYPCB directly.
If every row has a reference, the result still says that approval has not been verified. The tool cannot inspect test reports, evaluate product safety or authorize production. The broader electronics NPI checklist helps organize an ongoing introduction program; this worksheet focuses on the particular transition decision.
Balance recurring savings against revision and inventory risk
A larger order may spread setup across more units, but it also commits more material and finished stock to one configuration. Compare the full scenario: setup, recurring work, fixtures, verification, inventory and possible change exposure. Do not treat a lower unit price as proof that the larger release is the best decision.
Invented planning example: at an assumed USD 12 per board and USD 600 setup, 100 boards average USD 18 each. At 500 boards using the same assumed unit allowance, the average is USD 13.20. The arithmetic does not predict a supplier offer. It also does not price the risk that a later revision makes some of the additional 400 boards unusable.
Decide which uncertainty a smaller release buys time to resolve. If a connector location is still under evaluation, committing to a large mechanical configuration may be premature. If the design is frozen and demand is stable, a repeat release can be appropriate without another “prototype” label. The decision should follow evidence and commitments rather than a marketing category.
Use the early budget scenario to document your own assumptions. Reassess rates and exclusions for each quantity. A tool calculation cannot infer material utilization, supplier capacity, acceptance costs or changing component availability.
Define what happens after release
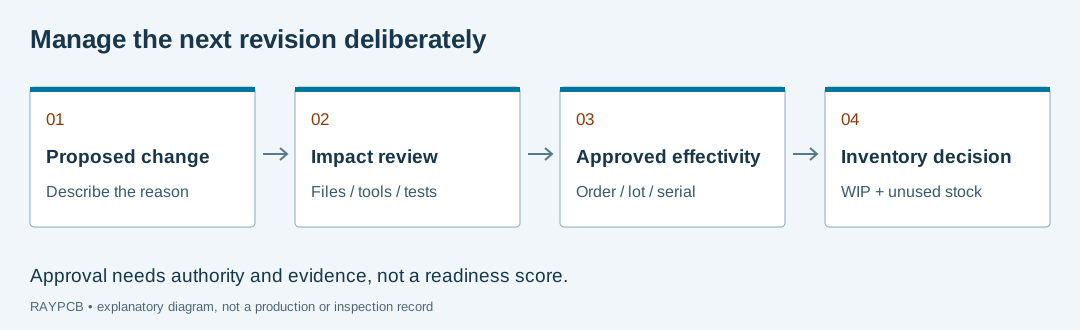
Assign an owner for engineering changes and specify how the effective point will be identified. A change may apply from a particular order, lot or serial range. Determine how work in progress, purchased parts and completed inventory will be treated. Do not send revised files without also discussing their effect on already authorized work.
Retain the build and acceptance record for the released configuration. A repeat order should reference that baseline and list differences explicitly. Agree which test and traceability records must be retained or supplied for each lot. The appropriate depth depends on the contract and product; referencing a traceability framework is not evidence that every record exists.
After the first repeat build, review the actual findings against the original transition assumptions. Update the plan when supply, process or design evidence changes. Production readiness is not a permanent label that removes the need for change control.
Common transition questions
How many prototypes should I make before production?
Choose a quantity that can answer the defined design and process questions. No single count establishes readiness. The required evidence depends on product risk, conditions, variation and the intended acceptance plan.
Can a successful prototype be used as the production reference?
It can inform the baseline if its actual configuration and modifications are documented. Reconcile it with the released files, BOM and firmware first. An unexplained hand modification should not become an implicit requirement.
Does passing inspection prove the product works?
No. Manufacturing acceptance, assembly workmanship and functional requirements have different scopes. Define the necessary verification and the authorized decision makers before release.
Can I discuss a production plan while findings remain open?
Yes. Share the open questions and proposed milestones. Planning does not require pretending the design is approved; a manufacturing commitment needs the agreed conditions and authorizations.
Bring the open questions to RAYPCB
Send the project reference, available files, quantity options and the decisions you need help with. If you used the worksheet, review its assumptions and attach the downloaded brief yourself. Opening Contact does not send the worksheet or place an order.
Technical references and scope
These official references explain data, standards or handling concepts. Use the applicable controlled documents and project agreement for acceptance. Links do not certify RAYPCB, qualify a product or replace engineering approval.