
RAYPCB · ENGINEERING GUIDE
Paste Mask vs Solder Mask: Layer Purpose, Apertures and Data Checks
Paste mask and solder mask describe different manufacturing information. The paste layer defines stencil apertures used to deposit solder paste during assembly. The solder-mask layer defines openings in the permanent coating on the PCB. Copying one layer into the other can create a board that looks plausible in CAD but prints or solders incorrectly.
Use the comparison below to review the role of each layer, especially for fine-pitch components and thermal pads. The tool compares ideal rectangular areas and stencil volume; it does not generate a stencil file or choose a qualified printing process.
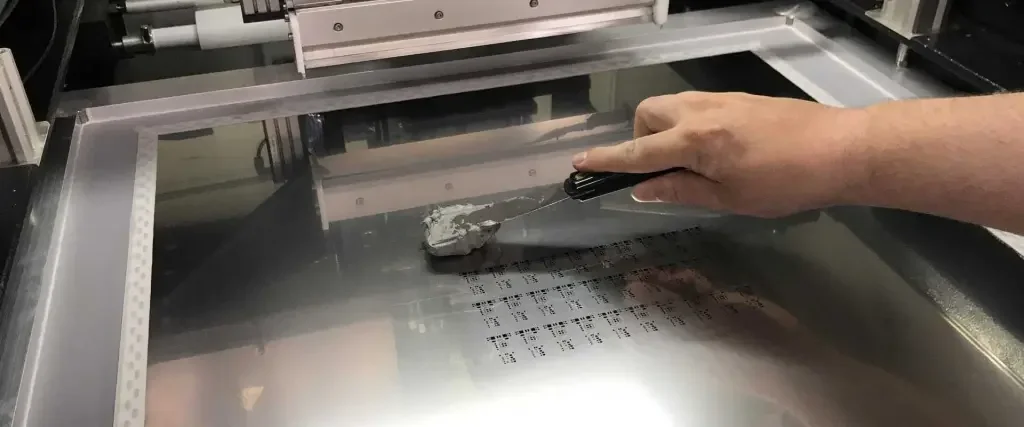
Follow the material through assembly
Solder resist stays on the board after fabrication and assembly. It protects selected surfaces and helps define where solderable copper remains exposed. Solder paste is a temporary mixture deposited through a stencil; after reflow, the joint and flux residues depend on the material and process. The stencil itself does not become part of the PCB.
These different lifetimes explain why the layers need separate ownership. The bare-board fabricator uses the mask data with the copper and construction. The stencil and assembly teams use paste apertures with the land pattern, component and printing process. An archive should identify both even when the same CAD export command produces them.
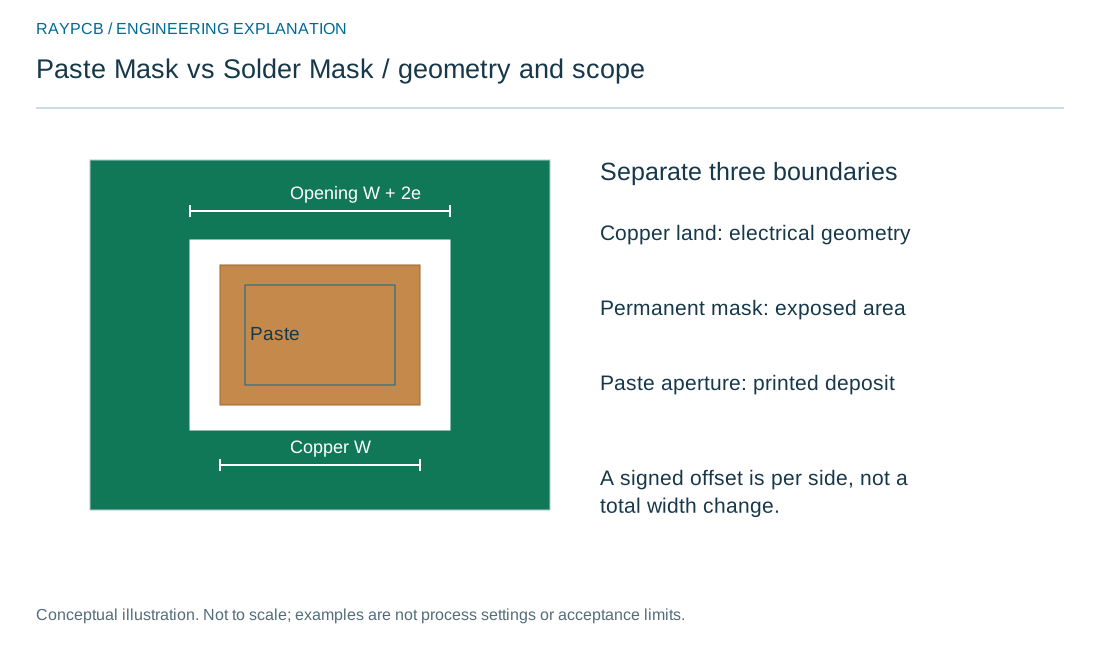
Copper, mask and paste comparison
Copper, mask and paste comparison
Use the current inputs and keep the assumptions
Start with the feature or process question you actually need to resolve. Fields are blank until you enter values or deliberately load an illustrative example. Example mode remains labeled after editing, so a sample is not silently presented as verified project data. Clear the example before preparing a project-specific record.
Use the units printed beside each input. Keep the drawing revision, measurement basis and source of any allowance in your controlled project records. A field that asks for a limit expects your agreed requirement; the example is not an IPC threshold or a statement of RAYPCB capability. A numerical result should lead to a focused review, not replace it.
Changing any input invalidates the displayed result and disables its download until you calculate again. The text download contains the current inputs, results and assumptions. Nothing is uploaded, stored in analytics or automatically transferred into the Contact form. You may attach the file manually if it helps explain your enquiry; completing the worksheet is optional.
| Input | What to establish before using it |
|---|---|
| Review reference | Use a nonconfidential reference to connect this worksheet to the correct design or process revision. |
| Copper land width · mm | This is the electrical land, not the stencil aperture. |
| Copper land length · mm | Use the released footprint geometry. |
| Signed solder-mask expansion · mm | Applies to the permanent-mask opening only; it is not a paste reduction. |
| Paste aperture width · mm | Use the actual stencil opening; a segmented pattern needs individual aperture areas. |
| Paste aperture length · mm | Keep linear dimensions distinct from area percentages. |
| Stencil thickness · mm | Ideal aperture volume excludes transfer-efficiency and paste-process effects. |
Compare the three relevant shapes
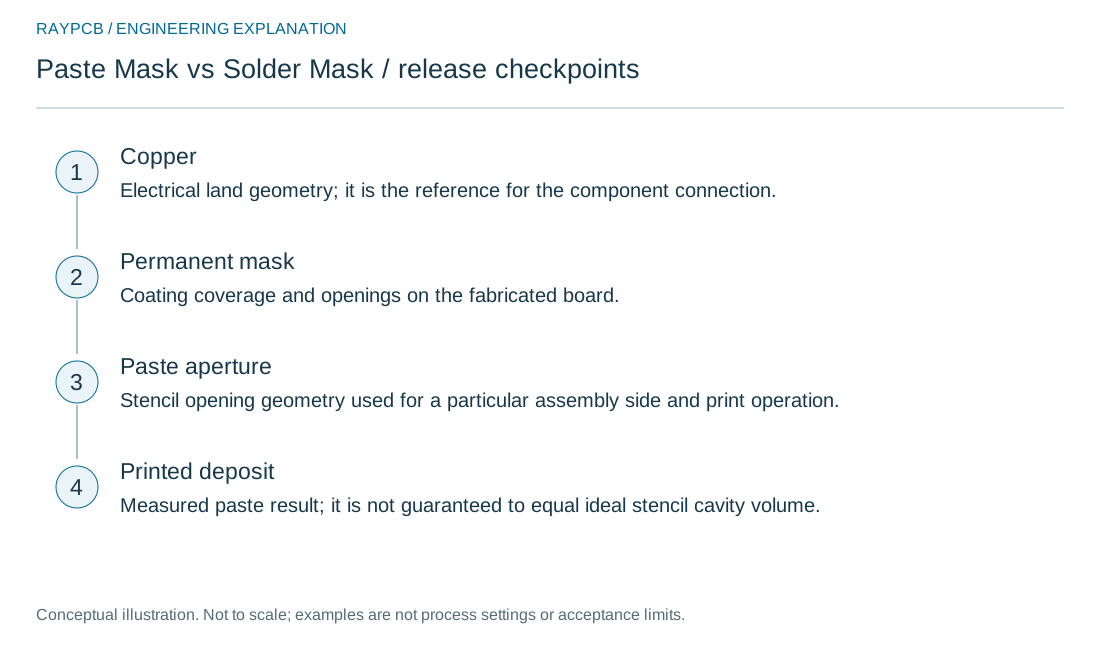
Start with the copper land. Place the permanent-mask opening around or over that land according to the intended strategy. Then place the stencil aperture appropriate to the solder-paste requirement. All three may differ in size, shape and segmentation. A large exposed thermal pad often makes the distinction especially visible.
The worksheet uses separate dimensions for these rectangles. It reports the paste-to-copper area ratio and an ideal aperture volume from stencil thickness. A larger mask opening does not mean the aperture should grow by the same amount. The appropriate paste deposit also depends on release efficiency, separation, print settings, paste and package behavior.
| Review item | What to establish |
|---|---|
| Copper | Electrical land geometry; it is the reference for the component connection. |
| Permanent mask | Coating coverage and openings on the fabricated board. |
| Paste aperture | Stencil opening geometry used for a particular assembly side and print operation. |
| Printed deposit | Measured paste result; it is not guaranteed to equal ideal stencil cavity volume. |
Interpret percentage reductions carefully
A percentage can refer to area or to a linear dimension. Reducing width and length each by ten percent leaves eighty-one percent of the original rectangular area. Reducing area by ten percent while retaining aspect ratio requires a different scale factor. Check the actual rule definition in your CAD version rather than relying on the word reduction alone.
Altium's documented paste-mask rules distinguish absolute and percentage treatment. The output geometry is the important verification point, especially when migrating libraries or using object overrides. Preserve the intended aperture dimensions in the stencil review so a percentage setting cannot hide an unexpected physical result.
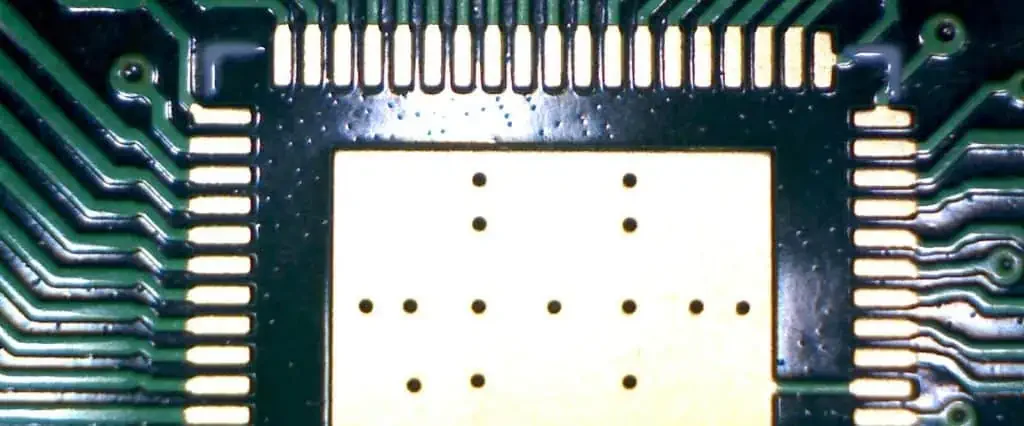
Treat thermal-pad segmentation as its own design
Several smaller apertures can distribute paste across a large thermal land. The segmentation pattern, web arrangement and total open area need review against the component recommendation and assembly process. A single area ratio does not tell you whether the deposit will collapse evenly, release well or produce acceptable voiding.
Keep nearby signal lands and vias visible in that review. Open vias can provide paths for solder loss; treatment of those vias belongs in the board construction. Do not attempt to solve an unreviewed via-in-pad condition merely by adding more paste. Ask the relevant teams to agree the combined land, via and stencil arrangement.
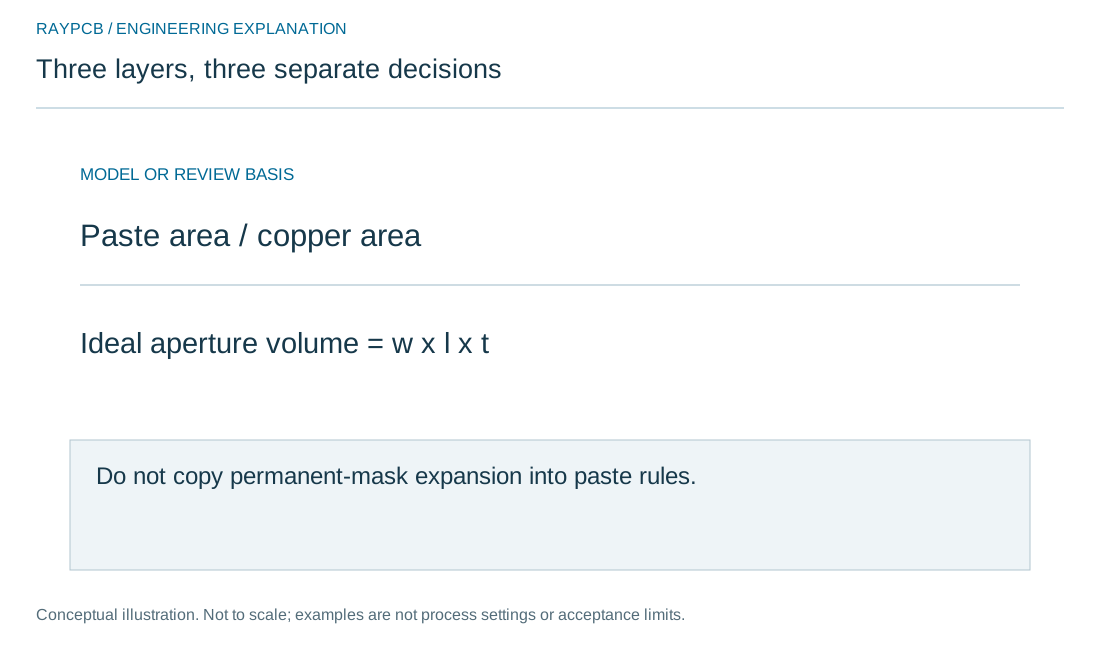
Use aperture volume as a comparison, not a promise
For a rectangular aperture, the ideal cavity volume is width multiplied by length multiplied by stencil thickness. It is a geometric starting point. Actual printed volume may differ because paste does not transfer perfectly and printing conditions vary. The tool deliberately does not convert its answer into a guaranteed joint height or a production yield.
When comparing alternatives, hold the units and aperture count constant. If one option uses segmented apertures, sum their individual areas rather than using the outer envelope that includes stencil webs. Record both the nominal geometry and any measured paste-deposit result so the design can be adjusted from evidence.
Package files so the layers cannot be swapped
Use descriptive layer filenames and include a readme or fabrication/assembly drawing that identifies top and bottom. Review the orientation and origin, particularly for bottom-side stencil data. A mirrored display can appear familiar while being wrong for the intended manufacturing operation.
The PCB stencil page owns stencil selection and quotation. Use solder-mask opening design for permanent coating geometry. Keeping those routes distinct helps an engineer reach the right review without reading two nearly identical generic layer descriptions.
Questions that prevent avoidable rework
Ask whether the stencil supplier is expected to optimize apertures and, if so, how proposed changes will be approved. Identify the source revision and request an aperture review for critical packages. Clarify whether the assembly provider requires paste files, copper files, package data or an existing stencil specification for the quotation.
If a board already has a printing problem, provide the measured deposit or defect location instead of only a screenshot of the mask setting. Include stencil thickness, aperture shape and the package reference. That information makes the next conversation about a real printing task rather than an ambiguous request to change the mask.
Review one critical footprint through the complete file chain
Choose a representative footprint whose geometry makes the mask decision important. Place its component recommendation, copper land, mask opening and paste aperture side by side. Name the role of each boundary before comparing dimensions. This prevents an aperture change intended for printing from being applied to the permanent coating by mistake.
Next, identify the source of every allowance. Nominal expansion, local opening growth and mask-to-copper registration describe different effects. A conservative tolerance budget can be appropriate, but only when it does not count the same variation twice. If the source of an allowance is unknown, preserve that as an open question instead of treating a familiar round number as verified process data.
Inspect the final exported files for that footprint and at least one important exception. This is where object overrides, library differences and rule scope become visible. The released output should match the documented design choice. A manufacturing partner's proposed change should be tied to the same feature and revision so both sides can assess its effect on assembly.
For a repeat order, retain the approved file set and any accepted exception. If a new supplier or mask grade is proposed, review the critical geometry against that route rather than assuming the old nominal dimensions are universally producible. The objective is a stable functional interface, not the smallest possible number in a capability table.
The enquiry can be brief: the marked region, exact component, relevant layers and the decision you need to make. That gives the reviewer enough context to discuss a real margin or opening strategy without forcing the customer to complete an unrelated cost calculator first.
Standards, source context and limits
Use the official references for their stated scope and the applicable controlled document for contractual requirements. A public scope page, product description or application note is not a complete acceptance specification. Material-supplier guidance applies to the named material and process; it is not evidence that every option is available for this board.
Agree the document revision, construction, inspection method and any exceptions with the responsible engineering and quality teams. The explanatory drawings and worksheet examples on this page are original planning aids, not factory records, qualification results or compliance certificates.

