
RAYPCB · Assembly engineering guide
Step Stencil SMT Printing: Setup, SPI and Process Validation
Step stencil SMT printing is the process of producing controlled deposits through a foil with different local thicknesses. The tool's geometry is only one part of the result. Board support, print direction, squeegee behavior, separation, paste condition and cleaning must work with the thickness transitions. This guide focuses on setup and verification after a stepped construction has been proposed or approved.
Preliminary files are welcome. Identify your board revision, printing equipment and the question you need to resolve.
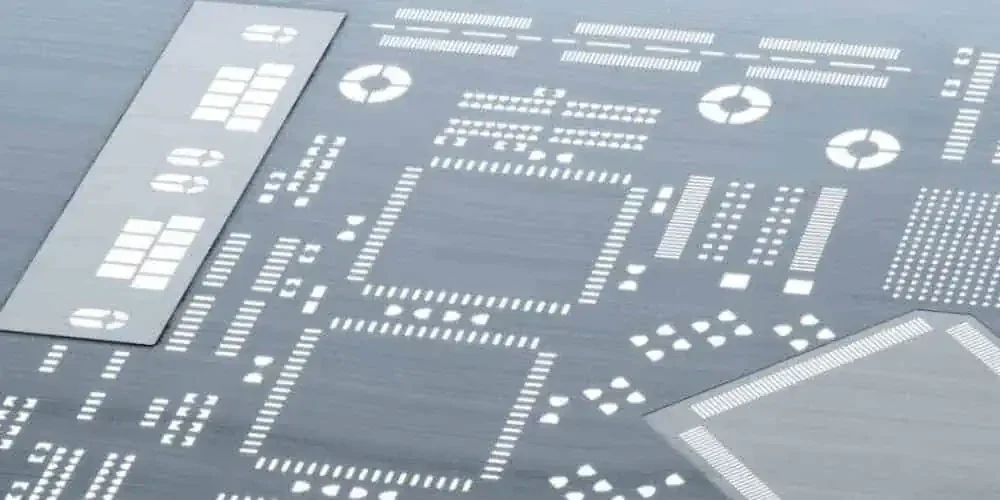
What to establish before the next decision
| Review item | Working requirement |
|---|---|
| Tool identity | Match the zone map, modified face and local thickness to the recipe. |
| Mechanical contact | Verify blade path and stable board support through the transition. |
| Measurement groups | Compare thin zones, thick zones and boundary apertures separately. |
| Controlled trial | Record material, print settings, inspection recipe and relevant restart behavior. |
| Release | Preserve accepted conditions and the agreed post-reflow evidence. |
Carry the zone map into the printer setup
The printing team needs a drawing that identifies each thickness zone, its apertures and the face on which the transition occurs. A label such as “100/150 microns” is insufficient without the zone locations and side definition. Compare the physical stencil identifier with the approved drawing before selecting a recipe.
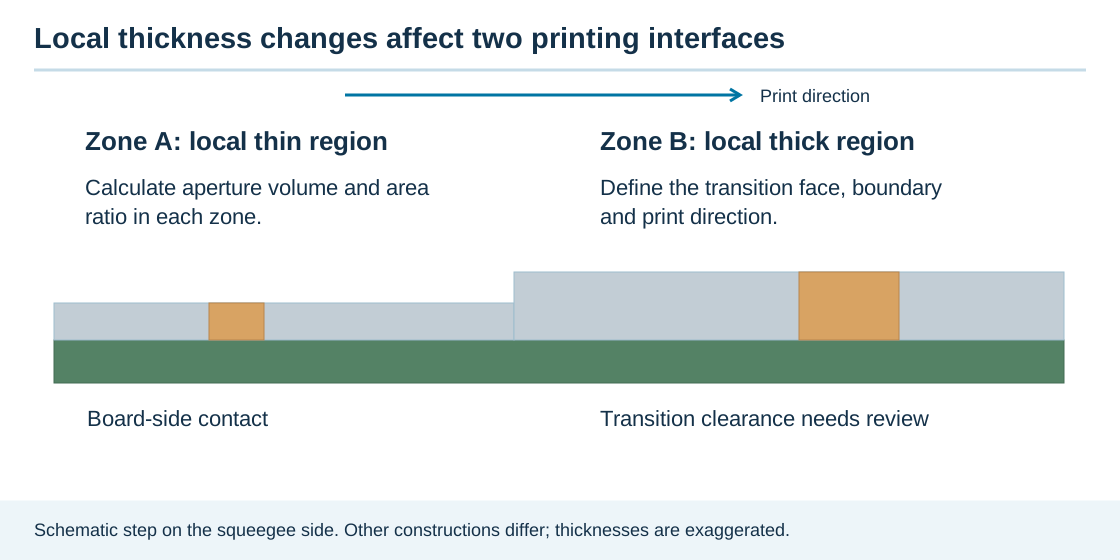
Keep the print direction on the setup record. The blade encounters a local transition in a particular orientation, and that relationship can matter when evaluating deposits close to the step. If the drawing or zone arrangement is still unresolved, use the stepped stencil product and design guide first. Process tuning should not become an undocumented way of compensating for an unclear construction.
Review contact at both the blade and board interfaces
The squeegee-side profile influences how the blade travels over the foil. The board-side profile influences local contact and sealing. Their effects depend on the actual step construction; do not treat every recessed region as mechanically equivalent. Check whether the blade path, stroke length and available clearance are consistent with the approved stencil.
At the board interface, verify support beneath the printing area and examine any local topography that could interfere with gasketing. For a second-side print, the support plan must account for fitted components. A visually flat stencil over an unloaded panel does not prove that the assembly remains stable during a printing stroke. Record the fixture configuration with the recipe.
Two-zone step stencil geometry comparison
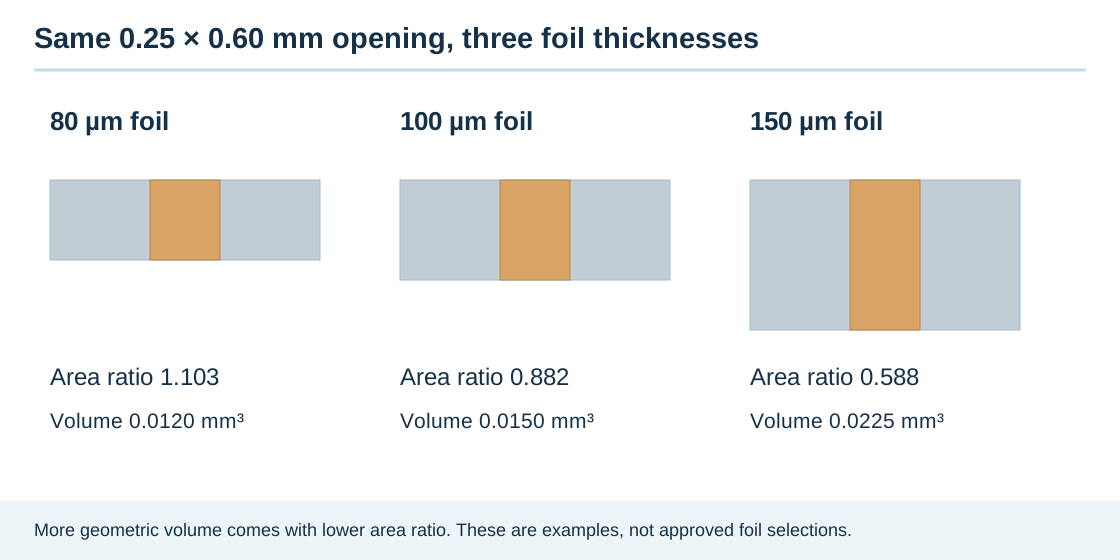
Enter the opening area and perimeter for one representative aperture in each zone, then the local foil thickness in micrometres. Area ratio is opening area divided by perimeter times thickness. Geometric volume is opening area times thickness. Perimeter matters: two openings of equal area can have different wall contact.
The example compares a 0.15 mm² opening with 1.70 mm perimeter at 100 µm against a 1.00 mm² opening with 4.00 mm perimeter at 150 µm. Their geometric volumes are 0.015 and 0.150 mm³ respectively. The tenfold difference reflects both aperture area and foil thickness; it is not a tenfold claim about transfer or joint strength.
The tool does not calculate transition keep-out, squeegee deformation or board contact. Its plausibility check rejects area/perimeter combinations that cannot describe a planar opening, but passing that check does not validate an actual shape. Confirm the zone drawing, modified face, orientation and nearby apertures with the printing team before release.
RAYPCB ENGINEERING
Stencil EngineeringStencil Design Workbench
Loading Stencil Design Workbench…
Use two-zone arithmetic to organize the trial
The workbench reports area ratio and geometric volume independently for two aperture groups. Enter actual opening area and perimeter, along with local thickness. This allows the engineer to distinguish a high-volume goal from a difficult-release geometry. It does not simulate paste flow across the transition or predict the pressure needed to print a zone.
For example, increasing local thickness from 100 to 150 µm adds 50% geometric volume to an unchanged opening, while reducing its area ratio by one third. Whether the resulting deposit is useful depends on transfer and assembly requirements. Define the intended improvement before testing; otherwise a larger SPI volume can be mistaken for success even where the target deposit has been exceeded.
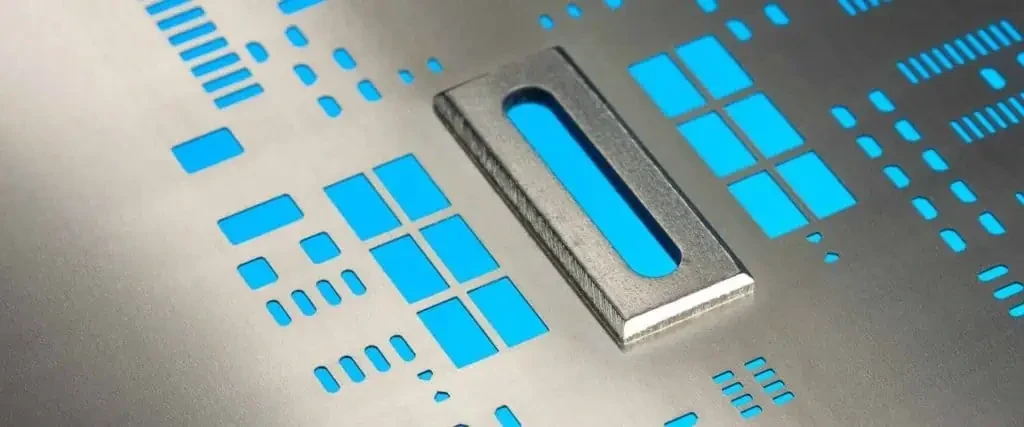
Establish a controlled first-print sequence
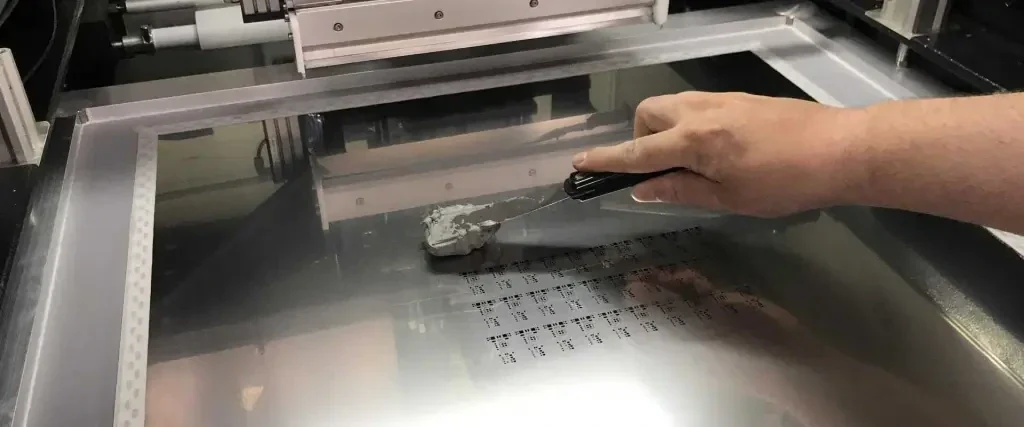
Confirm stencil identity, board revision, paste identity and equipment setup before printing. Check registration without using excess force to compensate for a mismatch. Evaluate the first deposit and pay particular attention to apertures near the zone boundaries, fine features inside thin zones and larger deposits in thick zones.
Use a documented response when a print is unsuitable. The decision to clean, adjust, reprint or remove a board from the process must follow the production procedure and material compatibility. Do not simply add paste to a suspect print without knowing whether that creates an uncontrolled deposit. The cleaning and misprint control guide explains why underside wiping and cleaning a misprinted board are separate operations.
Follow the working sequence
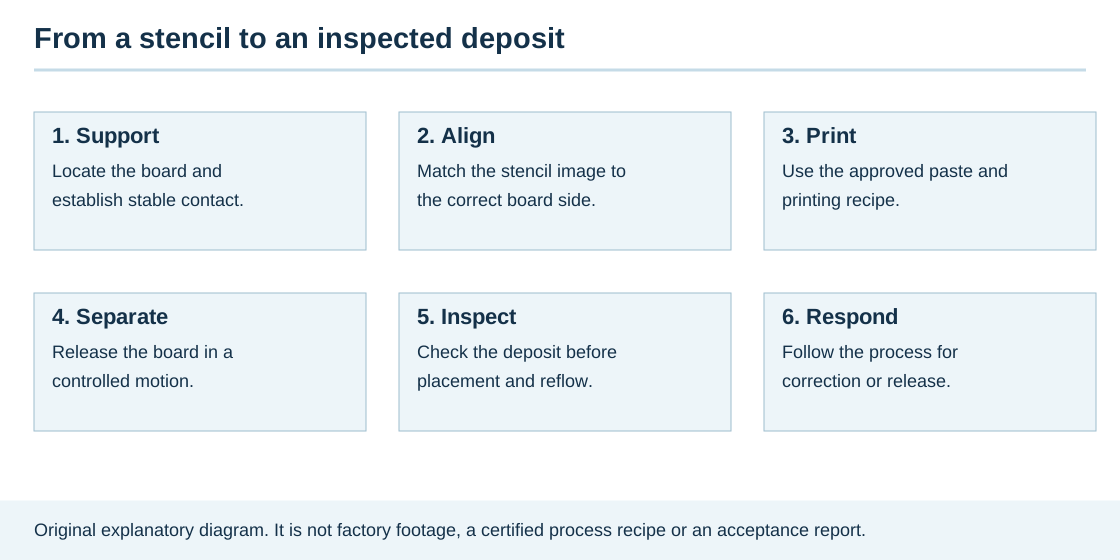
The steps remain readable without animation. Use the optional player to follow one operation at a time; it starts paused and respects reduced-motion preferences. This is a conceptual explanation, not a production video.
- Support
Locate and stabilize the board or panel.
- Align
Match the approved stencil to the correct side.
- Print
Use the defined material and controlled recipe.
- Separate
Release the board without disturbing the deposit.
- Inspect
Check the printed material before placement.
- Continue
Release or correct according to the assembly process.
Compare SPI by zone and aperture family
Collect measurements using a recipe appropriate to the intended deposits. Analyze thin and thick regions separately, and distinguish border apertures from those well inside a zone. A whole-board mean can hide a localized release problem. Record position and shape observations alongside volume, because the correct amount of paste in the wrong place is still a problem.
Compare repeat prints, not only the best first board. Include relevant conditions such as a pause and restart when they are part of the expected workflow. Use the same measurement basis when comparing configurations. A change in the inspection recipe can alter reported values without a corresponding physical improvement, so recipe revisions belong in the experiment record.
Troubleshoot the observed pattern
Low deposits near a transition can suggest a contact or release issue, but the location alone does not identify the cause. Inspect aperture condition, support, alignment and paste state before changing the foil. Smearing near a region can involve underside contamination or inadequate sealing as well as the step itself. Review one controlled variable at a time where practical.
If a large zone prints adequately while small apertures remain inconsistent, focus on the feature-specific process window rather than increasing all paste volumes. If every region shifts similarly, examine registration or board movement. These comparisons help avoid unnecessary tooling revisions. The aperture and deposit guide provides the geometry vocabulary needed to describe the issue precisely to a stencil or assembly engineer.
Cleaning and changeover need zone awareness
Local thickness features and coatings must be compatible with the cleaning approach. Confirm the equipment and chemistry instructions for the actual foil rather than assuming a previous flat-stencil routine applies unchanged. Cleaning should remove residue without introducing deformation, damage or remaining liquid that affects the next print.
At changeover, verify both the stencil and its stored recipe. Two tools for the same board family can have different zone maps, foil thicknesses or mounting details. Use an identifier that distinguishes them. Store the approved setup and inspection criteria with the stencil revision, and segregate superseded tools so an old construction cannot be returned accidentally to the production line.
Qualify the assembly result, then preserve the evidence
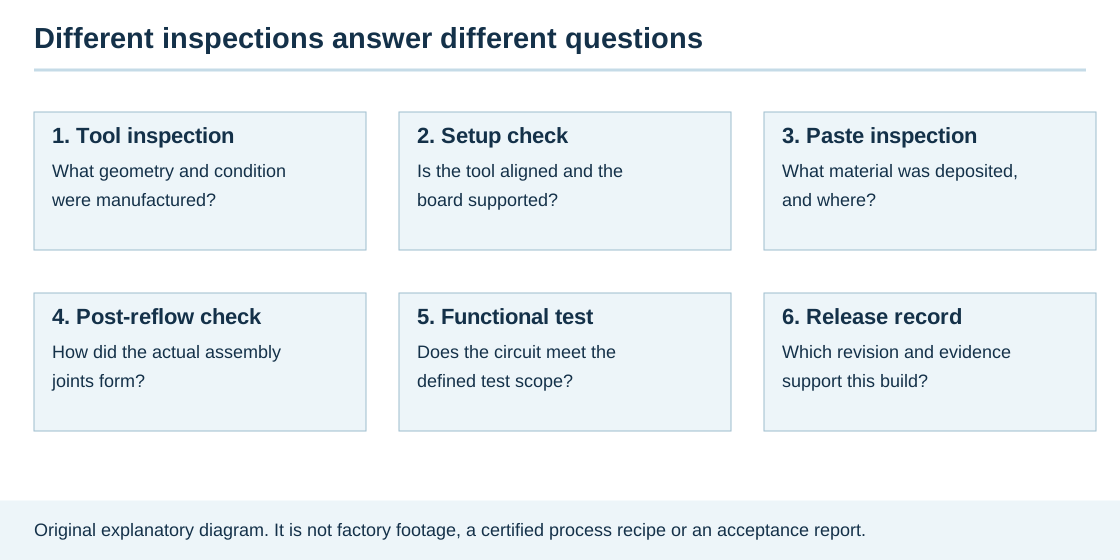
An acceptable paste print is necessary evidence for process control, but it does not establish the finished joint. Evaluate placement, reflow and the agreed inspection requirements for the actual component groups. For hidden joints, define the relevant inspection scope rather than inferring quality from a clean-looking top surface.
Retain the trial conditions, measurements, accepted recipe and any limitations. If the stencil or board changes later, use those records to decide which parts of the process need review. For a manufacturing enquiry, send the zone drawing and the observed issue with the files. PCB Assembly services is the correct next route when the request covers the complete build rather than only fabrication of a replacement foil.
Keep the cost discussion tied to the actual task
If this review changes the stencil construction, ask for a quotation against the resulting artwork and equipment interface. Separate the physical tool from engineering work, any special inspection and freight. A change in aperture design can affect the scope even when the outside board dimensions remain identical.
For an allowance-based calculation, use the PCB Stencil hub and cost planner. That tool deliberately uses your entered rates rather than presenting unverified tariffs as current prices. A process improvement should also be assessed against evidence from the actual assembly; this page does not assign a monetary saving to a hypothetical yield increase. If the immediate requirement is engineering help or a complete build, proceed directly to an enquiry.
Send a brief an engineer can act on
Include the paste artwork, board or panel outline, side and revision; describe the printer, holder or manual fixture. Identify critical components and the exact decision that remains open. For an existing process problem, add the observed location, relevant conditions and available inspection evidence. Keep files and photographs tied to the same revision.
State whether you need stencil fabrication only or a populated-board project. PCB Assembly services can address the broader scope of procurement, placement, soldering and agreed inspection or test. The assembly process guide explains how the printing step connects to the rest of the build.
Download the current tool brief or open an email draft when you want to share the calculation. Attach design files separately. The Contact link opens the existing enquiry page; it does not silently transmit calculator values or claim an integrated Gerber upload. You can enquire before completing a tool when your question is about the manufacturing route rather than a numeric result.
Questions about this stencil task
Which SPI result should be compared first?
Start with the defined deposit requirements for each aperture family and zone. Compare position, shape and the configured quantitative measurements. A whole-board average can conceal a boundary or small-feature problem, so keep those groups visible in the analysis.
Can I reuse the flat-stencil recipe?
Treat it as prior information, not automatic approval. The local profile can affect contact and cleaning behavior. Review support, blade travel, separation and inspection, then retain the conditions demonstrated for the stepped construction.
Does this calculator approve a stencil for production?
No. It makes its stated geometry or arithmetic visible. It does not inspect your files, predict paste release or certify compliance with an IPC standard. Use the result alongside the actual drawing, component guidance, qualified process and agreed inspection evidence.
What information helps if I am unsure about the next step?
Send the current design revision and describe the unresolved task: mounting fit, deposit geometry, process behavior or quotation scope. Include the relevant equipment and component details. Preliminary information is acceptable when its status is clear; approval of a production tool requires the agreed final data.
Continue with the next useful decision
Original engineering and standards references
Use component and process documents in their stated application context. Public IPC contents establish scope, not every licensed clause. Specify the agreed standard revision and acceptance requirements on the order; this guide does not claim universal IPC certification for a geometry calculation.

