
RAYPCB · ENGINEERING REFERENCE
IPC-A-610: Classes, Acceptance & Inspection Evidence
Define the IPC-A-610 revision, class and assembly evidence. Prepare an acceptance brief and distinguish workmanship from process and functional verification.
Original engineering guidance · References checked September 27, 2026
What does IPC-A-610 actually tell you?
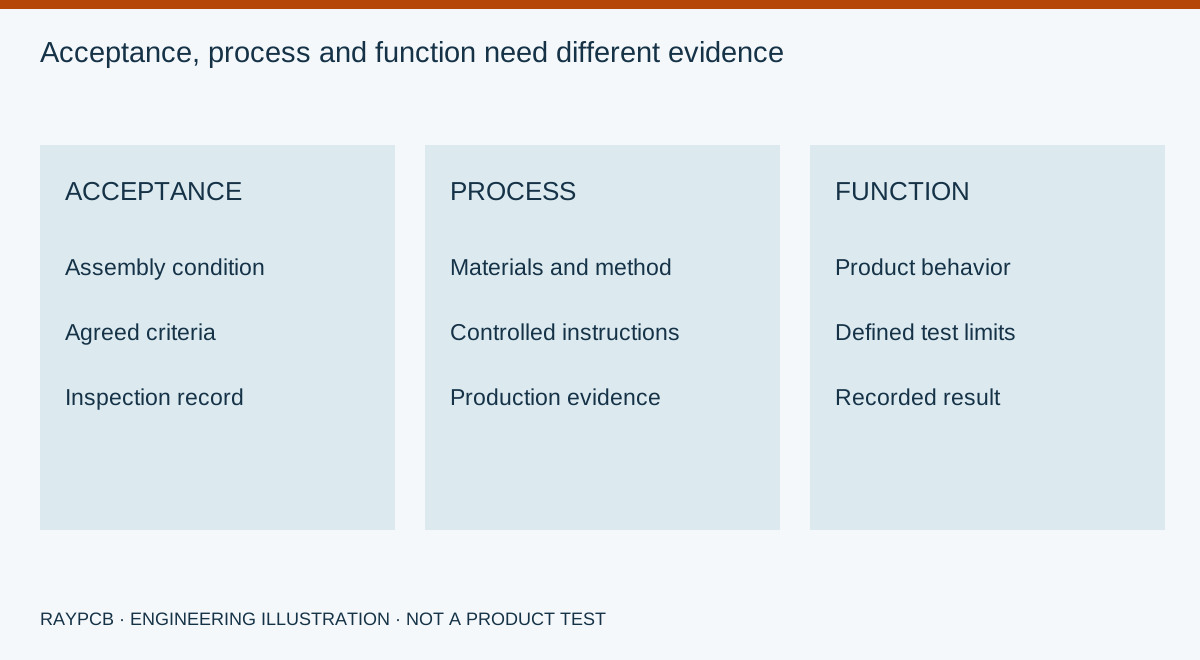
IPC-A-610 addresses the acceptability of completed electronic assemblies. It helps the responsible parties evaluate workmanship against an agreed edition, product class and applicable requirements. It does not design the circuit, define every manufacturing process, or prove that the finished product will work in its intended environment. A useful purchase order therefore connects the acceptance document to the assembly drawing, inspection plan and functional test requirements.
For a buyer, the important question is not simply whether a supplier mentions IPC-A-610. Ask which revision applies, who agreed the class, what evidence will be recorded, and how exceptions will be resolved. Those answers turn a general quality statement into a reviewable manufacturing requirement. The worksheet below helps organize that discussion without reproducing the licensed standard or making an automated pass/fail decision.
The wider IPC standards for PCB assembly guide explains how acceptance, soldering-process and bare-board documents work together. This page concentrates on the completed assembly and the evidence needed to accept it.
Separate acceptance, process control and product performance
IPC's official announcement of the J revisions distinguishes IPC-A-610J acceptance criteria from the soldering materials and process requirements in J-STD-001J. Both were released in 2024. The applicable contractual edition should be stated explicitly; an older drawing is not automatically updated by the publication of a newer document. Check the IPC document revision table when preparing a new specification.
| Question | Useful evidence | What remains separate |
|---|---|---|
| Is the assembled workmanship acceptable? | Agreed acceptance document, revision, class and inspection record | Circuit functionality and field reliability |
| Was the soldering process controlled? | Applicable process requirements, work instructions and production records | Acceptance of each individual assembly |
| Does the circuit perform its intended task? | Approved functional test procedure, limits and result | Product qualification and environmental lifetime |
| Are the supplied bare boards acceptable? | Fabrication specification and bare-board acceptance evidence | Component assembly workmanship |
An incoming board report cannot replace the completed PCBA inspection record. Likewise, a successful boot test cannot establish the quality of every hidden joint. Treat these as complementary evidence paths and define them before quotation. This helps the supplier estimate inspection, programming and test effort accurately instead of discovering additional requirements after the assembly is built.
Class 1, Class 2 and Class 3 are requirements decisions
The three product classes describe different performance expectations. Broadly, Class 1 concerns general electronic products; Class 2 concerns products where continued performance and extended service are important; Class 3 concerns products where sustained performance or performance on demand is critical. These descriptions orient the discussion. They are not a substitute for the definitions and detailed criteria in the authorized edition.
The responsible customer and manufacturer should agree the class and any additional requirements. An application label such as “industrial,” “medical” or “automotive” does not, by itself, complete that agreement. A demanding product may also have customer-specific, regulatory or environmental requirements that are not captured by writing a higher class number on the drawing.
Avoid choosing a class solely as a marketing statement. Ask what failure conditions matter, which assemblies and features are within scope, and what evidence the receiving team actually needs. If a customer exception changes a particular acceptance requirement, identify the feature, drawing reference and approval authority. A general note saying “all exceptions accepted” is difficult to audit and difficult to apply consistently.
For mixed product programs, keep the acceptance basis attached to the individual assembly revision. Two products built on the same line may use different requirements. Reusing a previous inspection checklist without checking the new drawing can silently carry the wrong criteria into a new order.
Build an acceptance scope you can review
Use this worksheet to record the document edition, declared class and open inspection questions. It deliberately does not choose a class from your industry or infer acceptance from a photograph. “Evidence identified” means you have a reference to review; it does not mean the evidence has passed an independent technical assessment.
RAYPCB ENGINEERING
Assembly EngineeringIPC-A-610 Acceptance Scope
Loading IPC-A-610 Acceptance Scope…
An incomplete brief is still useful. For example, you can request a quotation with the class unresolved, provided that the uncertainty is visible and the supplier identifies its pricing assumptions. Before production release, close the disagreement rather than allowing a default choice to become an accidental contract requirement. You can contact RAYPCB directly without completing the worksheet.
Match the inspection method to the feature
A practical inspection plan identifies the assembly state, the feature being evaluated and the method that can reveal it. Visible component orientation, some solder conditions and mechanical installation details may be checked optically. Hidden connections require a different evidence path. Do not represent one inspection machine as a universal replacement for all other verification.
For visible workmanship, AOI for PCB and SMT can support repeatable inspection when the program, reference conditions and review process are appropriate. For hidden joint structures, PCB X-ray inspection addresses a different question. Neither page should be read as a promise that every assembly receives every inspection method.
Inspection planning also needs a response to ambiguity. A feature that cannot be seen clearly should not be recorded as acceptable simply because no defect was detected. Define when magnification, alternate views, specialist review or another method is needed. Preserve the original observation before a repair changes the evidence.
Record which criteria apply to the exact package and condition. For example, a through-hole connection, a leaded surface-mount joint and a bottom-terminated component do not share one universal visual rule. This page intentionally avoids a simplified table of copied numerical thresholds; those belong in the applicable licensed standard and controlled inspection instructions.
Make an acceptance record traceable to the actual build
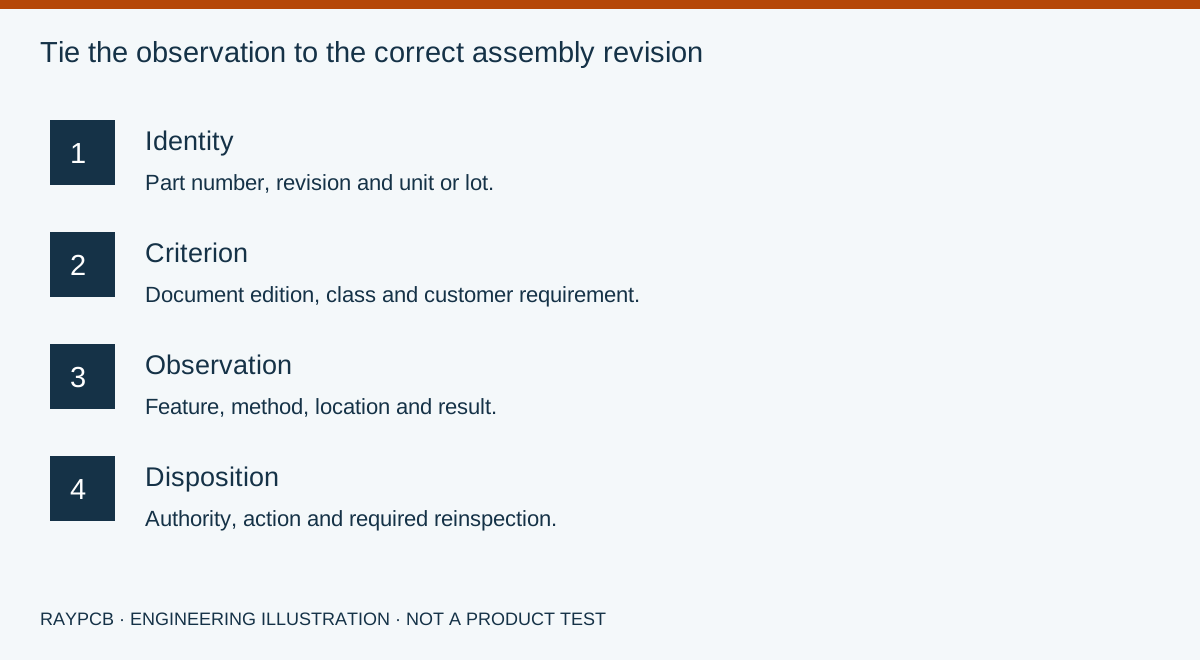
A useful acceptance record can be followed from the finished assembly back to its release inputs. Start with the part number, board revision, assembly revision and relevant lot or serial identity. Add the acceptance document, class and customer-specific requirements. Identify the inspection operation and the result, together with any approved deviation or rework history.
Photos are useful when they show the relevant feature, scale or orientation clearly. A general photo of a populated board is not evidence that a particular solder joint meets its criterion. If an image supports a disposition, retain enough context to locate that feature on the correct revision. Store the judgment and its basis alongside the image instead of relying on an unexplained green tick.
The record should also distinguish inspected items from uninspected items. Sampling, where used, needs an agreed plan and lot definition. “Inspected” and “100% inspected” are different statements; neither should be added to a quotation or certificate without an actual scope behind it. Do not infer a sampling plan from the class number.
For first builds, align this record with the first-piece inspection procedure. The first-piece review should capture issues that require changes to the release data or work instructions before the rest of the build proceeds. It should not become a photo album disconnected from the production revision.
Example: a connector joint that needs a disposition
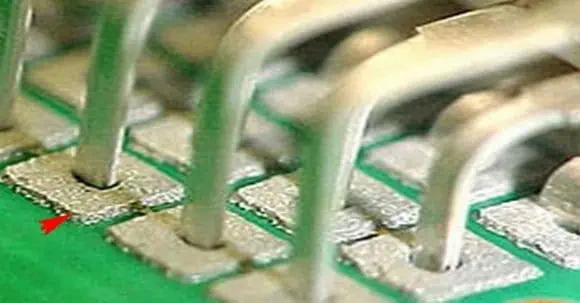
Consider an illustrative assembly with a through-hole connector and an agreed acceptance edition. An inspector flags one connection because the available view does not establish the required condition. The useful next step is to identify the exact location and applicable criterion, obtain adequate evidence, and classify the observation using the controlled procedure. Guessing from the connector's appearance is not a reliable decision.
If rework is authorized, the record should identify the affected assembly, the approved method and the verification performed afterward. If a deviation is considered instead, document the responsible authority and its scope. A deviation for one feature or lot should not silently become a new acceptance rule for future orders.
This example is a workflow, not a representation of an actual customer defect or a numerical IPC judgment. The same discipline applies when an issue concerns component placement, mounting hardware, cleanliness or protective coating. The feature changes; the need for a clear criterion, evidence and disposition remains.
Control revisions without promising “the latest” indefinitely
The public IPC-A-610J contents identify the March 2024 edition and its scope. This is a useful authorized reference, not a free copy of the complete standard. Obtain the licensed document through IPC or an authorized source when you need the detailed acceptance criteria.
A good revision-change review compares the requirements used by the current assembly against the proposed new basis. Identify affected inspection instructions, training needs, customer approvals and open work orders. Changing the text in a website footer does not update those controlled records.
When the purchase order and drawing disagree, resolve the conflict through the agreed order of precedence and responsible parties. Do not assume that the newest date always wins. Record the resolution so that production, inspection and receiving teams use the same requirement.
Personnel training, an organization-level quality system and product acceptance should also remain distinct. A trained inspector does not automatically certify every shipped board. A factory certificate does not replace the evidence required for the specific assembly. Ask for the relevant record rather than accepting an undefined “IPC certified PCB” claim.
What to include in an assembly enquiry
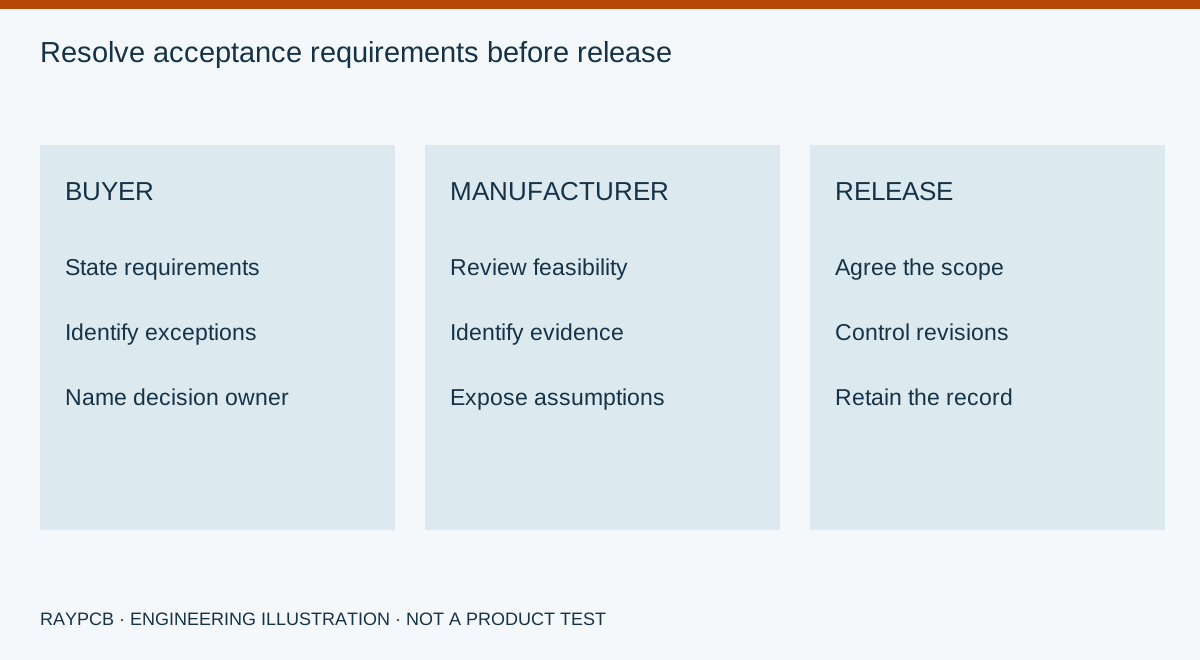
Send the assembly number and revision, quantities, release files and the proposed acceptance basis. Identify any addenda, customer clauses, special inspection locations, hidden joints, coating requirements and report expectations. Include the expected handling of defects, repair approvals and deviations where these affect the manufacturing scope.
If you have not yet selected the acceptance class, describe the product's operational requirements and the decision owner. The engineering discussion can then expose the missing choices. Do not supply confidential end-use detail unless it is necessary for the review; a clear technical requirement is more useful than a broad application slogan.
The PCB assembly service is the commercial route for a complete build. The required PCBA files guide helps organize the information that keeps quoting and production consistent. For this page's specific task, attach the acceptance brief to your enquiry and ask which assumptions remain open.
IPC-A-610 questions before placing an order
Is IPC-A-610 the same as J-STD-001?
No. They address related but different roles. IPC-A-610 addresses completed assembly acceptability; J-STD-001 addresses soldering materials and process requirements. Define the applicable editions and their contractual relationship instead of treating one title as a substitute for the other.
Does Class 3 guarantee that a product will never fail?
No. An acceptance class cannot eliminate design errors, misuse, environmental stress or every latent defect. Product reliability depends on the design, materials, manufacturing controls and relevant verification. State the performance and environmental requirements separately.
Can I use this page as a free IPC-A-610 PDF?
This page is original engineering guidance. It links to authorized IPC information and a public table of contents, but does not distribute the licensed standard. Use the authorized document for detailed acceptance decisions.
Can a photograph establish compliance?
A photograph may support a specific inspection record if it shows the required evidence clearly. It does not establish the condition of features outside the view, the entire assembly, or the manufacturing process. The applicable criterion and traceable assembly identity remain necessary.
What happens when the acceptance requirement is not agreed?
Keep the item open and identify who must decide. A quotation may state an explicit assumption, but production release should resolve the actual requirement. The worksheet records uncertainty rather than converting an incomplete answer into a pass.
Prepare a scoped assembly review
Send the board revision, construction, quantity and the inspection, protection, programming or test question you need reviewed. Identify unresolved requirements so the response can address them.
Send requirements for reviewOptional: attach the downloaded worksheet manually. This guidance does not certify a design, approve a shipment or replace the applicable authorized standards.

